NE NEH NEI Series · R004
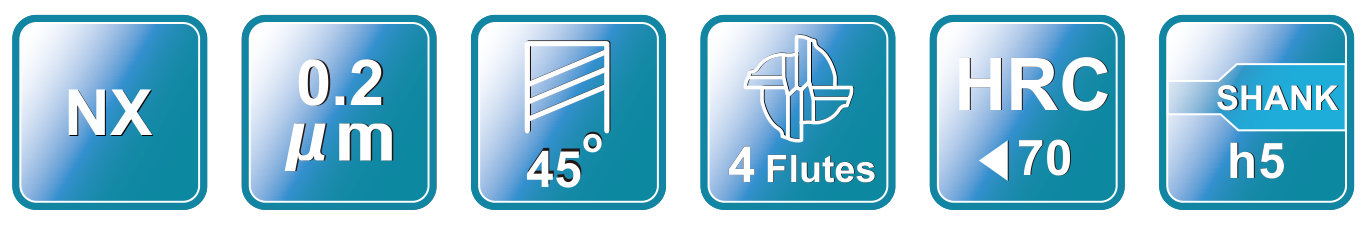
Catalog group R004.
Use the symbols and values with the corresponding model table.

Build your square end mill range around the cutting diameters, flute counts and tool lengths your customers need. AXIMET's catalog groups 2-, 4- and 6-flute models by series, so you can request the right combination by model rather than diameter alone.
A square end mill, also called a flat end mill, has cutting edges arranged around a nominally flat end. It is used to produce features such as slots, pockets, shoulders and flat surfaces. The required feature comes first: a cutter must fit the slot or pocket and reach the bottom while leaving enough clearance for the holder.
Two cutters with the same nominal diameter can have different flute counts, cutting lengths, shank diameters and overall lengths. For a mixed order, compare the complete model row against the holder and feature drawing, then specify quantities for each item.
The catalogue includes the following square-end series. Select a series and review its own dimension drawing and model table before ordering.
| Catalogue series | Flutes in the listed group | Catalog group |
|---|---|---|
| NE / NEH / NEI | 4 | High-hardness and high-precision series N |
| NE | 6 | High-hardness and high-precision series N |
| HE | 2 or 4 | High-speed and high-hardness series H |
| DE | 2, 4 or 6 | Universal series D |
| DEX | 4 | Universal series D; see DEX model rows |
| EE | 4 | Copper electrode series E |
Not every flute count is available in every series or size. Compare the corresponding model row and dimension drawing before assembling a size range. Where a catalog field is blank, request the missing information rather than assuming a value.
Cutting diameter establishes the nominal cutter size. For slotting, check the required slot width and finish allowance; for a pocket, check that the cutter can enter the internal corners and follow the intended toolpath.
Flute length identifies the fluted cutting section. Compare it with the axial engagement required by the operation and make sure the neck, holder and remaining tool length clear the feature. Flute length and overall tool length are different dimensions.
Overall length and reach affect access to the feature. Check the required stick-out against the holder and part geometry. A longer overall tool is not automatically suitable for every deep pocket.
Shank diameter must match the toolholder and clamping arrangement. Confirm the specified diameter and holder requirements before placing a mixed-size order.
Flute count affects the number of cutting edges and the space available for chips. A slotting job that encloses the cutter places different demands on chip clearance than an open-side pass. Consider the work material, operation, toolpath and machine together; do not select a flute count by material name alone.
Start with the width, depth and corner geometry of the feature. Consider chip evacuation and tool access as well as cutter diameter. A narrow, deep slot can place different demands on a cutter than an open pocket; review engagement and machine setup before selecting the series.
Define the required wall and floor geometry, cutting depth and access around the workpiece. Compare the cutting length with the wall height and make sure the holder has room to clear clamps and adjacent features.
The EE group is listed in the catalogue's copper-electrode series. When ordering for electrode work, provide the workpiece, the geometry to be produced and the required model dimensions so the intended application can be checked against the catalogue entry.
| Tool geometry | Typical selection question |
|---|---|
| Square end | Does the feature call for a flat floor or a straight shoulder? |
| Ball nose | Is a rounded tool profile needed for a contoured surface? |
| Corner radius | Does the part or toolpath require a defined radius at the cutter corner? |
These profiles produce different shapes. A flat cutter also leaves an internal floor-to-wall corner determined by its edge geometry; do not assume it creates a perfectly sharp internal corner. Include the feature tolerance and drawing requirements with your inquiry.
For each model, identify the dimensions and characteristics that matter to the receiving inspection: cutter diameter, shank diameter, flute count, flute length and overall length. If the feature requires a particular corner condition or drawing revision, include it in the purchase specification.
For a trial order, keep the quoted model and drawing revision with the sample. Evaluate the tool in the intended machine, holder and workpiece, and record the agreed dimensions and acceptance requirements before a repeat order.
Send us your catalogue model numbers and quantities, or provide the cutting diameter, flute count, cutting length, overall length and shank diameter required for each line. Include the workpiece material, operation, machine and holder, together with any drawing or sample requirements. If packaging, labels or marking matter to your order, tell us the details so they can be reviewed with the quotation.
Compare each square-end series using its product view, dimension drawing and catalog symbols.
Catalog group R004.
Use the symbols and values with the corresponding model table.
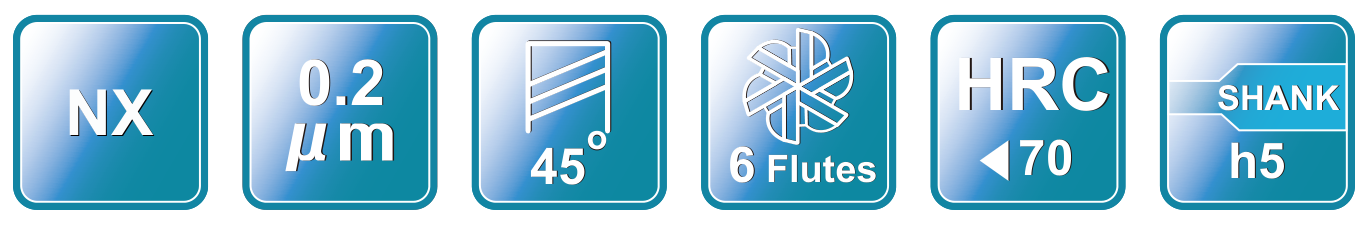
Catalog group R005.
Use the symbols and values with the corresponding model table.
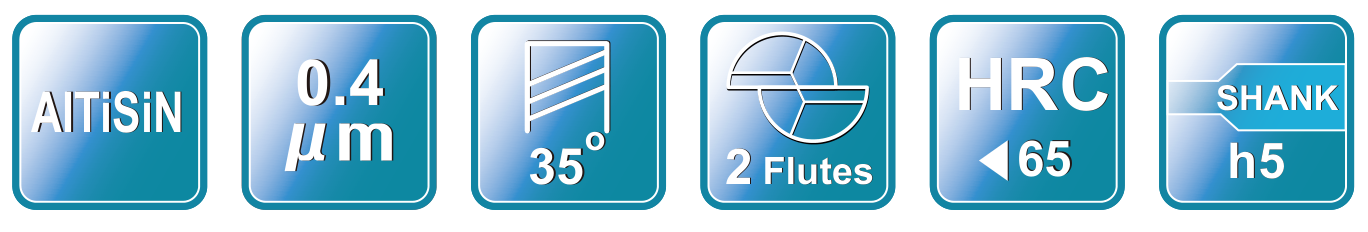
Catalog group R018.
Use the symbols and values with the corresponding model table.
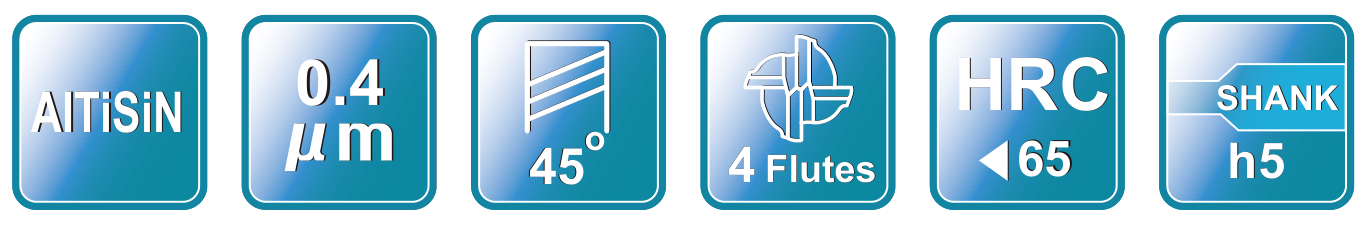
Catalog group R020.
Use the symbols and values with the corresponding model table.
Catalog group R036.
Use the symbols and values with the corresponding model table.
Catalog group R038.
Use the symbols and values with the corresponding model table.
Catalog group R039.
Use the symbols and values with the corresponding model table.
Catalog group R042.
Use the symbols and values with the corresponding model table.
Catalog group R059.
Use the symbols and values with the corresponding model table.
Review the listed model dimensions and request any additional specifications needed for your order. Blank fields and catalog dashes remain unavailable values; they are not converted to zero.
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Effective length (L1, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|---|
| NE0104A | D1 | 3 | — | L50 | 4 | 4 |
| NE0104 | D1 | 3 | — | L60 | 6 | 4 |
| NE0154A | D1.5 | 4 | — | L50 | 4 | 4 |
| NE0154 | D1.5 | 4 | — | L60 | 6 | 4 |
| NE0204A | D2 | 6 | — | L50 | 4 | 4 |
| NE0204 | D2 | 6 | — | L60 | 6 | 4 |
| NE0254A | D2.5 | 6 | — | L50 | 4 | 4 |
| NE0254 | D2.5 | 6 | — | L60 | 6 | 4 |
| NE0304A | D3 | 8 | — | L50 | 4 | 4 |
| NE0304 | D3 | 8 | — | L60 | 6 | 4 |
| NE0404A | D4 | 10 | 12 | L50 | 4 | 4 |
| NE0404 | D4 | 10 | 12 | L60 | 6 | 4 |
| NE0504 | D5 | 13 | 15 | L60 | 6 | 4 |
| NE0604 | D6 | 13 | 16 | L50 | 6 | 4 |
| NE0604L | D6 | 13 | 16 | L60 | 6 | 4 |
| NE0804 | D8 | 19 | 23 | L60 | 8 | 4 |
| NE1004 | D10 | 22 | 27 | L75 | 10 | 4 |
| NE1204 | D12 | 26 | 32 | L75 | 12 | 4 |
| NEH0404A | D4 | 12 | 14 | L75 | 4 | 4 |
| NEH0404 | D4 | 12 | 14 | L75 | 6 | 4 |
| NEH0604 | D6 | 20 | 23 | L75 | 6 | 4 |
| NEH0804 | D8 | 25 | 29 | L75 | 8 | 4 |
| NEI0604 | D6 | 20 | 23 | L100 | 6 | 4 |
| NEI0804 | D8 | 25 | 29 | L100 | 8 | 4 |
| NEI1004 | D10 | 33 | 38 | L100 | 10 | 4 |
| NEI1204 | D12 | 37 | 43 | L100 | 12 | 4 |
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Effective length (L1, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|---|
| NE0606 | D6 | 15 | — | L50 | 6 | 6 |
| NE0606L | D6 | 15 | — | L60 | 6 | 6 |
| NE0806 | D8 | 20 | — | L60 | 8 | 6 |
| NE1006 | D10 | 25 | — | L75 | 10 | 6 |
| NE1206 | D12 | 30 | — | L75 | 12 | 6 |
| NE1406 | D14 | 35 | — | L100 | 14 | 6 |
| NE1606 | D16 | 40 | — | L100 | 16 | 6 |
| NE2006 | D20 | 45 | — | L100 | 20 | 6 |
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|
| HE0102A | D1 | 3 | L50 | 4 | 2 |
| HE0102 | D1 | 3 | L60 | 6 | 2 |
| HE0152A | D1.5 | 4 | L50 | 4 | 2 |
| HE0152 | D1.5 | 4 | L60 | 6 | 2 |
| HE0202A | D2 | 6 | L50 | 4 | 2 |
| HE0202 | D2 | 6 | L60 | 6 | 2 |
| HE0252A | D2.5 | 6 | L50 | 4 | 2 |
| HE0252 | D2.5 | 6 | L60 | 6 | 2 |
| HE0302Z | D3 | 8 | L50 | 3 | 2 |
| HE0302A | D3 | 8 | L50 | 4 | 2 |
| HE0302 | D3 | 8 | L60 | 6 | 2 |
| HE0352A | D3.5 | 10 | L50 | 4 | 2 |
| HE0352 | D3.5 | 10 | L60 | 6 | 2 |
| HE0402A | D4 | 10 | L50 | 4 | 2 |
| HE0402 | D4 | 10 | L60 | 6 | 2 |
| HE0502Z | D5 | 13 | L60 | 5 | 2 |
| HE0502 | D5 | 13 | L60 | 6 | 2 |
| HE0602 | D6 | 15 | L50 | 6 | 2 |
| HE0602L | D6 | 15 | L60 | 6 | 2 |
| HE0802 | D8 | 20 | L60 | 8 | 2 |
| HE1002 | D10 | 25 | L75 | 10 | 2 |
| HE1202 | D12 | 30 | L75 | 12 | 2 |
| HE1602 | D16 | 45 | L100 | 16 | 2 |
| HE2002 | D20 | 45 | L100 | 20 | 2 |
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|
| HE0104A | D1 | 3 | L50 | 4 | 4 |
| HE0104 | D1 | 3 | L60 | 6 | 4 |
| HE0154A | D1.5 | 4 | L50 | 4 | 4 |
| HE0154 | D1.5 | 4 | L60 | 6 | 4 |
| HE0204A | D2 | 6 | L50 | 4 | 4 |
| HE0204 | D2 | 6 | L60 | 6 | 4 |
| HE0254A | D2.5 | 6 | L50 | 4 | 4 |
| HE0254 | D2.5 | 6 | L60 | 6 | 4 |
| HE0304Z | D3 | 8 | L50 | 3 | 4 |
| HE0304A | D3 | 8 | L50 | 4 | 4 |
| HE0304 | D3 | 8 | L60 | 6 | 4 |
| HE0354A | D3.5 | 10 | L50 | 4 | 4 |
| HE0354 | D3.5 | 10 | L60 | 6 | 4 |
| HE0404A | D4 | 10 | L50 | 4 | 4 |
| HE0404 | D4 | 10 | L60 | 6 | 4 |
| HE0504Z | D5 | 13 | L60 | 5 | 4 |
| HE0504 | D5 | 13 | L60 | 6 | 4 |
| HE0604 | D6 | 15 | L50 | 6 | 4 |
| HE0604L | D6 | 15 | L60 | 6 | 4 |
| HE0804 | D8 | 20 | L60 | 8 | 4 |
| HE1004 | D10 | 25 | L75 | 10 | 4 |
| HE1204 | D12 | 30 | L75 | 12 | 4 |
| HE1604 | D16 | 45 | L100 | 16 | 4 |
| HE2004 | D20 | 45 | L100 | 20 | 4 |
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|
| DE0102A | D1 | 3 | L50 | 4 | 2 |
| DE0102 | D1 | 3 | L50 | 6 | 2 |
| DE0152A | D1.5 | 4 | L50 | 4 | 2 |
| DE0152 | D1.5 | 4 | L50 | 6 | 2 |
| DE0202A | D2 | 6 | L50 | 4 | 2 |
| DE0202 | D2 | 6 | L50 | 6 | 2 |
| DE0252A | D2.5 | 6 | L50 | 4 | 2 |
| DE0252 | D2.5 | 6 | L50 | 6 | 2 |
| DE0302Z | D3 | 8 | L50 | 3 | 2 |
| DE0302A | D3 | 8 | L50 | 4 | 2 |
| DE0302 | D3 | 8 | L50 | 6 | 2 |
| DE0352A | D3.5 | 10 | L50 | 4 | 2 |
| DE0352 | D3.5 | 10 | L50 | 6 | 2 |
| DE0402A | D4 | 10 | L50 | 4 | 2 |
| DE0402 | D4 | 10 | L50 | 6 | 2 |
| DE0452 | D4.5 | 11 | L50 | 6 | 2 |
| DE0502Z | D5 | 13 | L50 | 5 | 2 |
| DE0502 | D5 | 13 | L50 | 6 | 2 |
| DE0552 | D5.5 | 15 | L50 | 6 | 2 |
| DE0602 | D6 | 15 | L50 | 6 | 2 |
| DE0702 | D7 | 18 | L60 | 8 | 2 |
| DE0802 | D8 | 20 | L60 | 8 | 2 |
| DE0902 | D9 | 23 | L75 | 10 | 2 |
| DE1002 | D10 | 25 | L75 | 10 | 2 |
| DE1102 | D11 | 30 | L75 | 12 | 2 |
| DE1202 | D12 | 30 | L75 | 12 | 2 |
| DE1402 | D14 | 35 | L100 | 14 | 2 |
| DE1602 | D16 | 45 | L100 | 16 | 2 |
| DE1802 | D18 | 45 | L100 | 18 | 2 |
| DE2002 | D20 | 50 | L100 | 20 | 2 |
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|
| DE0104A | D1 | 3 | L50 | 4 | 4 |
| DE0104 | D1 | 3 | L50 | 6 | 4 |
| DE0154A | D1.5 | 4 | L50 | 4 | 4 |
| DE0154 | D1.5 | 4 | L50 | 6 | 4 |
| DE0204A | D2 | 6 | L50 | 4 | 4 |
| DE0204 | D2 | 6 | L50 | 6 | 4 |
| DE0254A | D2.5 | 6 | L50 | 4 | 4 |
| DE0254 | D2.5 | 6 | L50 | 6 | 4 |
| DE0304Z | D3 | 8 | L50 | 3 | 4 |
| DE0304A | D3 | 8 | L50 | 4 | 4 |
| DE0304 | D3 | 8 | L50 | 6 | 4 |
| DE0354A | D3.5 | 10 | L50 | 4 | 4 |
| DE0354 | D3.5 | 10 | L50 | 6 | 4 |
| DE0404A | D4 | 10 | L50 | 4 | 4 |
| DE0404 | D4 | 10 | L50 | 6 | 4 |
| DE0454 | D4.5 | 11 | L50 | 6 | 4 |
| DE0504Z | D5 | 13 | L50 | 5 | 4 |
| DE0504 | D5 | 13 | L50 | 6 | 4 |
| DE0554 | D5.5 | 15 | L50 | 6 | 4 |
| DE0604 | D6 | 15 | L50 | 6 | 4 |
| DE0704 | D7 | 18 | L60 | 8 | 4 |
| DE0804 | D8 | 20 | L60 | 8 | 4 |
| DE0904 | D9 | 23 | L75 | 10 | 4 |
| DE1004 | D10 | 25 | L75 | 10 | 4 |
| DE1004L | D10 | 30 | L75 | 10 | 4 |
| DE1104 | D11 | 30 | L75 | 12 | 4 |
| DE1204 | D12 | 30 | L75 | 12 | 4 |
| DE1404 | D14 | 35 | L100 | 14 | 4 |
| DE1604 | D16 | 45 | L100 | 16 | 4 |
| DE1804 | D18 | 45 | L100 | 18 | 4 |
| DE2004 | D20 | 50 | L100 | 20 | 4 |
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|
| DEX0104A | D1 | 3 | L50 | 4 | 4 |
| DEX0104 | D1 | 3 | L50 | 6 | 4 |
| DEX0154A | D1.5 | 4 | L50 | 4 | 4 |
| DEX0154 | D1.5 | 4 | L50 | 6 | 4 |
| DEX0204A | D2 | 6 | L50 | 4 | 4 |
| DEX0204 | D2 | 6 | L50 | 6 | 4 |
| DEX0254A | D2.5 | 6 | L50 | 4 | 4 |
| DEX0254 | D2.5 | 6 | L50 | 6 | 4 |
| DEX0304Z | D3 | 8 | L50 | 3 | 4 |
| DEX0304A | D3 | 8 | L50 | 4 | 4 |
| DEX0304 | D3 | 8 | L50 | 6 | 4 |
| DEX0404A | D4 | 10 | L50 | 4 | 4 |
| DEX0404 | D4 | 10 | L50 | 6 | 4 |
| DEX0504Z | D5 | 13 | L50 | 5 | 4 |
| DEX0504 | D5 | 13 | L50 | 6 | 4 |
| DEX0604 | D6 | 15 | L50 | 6 | 4 |
| DEX0804 | D8 | 20 | L60 | 8 | 4 |
| DEX1004 | D10 | 30 | L75 | 10 | 4 |
| DEX1204 | D12 | 30 | L75 | 12 | 4 |
| DEX1404 | D14 | 35 | L100 | 14 | 4 |
| DEX1604 | D16 | 45 | L100 | 16 | 4 |
| DEX1804 | D18 | 45 | L100 | 18 | 4 |
| DEX2004 | D20 | 50 | L100 | 20 | 4 |
| Type No. | Diameter (D, mm) | Flute length (Lc, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|
| DE0606 | D6 | 15 | L50 | 6 | 6 |
| DE0806 | D8 | 20 | L60 | 8 | 6 |
| DE1006 | D10 | 25 | L75 | 10 | 6 |
| DE1206 | D12 | 30 | L75 | 12 | 6 |
| DE1406 | D14 | 35 | L100 | 14 | 6 |
| DE1606 | D16 | 40 | L100 | 16 | 6 |
| DE2006 | D20 | 45 | L100 | 20 | 6 |
| Type No. | Diameter (D, mm) | Corner R (R, mm) | Flute length (Lc, mm) | Effective length (L1, mm) | Overall length (L, mm) | Shank Dia (d, mm) | Flutes (F) |
|---|---|---|---|---|---|---|---|
| EE0104A | D1.0 | — | 2 | — | L50 | 4 | 4 |
| EE0154A | D1.5 | — | 3 | — | L50 | 4 | 4 |
| EE0204A | D2.0 | — | 4 | — | L50 | 4 | 4 |
| EE0254A | D2.5 | — | 5 | — | L50 | 4 | 4 |
| EE0304A | D3.0 | — | 6 | — | L50 | 4 | 4 |
| EE0404A | D4.0 | — | 8 | — | L50 | 4 | 4 |
| EE0604 | D6.0 | — | 15 | 20 | L50 | 6 | 4 |
| EEH0604 | D6.0 | — | 15 | 20 | L75 | 6 | 4 |
| EEI0604 | D6.0 | — | 15 | 20 | L100 | 6 | 4 |
Explore our workshop equipment and specify square-end tools by model, cutter diameter and flute count.
CNC tool grinding equipment; square-end orders are specified by cutter diameter and end profile.
Multi-tank cleaning equipment; include any required surface condition with the sample specification.
CNC grinding machines supporting tool production; flute count distinguishes the listed square-end models.
Tool grinding equipment; cutting length matters when selecting a cutter for slots or shoulders.
Automated grinding cell; model and drawing references help identify repeat-order requirements.
Automated tool handling alongside grinding equipment; list each diameter and flute combination separately.
CNC grinding machines in the workshop; compare the cutter profile with the feature drawing.
Tool-coating equipment; state the coating specification if it is required for your order.
Coating-area equipment; finish requirements should reflect the intended workpiece and operation.
Laser-marking station; provide the model identification or marking format required for your order.
Tool-finishing workstations; the selected square-end model determines the features to review.
Cutting-edge preparation equipment; edge condition can be included in the tool drawing.
Edge honing and polishing equipment; specify any required corner condition for the selected cutter.
Wet-blasting equipment; identify finish requirements by series when requesting a quote.
Another view of wet-blasting equipment; associate any finish request with the correct model.
For square-end orders, identify the dimensions and edge features required for your sample and purchase specification.
Tool inspection room; agree on sample inspection dimensions before placing a repeat order.
Profile-measuring station; cutter diameter and end geometry are useful inspection references.
Measurement workstations; check shank diameter and tool lengths against the model table.
Balancing instrument; include any balance requirement relevant to the machine and application.
Tool presetter; holder fit and projection are relevant when setting up a square-end cutter.
Optical tool presetter; record length references consistently for the intended setup.
Optical inspection workstations; identify the end and edge features required for sample acceptance.
Tool-measuring equipment; the approved drawing defines the dimensions to review.
A square end mill is selected for milling tasks such as slots, pockets, shoulders and flat surfaces where its nominally flat end is appropriate. Match its diameter, cutting length, holder and toolpath to the feature and machine.
A square end mill has a nominally flat cutting end, while a ball nose end mill has a rounded end profile. Select the geometry from the part feature and programmed toolpath; the two profiles do not produce the same surface shape.
Consider the work material, operation, chip evacuation, machine and engagement. Compare the actual model tables for the required diameter and dimensions, because a given flute count may not be offered in every series or size.
Check the required cutting depth, flute length, tool reach, overall length and holder clearance. Do not treat overall length as the same thing as usable cutting length. Compare the catalogue drawing with the actual feature and setup.
The catalogue identifies the four-flute EE group as a copper-electrode series. Provide the model, workpiece and feature requirements so the selected item can be checked against the corresponding catalogue record.
Send your model list and quantity by model. If you do not have model numbers, provide cutter diameter, flute count, cutting length, overall length, shank diameter, workpiece and operation. Add any drawing, packaging or marking requirements relevant to your order.
Send the catalog models, quantities, workpiece material, operation, machine and holder requirements. Unconfirmed values will be reviewed rather than assumed.
Carbide Cutting Tools · Ball Nose End Mills · Corner Radius End Mills · Micro Diameter End Mills