A burr can have the right shape and still be the wrong size. Head diameter changes contact and speed. Shank diameter determines collet fit. This Carbide Burr Size Chart helps you specify an industrial range without treating metric and inch sizes as interchangeable.
How to Read Carbide Burr Dimensions
A useful size record separates the cutting head from the machine interface. If a quotation says only ‘10 mm burr’, you do not know the cutting length, shank, overall length or whether the model fits the customer's grinder. Use four dimensions on every product drawing, data sheet and purchase order.
Keep the drawing revision and SKU beside these dimensions. That link prevents two visually similar burrs from being mixed during sample approval, label production or replenishment.
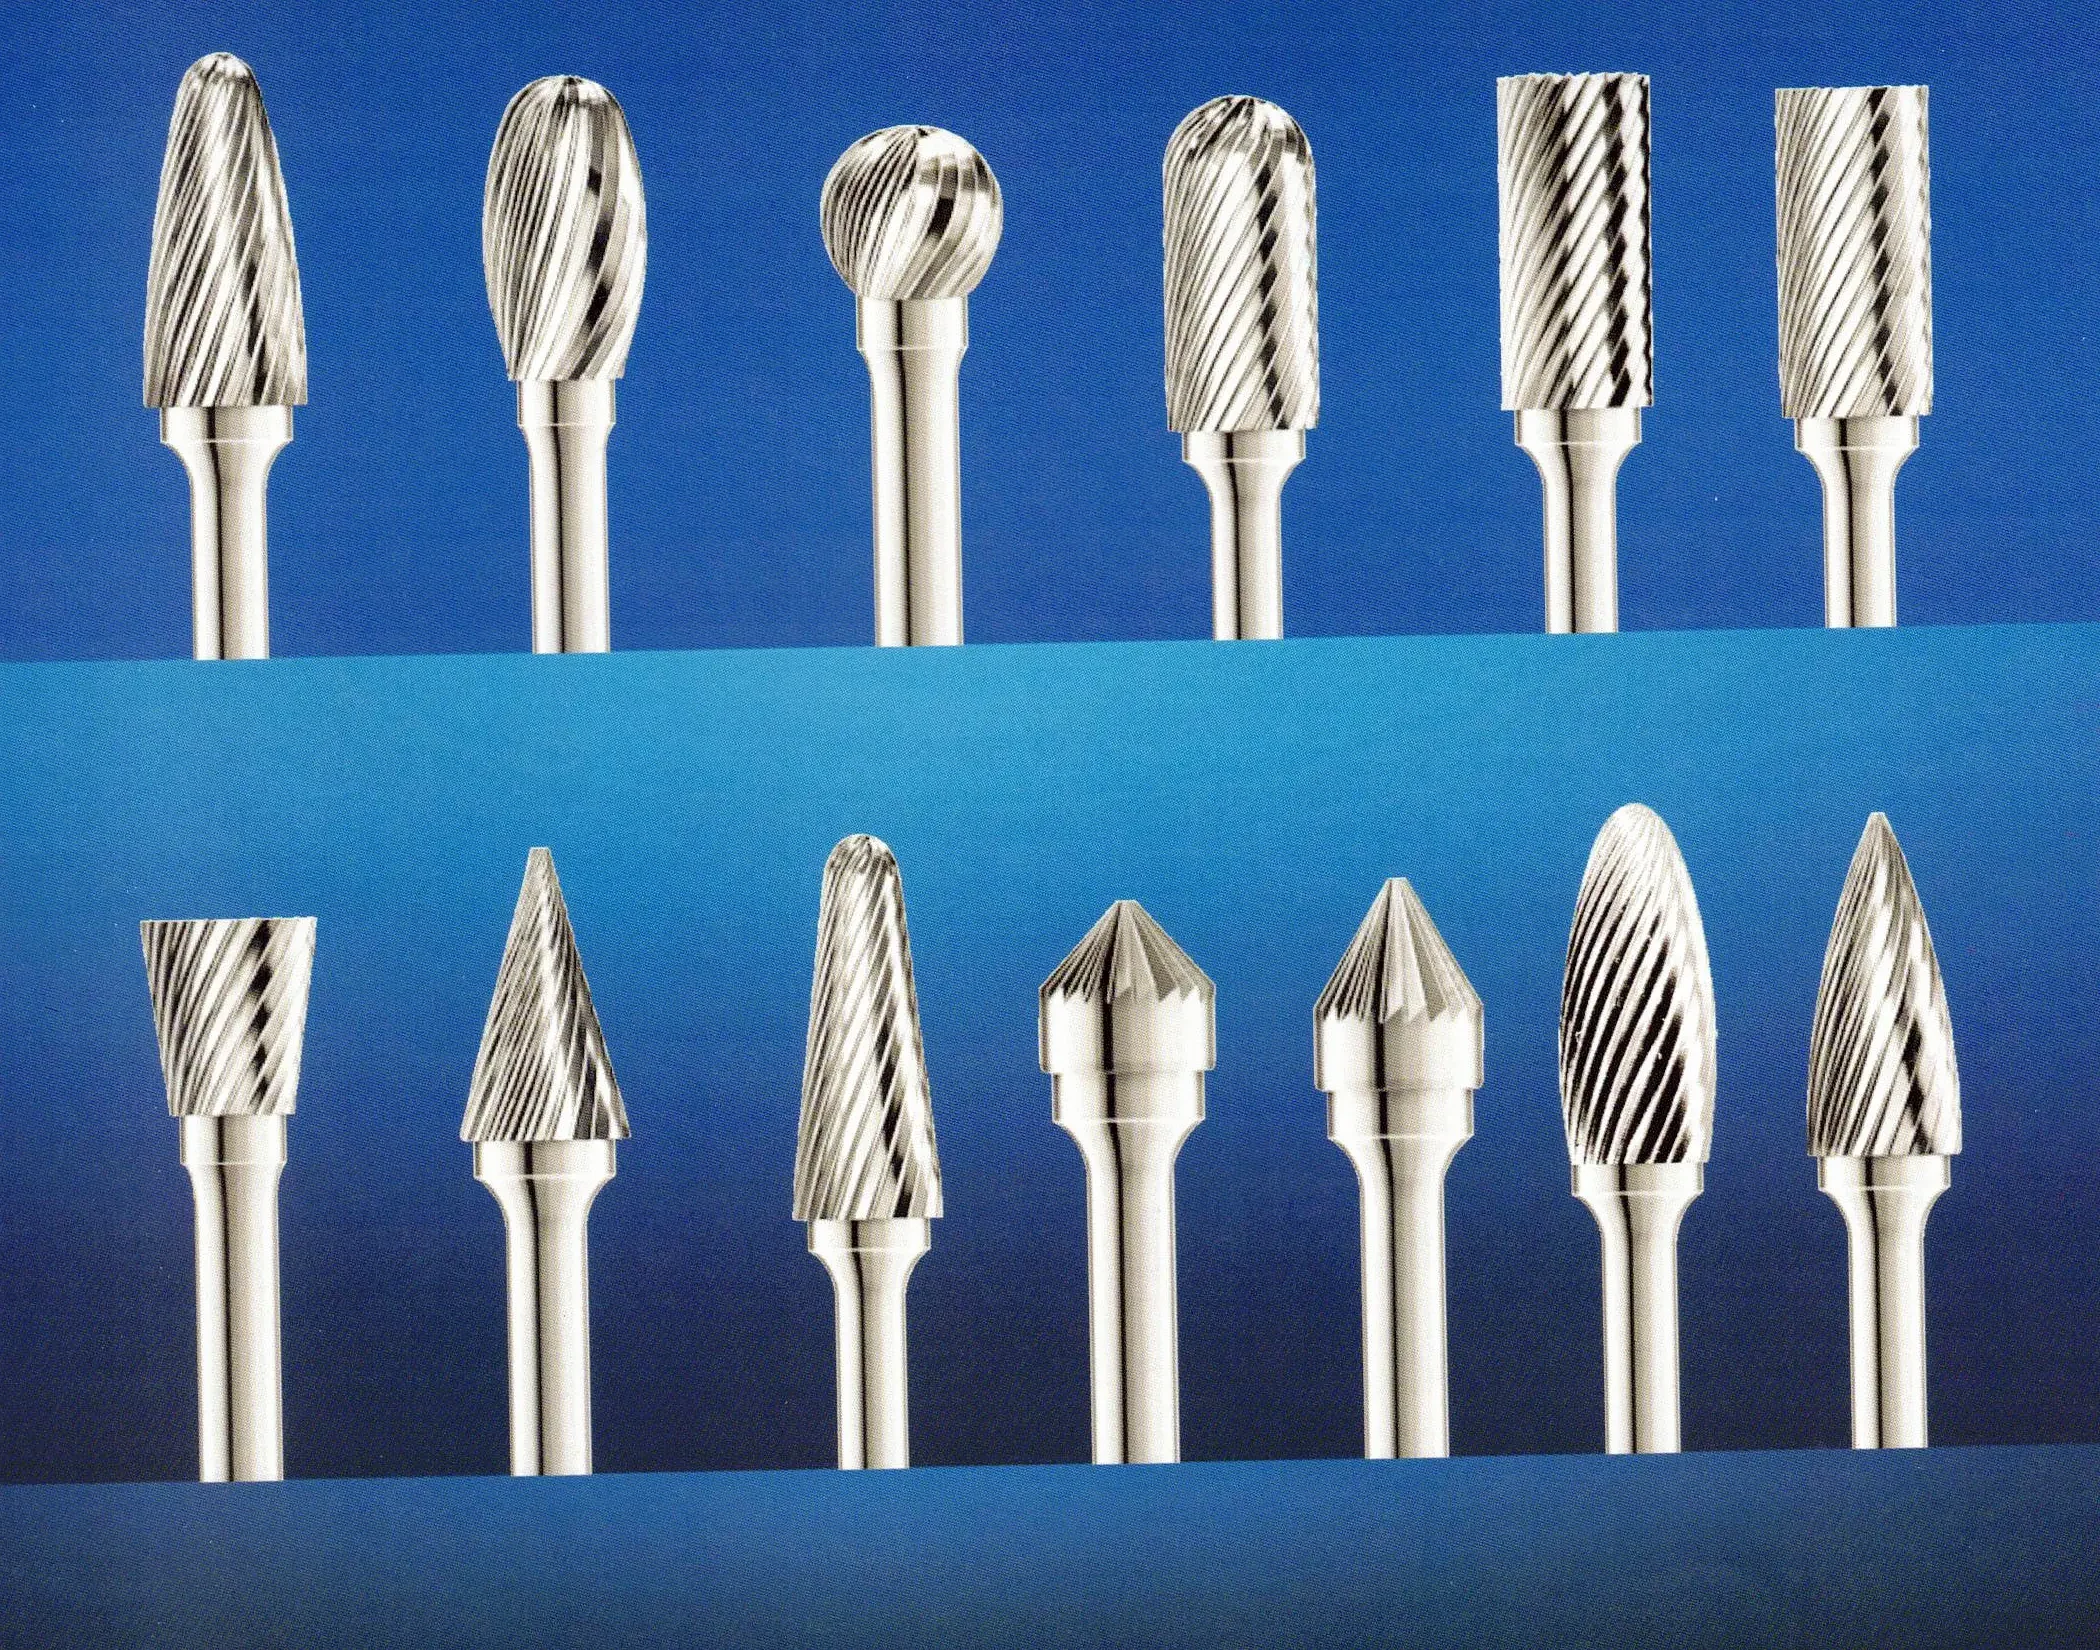
Dimensions tell you whether a burr fits the machine and available space. Head shape determines where its cutting surface meets the part. Compare the profiles in thecarbide burr shape chartbefore selecting the dimensions for that shape.
| Code | Dimension | What You Should Record | Why It Changes Selection |
|---|---|---|---|
| d1 | Head Diameter | Maximum cutting diameter | Controls access, contact area and RPM lookup row |
| l2 | Cutting Length | Usable fluted length | Controls reach across an edge, weld or cavity |
| d2 | Shank Diameter | Metric or inch interface | Must match the installed collet |
| l1 | Overall Length | Tip-to-shank-end length | Affects reach, overhang and packaging |
Carbide Burr Head Sizes and Cutting Length
Carbide Burr Head Sizes should be selected from the feature you need to machine, not from a belief that the largest head is always more productive. Smaller heads enter tight radii and cross-holes. Larger heads cover open surfaces faster, but they also increase contact, torque demand and the consequence of runout.
Cutting length is a separate decision. A short head gives better support in a shallow feature. A longer cutting section covers a deeper wall or wider weld, but it creates more leverage when engagement moves away from the collet. Specify the shortest cutting length that fully reaches the working area, then confirm overall length and overhang.
| Head Diameter Band | Best Starting Use | Buyer Check Before Ordering |
|---|---|---|
| 3–6 mm | Fine deburring, small bores, narrow slots and detailed contours | Confirm the grinder can reach the required RPM and that the shank/collet combination is rigid |
| 8–10 mm | General fabrication, casting cleanup and controlled weld dressing | Match shape and cutting length to the contact zone; verify available drive power |
| 12–16 mm | Open edges, larger castings and higher-volume stock removal | Check grinder speed range, power, access and allowed contact area before qualification |
Carbide Burr Shank Sizes and Collet Fit
Carbide Burr Shank Sizes are machine interfaces. Treat each nominal size as its own standard. A grinder may accept several sizes only when the correct dedicated collet and nut are installed; a list of supported collets does not mean one collet clamps every size.
Compatibility Rule: Do not place a 6 mm shank in a 1/4-inch collet or a 3 mm shank in a 1/8-inch collet unless the grinder manufacturer provides a purpose-made reducing system for that exact combination. Never use improvised sleeves or shims.
Use a dedicated Carbide Burr Shank Size Guide when you need a deeper comparison of regional tool interfaces. For assortment planning, put the shank standard in the SKU name, barcode description and carton label so a metric model is never substituted by its nearby inch size.
Carbide Burr Shank Sizes are machine interfaces. Treat each nominal size as its own standard. A grinder may accept several sizes only when the correct dedicated collet and nut are installed. Compatibility Rule: Do not place a 6 mm shank in a 1/4-inch collet or a 3 mm shank in a 1/8-inch collet unless the grinder manufacturer provides a purpose-made reducing system. Never use improvised sleeves or shims. Put the shank standard in the SKU, barcode description and carton label.
| Burr Shank | Exact Diameter | Required Collet | Commercial Use |
|---|---|---|---|
| 3 mm | 3.000 mm | 3 mm | Metric miniature and precision ranges |
| 1/8 inch | 3.175 mm | 1/8 inch | Inch-market rotary tools and small die grinders |
| 6 mm | 6.000 mm | 6 mm | Metric industrial die grinders |
| 1/4 inch | 6.350 mm | 1/4 inch | North American industrial die grinders |
Carbide Burr RPM Chart by Head Diameter
RPM comes from cutting speed, head diameter, material and tooth geometry. The table below reproduces published diameter-to-RPM relationships at selected cutting speeds. First obtain the correct cutting-speed band for the material and cut, then read across the diameter row. These are reference values, not universal AXIMET model limits.
A Carbide Burr Speed Chart that lists only diameter and RPM is incomplete. It should state the cutting-speed basis, workpiece family, cut type, shank/overhang condition and whether the number is a working range or a maximum. A supplier's Carbide Burr Recommended Speed should carry the same context into the data sheet.
| Head Diameter | 250 m/min | 450 m/min | 600 m/min | 750 m/min | 900 m/min |
|---|---|---|---|---|---|
| 3 mm | 27,000 | 48,000 | 64,000 | 80,000 | 95,000 |
| 6 mm | 13,000 | 24,000 | 32,000 | 40,000 | 48,000 |
| 8 mm | 10,000 | 18,000 | 24,000 | 30,000 | 36,000 |
| 10 mm | 8,000 | 14,000 | 19,000 | 24,000 | 29,000 |
| 12 mm | 7,000 | 12,000 | 16,000 | 20,000 | 24,000 |
| 16 mm | 5,000 | 9,000 | 12,000 | 15,000 | 18,000 |
How to use the table:Do not choose a column by material name alone. Confirm the burr manufacturer's cutting-speed recommendation for the exact material group and cut. The lowest rating among burr, grinder, collet and accessory governs.
How to Find the Best RPM for Carbide Burr Work
There is no single Best RPM for Carbide Burr work. Pressure, contact area and runout are part of the same approval. Use this qualification sequence for each model and application:
- Confirm the workpiece material, burr cut, head diameter, shank and protruding length.
- Obtain the burr supplier's published cutting-speed band and maximum rotational speed.
- Confirm the grinder's controllable speed range, collet size, power and accessory rating.
- Select the diameter row and begin qualification at the lower end of the approved working band.
- Use light, moving contact and observe chip formation, sound, vibration, heat, finish and tooth loading.
- Increase only within the approved range; stop if chatter, color change, rubbing or unstable cutting appears.
- Record the accepted setup with the SKU so repeat orders carry the same operating basis.
How to Adjust Speed for Long-Shank Burrs
Long reach increases bending leverage. Do not apply a standard-shank RPM to an extended model. Use a rigid drive and clamping system, minimize exposed shank, and follow the long-shank limits published for that exact tool. Some manufacturers also distinguish maximum idling speed from maximum application speed with the burr already in contact.
Published Long-Shank Example: The table is a manufacturer-specific reference for selected long-shank burrs, not a substitute for the supplier's current model data. If the exact long-shank rating is unavailable, do not infer it from a neighboring diameter or length.
| Head Diameter | Shank Length | Maximum Idling RPM | Maximum Application RPM |
|---|---|---|---|
| 3 mm | 75 mm | 10,000 | 31,000 |
| 6 mm | 75 mm | 6,000 | 15,000 |
| 6 mm | 150 mm | 8,000 | 15,000 |
| 8 mm | 150 mm | 6,000 | 11,000 |
| 10 mm | 150 mm | 4,000 | 9,000 |
| 12 mm | 150 mm | 3,000 | 7,000 |
Can You Use Carbide Burrs in a High-Speed Rotary Tool?
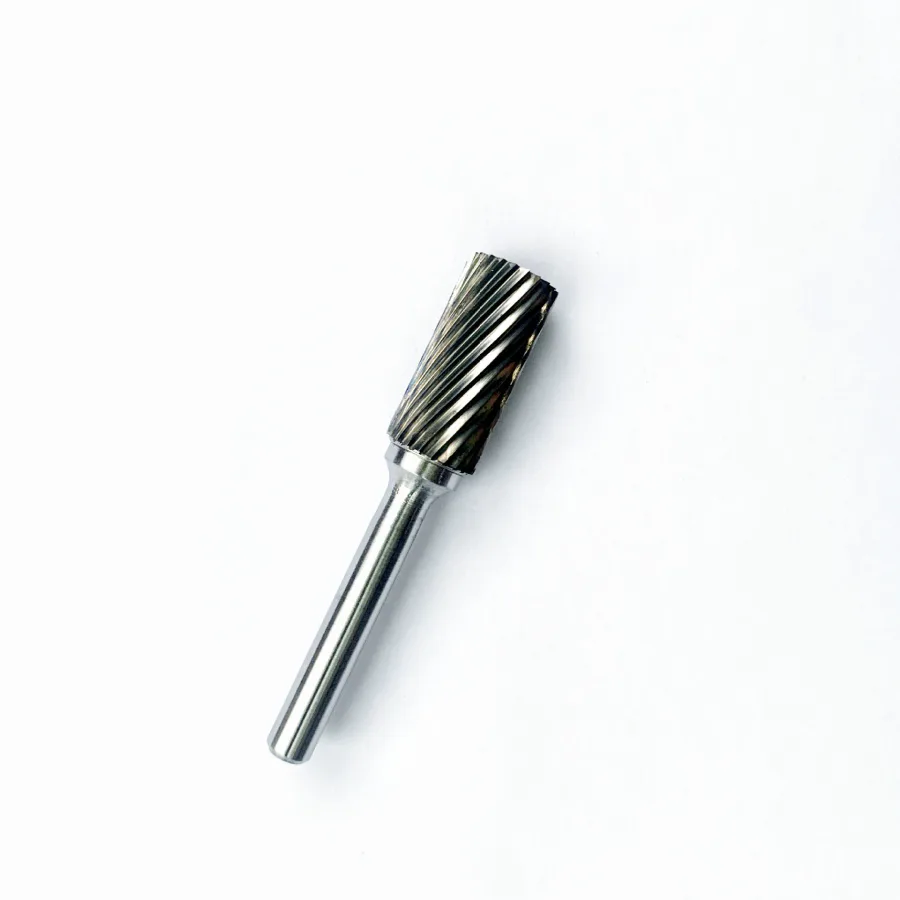
When selecting a Carbide Burr for High Speed Rotary Tool applications, you must check more than its advertised no-load RPM. Confirm the exact collet, accessory diameter rating, motor power, duty cycle and exposed shank. Compact tools may reach high speed yet lack the rigidity or power required for a large head under load.
For a 3 mm or 1/8-inch program, ask customers which tool platforms they actually use and whether the correct collet is available. Do not market every miniature burr as universally compatible with compact rotary tools. For 6 mm and 1/4-inch industrial ranges, qualify the burr on representative pneumatic or electric die grinders used in the target market.
How to Choose Carbide Burr Sizes for Your Product Range
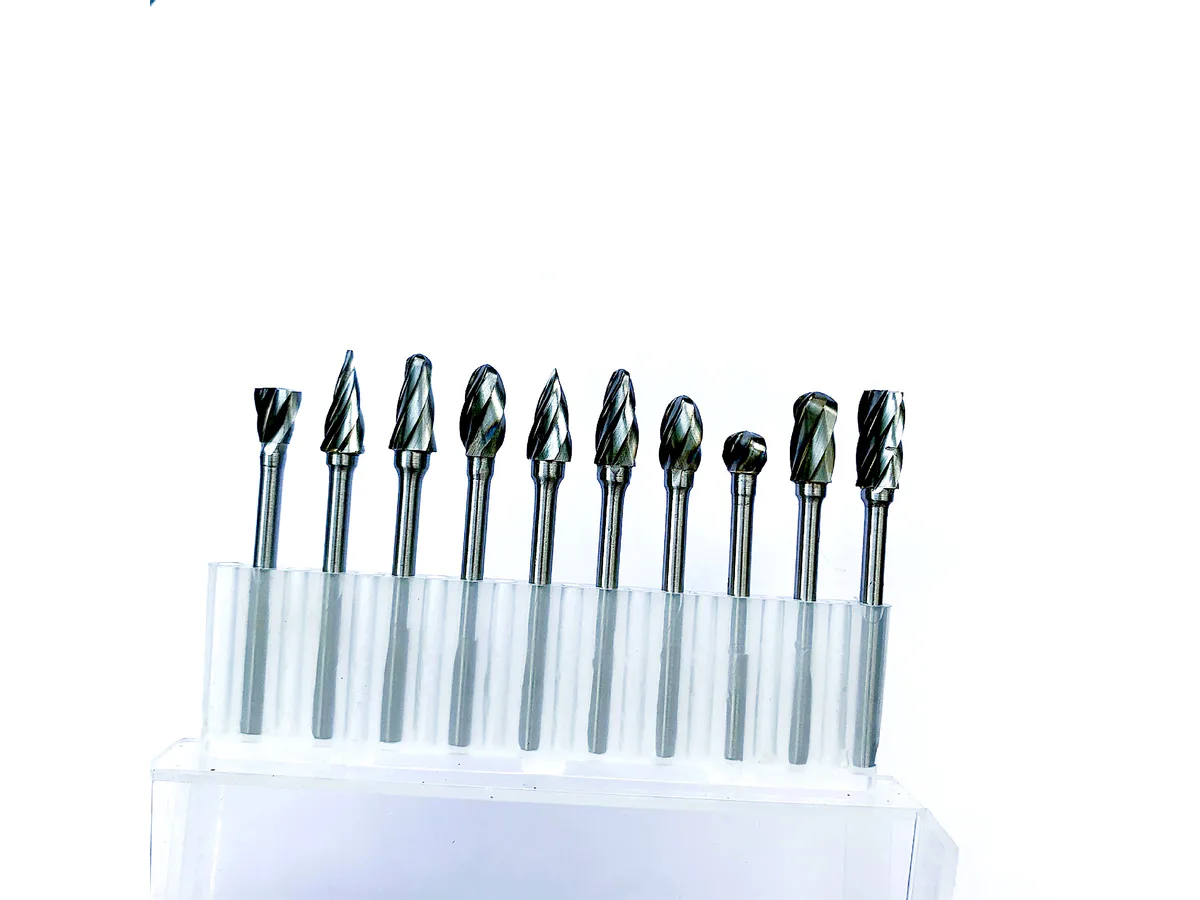
A distributor does not need every head in every length and shank. Start with customer operations and grinder interfaces, then create deliberate coverage. This avoids duplicate inventory and makes technical sales easier.
When comparing head-size ranges across suppliers, align the same four dimensions, cut and material application. A lower unit price is not comparable if cutting length, head construction, runout standard or packaging protection differs.
- Segment the market by metric and inch grinder platforms before selecting SKUs.
- Use 3–6 mm heads for precision access, 8–10 mm for general fabrication and 12–16 mm for open high-removal work.
- Choose shapes from the component geometry: flats, radii, slots, contours, chamfers or cross-holes.
- Keep standard and long-shank models in separate families with separate operating guidance.
- Give every shape-size-cut-shank combination its own replacement code, even when sold in a set.
- Use sales history and application feedback to expand the range instead of adding adjacent sizes without a distinct role.
OEM Quotation Data Checklist
A complete RFQ should allow the supplier to identify the product, application and commercial format without guessing. Include:
Attach a customer application photo or drawing when access is difficult. It often reveals whether the requested issue is head diameter, cutting length, overall reach or the wrong burr shape.
- Shape code or approved profile drawing
- Head diameter (d1) and cutting length (l2)
- Shank diameter (d2), metric or inch standard, and overall length (l1)
- Standard, extended or flexible shank construction
- Cut type, tooth grade and target workpiece materials
- Grinder type, collet, controllable RPM range and typical duty cycle
- Required dimensional tolerances and sample inspection method
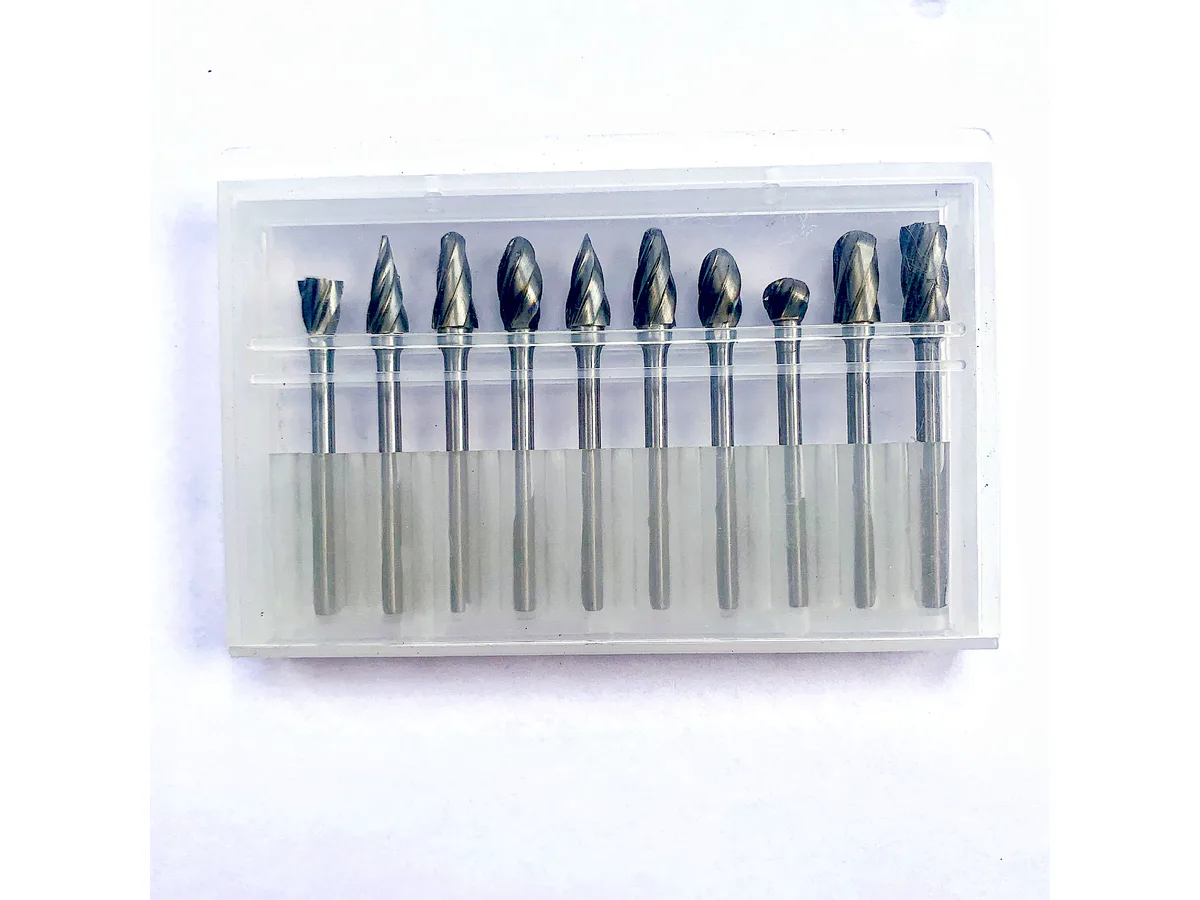
- Individual or set configuration, replacement SKU plan and pack quantity
- Laser marking, barcode, label language, artwork and packaging requirements
- Sample quantity, initial order quantity, annual forecast and destination market
Frequently Asked Questions
Should distributors stock both metric and inch shanks?
Yes, when customer equipment uses both systems. Keep metric and inch models as separate SKUs, labels and replacement codes. Do not merge 3 mm with 1/8 inch or 6 mm with 1/4 inch.
Does a larger carbide burr head always remove material faster?
No. Removal rate also depends on cut, material, grinder power, contact area, pressure and usable RPM. Select the smallest head that provides the required reach and productive contact.
Which dimensional tolerances should buyers compare during sample approval?
Compare head diameter, cutting length, shank diameter, overall length and head-to-shank alignment using one agreed method. Add runout, tooth condition and visible joint quality.
How do buyers choose carbide burr head diameter and cutting length?
Choose the smallest head that clears the feature and the shortest cutting length that reaches the full working zone. Approve every head-length combination on representative parts.
Which RPM should be used for each burr diameter?
Use diameter only after confirming the manufacturer's cutting-speed range for the exact material and cut. The lowest rating among burr, grinder and collet governs.
Which collet fits 3 mm, 6 mm, 1/8-inch and 1/4-inch shanks?
Each shank needs its matching collet. Verify the collet and nut against the grinder model; do not use sleeves or rely on nominally close sizes.
Are 6 mm and 1/4-inch shanks interchangeable?
No. A 6 mm shank measures 6.000 mm, while 1/4 inch measures 6.350 mm. They require separate collets.
How should speed be adjusted for long-shank carbide burrs?
Use the exact model limit, minimize exposed length and keep the drive rigid. If no value is published, do not infer one from an adjacent size.
Which size data should be included in an OEM quotation?
Include shape, head diameter, cutting length, shank diameter, overall length, cut, workpiece and grinder interface, plus tolerances, quantity, packaging, marking and barcode requirements.
Final Thoughts
Use the chart to shortlist a size, then validate cut, material and RPM on the customer's application. For an OEM range, send AXIMET TOOLS your grinder interfaces, size matrix, packaging and annual volume. Review thecarbide burr rangeor request a technical quotation.
Request a Size and RPM Review | Get an OEM Quotation
Related Product and Buyer Guides
- Tungsten Carbide Burrs
- 6mm Shank Carbide Burr
- Carbide Burr Shapes
- Cylindrical Carbide Burr
- Carbide Burr Shank Size Guide