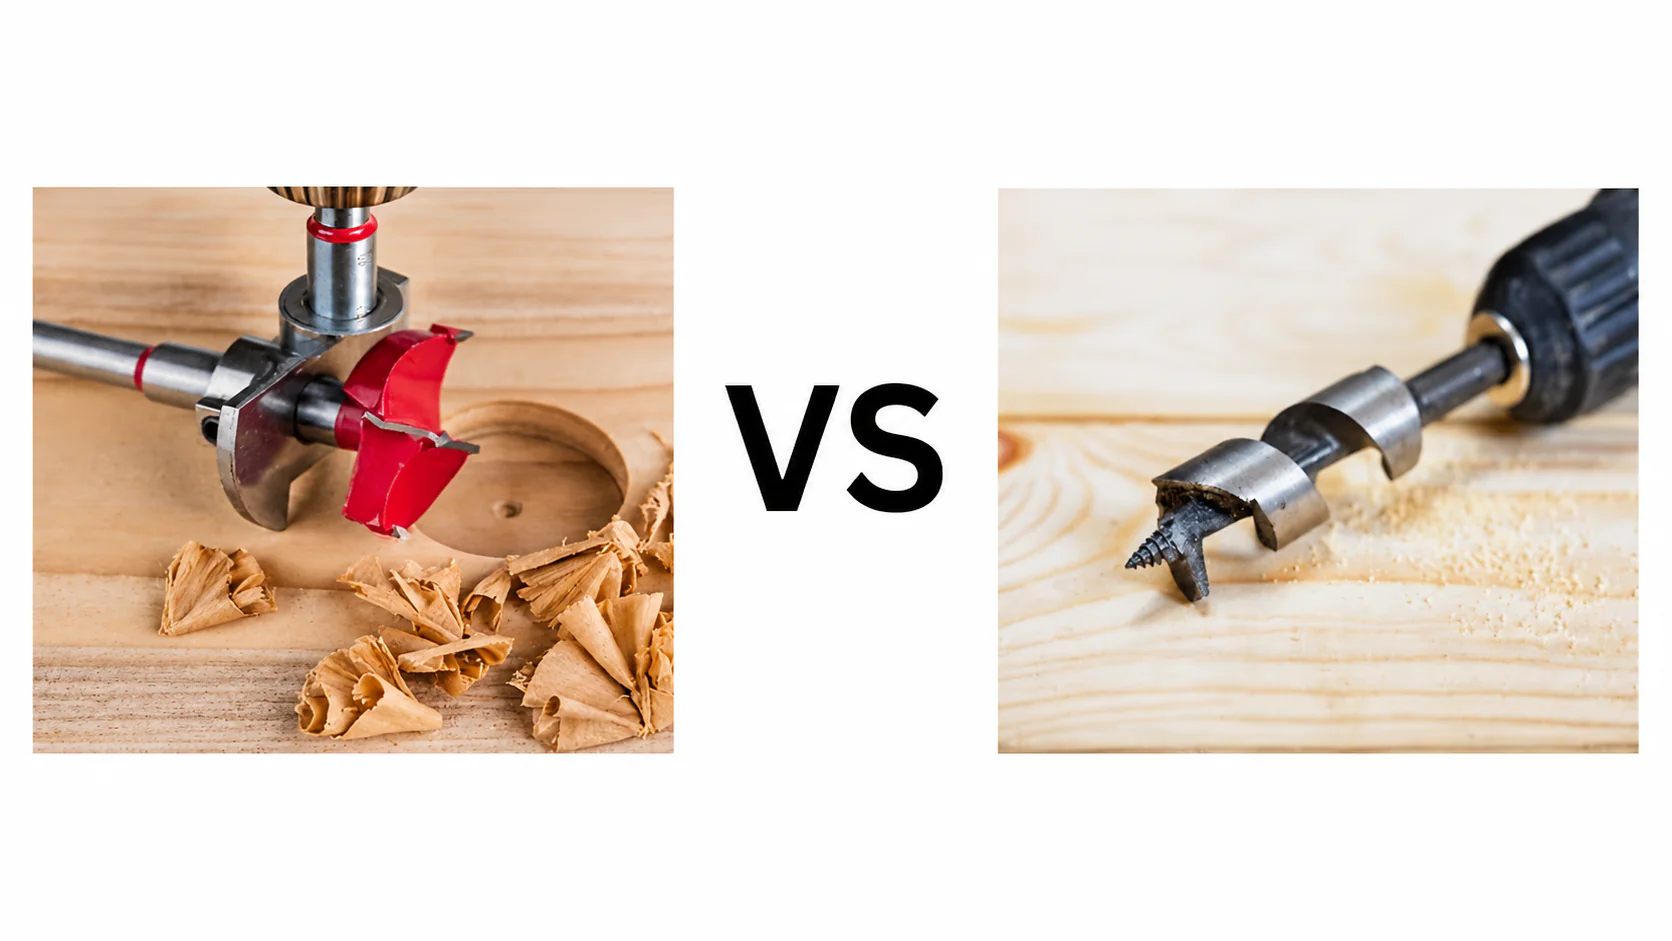
Choose a Forstner bit for a controlled recess or a hole whose bottom and rim matter. Choose an auger bit when deeper wood boring and chip transport dominate the job. Compare the exact geometry, usable depth and machine; matching diameters do not make the two tools interchangeable.
Start With the Finished Hole
The most useful difference between a Forstner bit and an auger bit is the hole each cutting structure is intended to produce. A Forstner head cuts around a broad circular area and is commonly selected for stopped recesses. An auger combines cutting edges with a spiral body that moves chips out of a deeper bore. Both remove wood, but they solve different production problems.
Write the hole requirement before choosing the tool. Is it a blind recess for hardware, a through-hole in a beam, or a bore that must meet another opening? Which surface will remain visible? Must the bottom support a fitting, or does only the clearance through the timber matter? These questions separate an appropriate tool from one that merely has the right diameter.
Depth must also mean the depth of the actual feature. A broad shallow recess is not equivalent to a narrow passage through thick timber. The drawing should distinguish recess depth, through thickness and any extra point penetration. Once those requirements are clear, compare the bit's working geometry rather than relying on a general wood-drilling label.
Read the Cutting Structures
What a Forstner Head Does
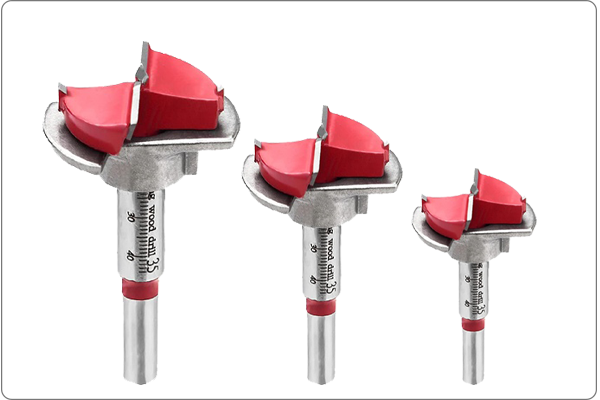
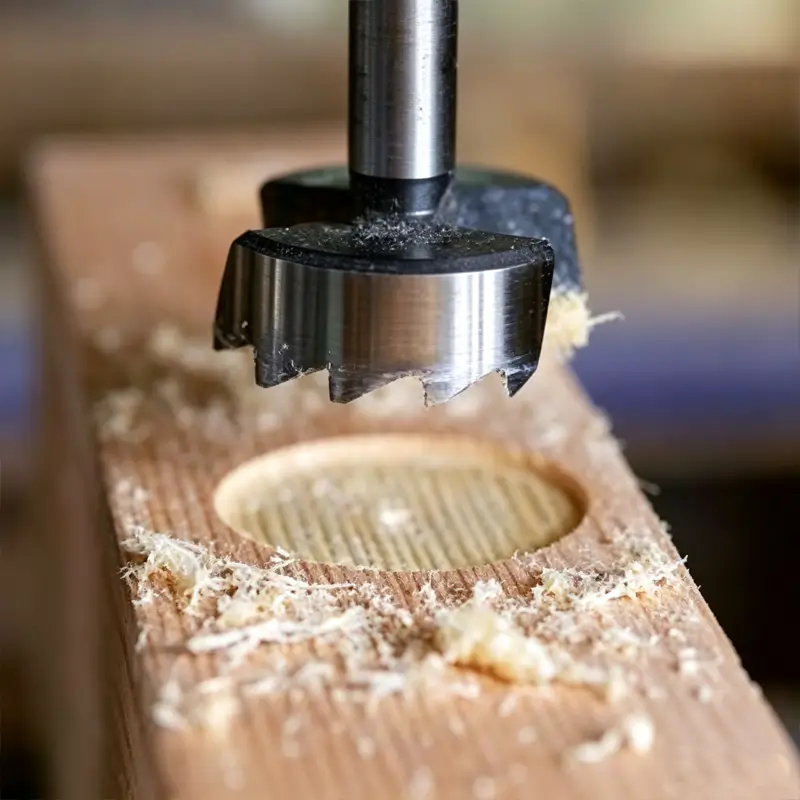
A typical Forstner bit has a center point, peripheral cutting features and cutters that remove material inside the circle. The perimeter helps define the hole boundary while the inner cutting edges form the recess. Details vary: smooth rims, toothed rims and other modified profiles have different cutting behavior. The family name does not specify every head geometry or permitted application.
Forstner bits are useful where a controlled stopped hole and bottom form matter, such as a hardware recess. Flat-bottomed is a practical description, not a promise that the entire bottom has no mark. A projecting center point can leave a deeper indentation. Check that point against the remaining panel thickness and the clearance required beneath the fitting.
Some designs support edge drilling, overlapping holes or angled entries. Treat those as design-specific applications that require suitable guidance and workholding, not automatic permissions for every Forstner bit. A part of the rim cutting into open space is a different starting condition from a full circle on a flat surface. The setup must keep the bit and workpiece controlled.
What an Auger Adds
An auger has a helical body with space for chips and, in many common wood-boring designs, a threaded lead point. The point helps locate the start and draws the tool forward as it rotates. Cutting edges remove the wood and the flute provides a route for the chips. Exact screw form, cutting lips and spiral design vary between patterns.
The lead point changes the feel of the cut. A self-feeding action can reduce the push needed to advance, but it also means the tool can pull into the work more assertively than expected. The operator needs a machine and holding position suitable for the resulting reaction. More self-feed is not automatically more control, particularly in a restricted working space.
An auger is relevant when a deeper bore needs reach and effective chip movement. Its threaded point also projects ahead of the main cutting diameter. That matters near the far face, inside a blind feature or wherever another component lies beyond the wood. Overall length alone does not explain either the available chip space or the depth the selected tool can complete.
Compare Forstner and Auger Bits Directly
| Selection Question | Forstner Bit | Auger Bit |
|---|---|---|
| What is the main hole requirement? | Controlled recess, defined rim and bottom form | Deeper wood bore with reach and chip transport |
| What locates or advances the tool? | Center point and head geometry; feed depends on design | Commonly a threaded lead point with self-feeding action |
| What occupies the bottom of a blind hole? | Broad cut bottom, usually with a local center-point mark | Lead point and head geometry do not produce the same recess bottom |
| How are chips handled? | Clearance around the head requires attention as depth increases | Helical flute provides a chip-transport path |
| What does the diameter fail to describe? | Point projection, rim, head depth and shank | Screw form, flute length, working reach and shank |
| Which setup details matter? | Stable support, depth control and suitable guidance | Reaction control, alignment, reach and chip clearance |
This comparison describes the families rather than an interchangeability rule. A particular bit may have a specialized design that changes its range of uses. Compare the actual tool instructions and geometry when the work involves a critical surface, restricted access or an operation outside ordinary straight boring. A convenient general description is not a substitute for that check.
Consider two jobs with the same nominal diameter: a stopped seat for a hinge cup and a passage through timber. The first is selected around the fitting's recess and remaining wall; the second around the full route, access and chip clearance. They can justify different tool families even at the same diameter. Compare the finished feature before comparing purchase prices.
Choose Forstner Geometry for Recesses and Hardware Seats
For a stopped recess, specify diameter and bottom depth separately. A fitting may locate against the sidewall, sit on the bottom or require clearance around both. If the tool's center point projects beyond the broad bottom, include that projection when checking the material remaining beneath the recess. This is especially important in a thin panel where the point could mark the opposite face before the intended seat is complete.
Check the actual panel or timber, not only its nominal thickness. Surface veneers, coatings and an uneven face can influence the acceptable depth and appearance. When the fitting has its own installation drawing, use that requirement to establish the hole rather than selecting the nearest diameter by eye. Fit and finish are part of the same decision.
A drill press can provide useful alignment and depth control where the bit and work allow it. A handheld setup may also be permitted by a particular tool, but keeping the axis and depth steady requires suitable support. Do not treat the ability to clamp the shank as proof that every portable drilling arrangement will make a controlled recess.
Choose Auger Geometry for Reach and Chip Movement
For a deeper timber hole, compare working length and flute length with the entire path through the material. A long plain shank can improve access without providing the same continuous chip space as a longer fluted body. Two augers with similar overall lengths can therefore behave differently in a deep bore. Describe the needed reach rather than ordering by length alone.
Consider the lead screw's behavior in the actual wood. Wood density, grain direction, knots and the tool's screw design can change how it feeds. An auger that enters readily in one timber should not be assigned the same feed behavior in every species or engineered panel. Select a design whose material guidance includes the work you intend to perform.
Provide room for chips to leave the flute and for the operator to maintain the drilling axis. A confined recess can obstruct chip discharge even when the tool reaches the far end of the hole. Do not allow packed chips, unexpected resistance or an uncontrolled pull to continue simply because the auger is intended for deep boring. Stop and review the setup.
Keep Spade Bits in Their Own Role
A spade bit is a third family, recognizable by its flat cutting body. It is commonly considered for general wood through-holes, but its point, spurs and feed design still determine its application. Some forms have self-feeding points; others do not. The flat outline alone does not tell you its finished-hole quality or the machine mode it permits.
In a three-way choice, a controlled bottom requirement points toward suitable Forstner geometry, while a deeper passage emphasizes the auger's flute and reach. A spade bit may fit a simpler through-hole task where its finish and access are acceptable. Keep that comparison brief and job-based rather than suggesting that one family is a universal upgrade over the other two.
A hole saw introduces another cutting structure and is not an auger or Forstner substitute merely because the diameter is available. It removes a ring and leaves a plug, rather than clearing the entire bore as chips. Where only a through-hole is needed, that may be worth comparing separately; where a flat-bottom recess is required, the finished feature is different.
Separate Overall Length, Working Depth and Installed Clearance
Overall length runs from the tool's end to its tip, but some of that length must sit inside the chuck or holder. Usable depth depends on the cutting and clearance geometry as well as the manufacturer's limits. Installed clearance includes the chuck, machine body and any obstruction near the work. Each dimension answers a different question.
For a drill press, check quill travel and clearance above the workpiece with the actual bit installed. A long tool can reduce the available space for positioning thick timber under the head. For a portable drill, check the approach angle, the room behind the tool and whether the auxiliary handle can be used as intended. Reach that exists on a drawing may not exist in the assembled setup.
Use only an extension intended for the bit, holder and operation. Added length changes the assembly and can increase the effect of runout or misalignment. Do not improvise an extension simply because two components appear to fit. If an extension is required, identify it as part of the operating arrangement and check its restrictions before choosing the tool.
Match the Machine and Feed to the Bit
A compatible shank establishes physical fit, not the machine's ability to drive every head diameter. Compare chuck capacity, the machine's wood-drilling capacity, the required holding arrangement and the bit instructions. A reduced shank does not reduce the load created by a large cutting head. That distinction matters when a bit fits a smaller chuck but needs more control than the machine provides.
There is no single RPM that is correct for all Forstner and auger bits of a given diameter. Cutting geometry, wood, depth and tool design influence the recommendation. Use the speed information for the specific product and material. A specialist high-speed design does not establish a safe speed for a conventional bit that looks similar.
Select the operating mode permitted by both tool and machine. A hex shank does not by itself authorize impact operation, and an SDS-style interface does not mean hammer action is appropriate for wood boring. Follow the bit's stated mode. Keep the machine under control and stop if grabbing, stalling or unexpected reaction makes the cut unstable.
Support the Work and Plan the Exit
Clamp the work securely and keep it supported throughout the cut. A workpiece that can rotate is not controlled simply because it lies flat on a bench or drill-press table. Keep hands clear of the cutting area, use suitable eye protection and secure loose clothing around rotating tools. Adjust stops or inspect the cutting head only with the machine safely stopped.
For a through-hole, identify the face whose edge must remain clean. A well-supported sacrificial backing piece can help support fibers at the exit when the setup permits it. Another method may involve working from both faces, but accurate alignment is then essential. Try the proposed method on representative material instead of assuming the entry and exit will have identical finish.
For blind holes, use dependable depth control that accounts for the point as well as the main cut. Do not judge remaining wall thickness by the visible body alone. Stop to inspect safely when necessary, and clear chips according to the equipment's instructions. A pile of chips can hide the recess edge and make a developing finish problem harder to see.
Diagnose Finish and Cutting Problems by Cause
| Symptom | What to Check First | What Not to Assume |
|---|---|---|
| Ragged entry | Edge condition, surface support and starting alignment | A larger machine alone will improve the rim |
| Torn exit face | Backing, face priority and breakthrough method | A clean entry guarantees a clean exit |
| Burn marks or rubbing | Sharpness, chip clearance and the stated speed/feed guidance | More pressure is always the remedy |
| Hole drifts in deeper timber | Tool length, guidance, grain and machine alignment | A longer auger is automatically straighter |
| Auger pulls in unexpectedly | Lead screw, material and operator reaction control | Self-feed removes the need for control |
| Shank slips or the setup vibrates | Holder engagement, runout and tool condition | Matching nominal shank size proves a sound setup |
Make changes one at a time so the cause remains visible. A fresh bit tested in the same unsupported work can reproduce a breakout problem that was never caused by dullness. Conversely, changing the backing will not restore a damaged cutting edge. Separate the condition of the tool from the support and operating choices around it.
Do not continue with a damaged, bent or unstable bit to finish the last few holes. Inspect the tool with the machine isolated, and follow the manufacturer's sharpening or replacement guidance. Freehand changes to a rim, spur or lead screw can alter the cutting geometry. Regrinding is a tooling operation, not simply a way to make a worn tool look sharp again.
Build a Wood-Boring Assortment Around Real Jobs
For a distributor or production buyer, start with a short list of recurring hole requirements. Separate hardware recesses, general through-holes and deeper timber passages. Then choose diameters and working lengths within the family suited to each job. This creates a useful range without presenting several unlike tools as interchangeable versions of a generic wood bit.
Describe each item with the dimensions and features that affect use. Forstner enquiries need diameter, recess depth, head form and shank. Auger enquiries need diameter, working and overall length, flute and lead-point design, plus the intended machine. Include wood or panel type and the required visible finish for both. Photographs of the application can clarify restricted access or an unusual feature.
Compare Forstner bits by these requirements rather than by assortment size alone. A trial in representative material should check hole form, depth and edge finish under the intended setup. The useful result is whether the tool makes the required feature reliably in that application, not whether the sample simply enters the wood.
Frequently Asked Questions
Is a Forstner Bit Better Than an Auger Bit?
It is better for some hole requirements, not for every wood-drilling task. Choose suitable Forstner geometry when the recess bottom and rim matter. Compare an auger when reach and chip transport are central to a deeper bore. The correct comparison includes the exact head, working length and machine, so matching diameters alone do not identify a substitute.
Does a Forstner Bit Leave a Completely Flat Bottom?
It generally produces a broad, relatively flat recess bottom, but a center point can leave a deeper local mark. Check the actual point projection and the remaining thickness under a blind hole. If a fitting requires uninterrupted contact over the entire bottom, its drawing and the selected tool geometry must agree; flat-bottomed should not be read as mark-free.
Can I Use an Auger for a Blind Hardware Recess?
Do not substitute it simply because the diameter matches. Its lead point, cutting head and helical body are intended for a different boring task and do not create the same broad recess bottom. Check the fitting's seat and clearance requirements first. If the feature needs a controlled flat-bottom form, select tooling designed for that feature.
Can Both Types Be Used in a Handheld Drill?
Some products permit portable drilling, while others or particular operations require a different setup. Check the actual bit and drill instructions, machine capacity and reaction control. A shank that fits the chuck is only one part of compatibility. Large heads, deeper bores and self-feeding points can demand more support and control than the available position allows.
Should Forstner and Auger Bits Run at the Same RPM?
Not automatically. Diameter matters, but head design, material, depth and cutting conditions also affect the recommendation. Use the manufacturer's guidance for the specific bit and wood. Do not apply one brand's specialist high-speed figures to another conventional bit, or assume that choosing a lower gear alone resolves poor chip clearance or an unstable setup.
Where Does a Spade Bit Fit in a Wood-Drilling Set?
It fills a separate role when its flat cutting geometry suits the through-hole, finish and access required. It does not replace the Forstner's recess function or the auger's deep-boring arrangement automatically. Build the set around the jobs performed and compare each tool's point, working length and machine guidance rather than treating all wood bits as one family.
Conclusion
Forstner and auger bits should be selected by the finished feature. A controlled recess emphasizes the Forstner's head and bottom form; deeper wood boring emphasizes the auger's reach, feed and chip transport. In either case, working length, support and machine suitability complete the decision. Diameter is only the start of the specification.
Send AXIMET the wood or panel type, hole diameter, depth, finish requirement and machine details to discuss the appropriate wood-boring selection.