HSS means high-speed steel, a family of tool steels used to make drill bits. It identifies the cutting material, not one universal drill. Choose an HSS drill by its grade, geometry, length, shank and intended workpiece—not by colour or the acronym alone.
What HSS Means on a Drill Bit
An HSS drill bit uses high-speed steel as its cutting material. The name distinguishes this family from ordinary carbon tool steel and from carbide. It does not describe a coating, a particular point angle or a single alloy composition. Two drills marked HSS can therefore belong to different product series and perform differently in the same hole.
For someone buying replacement tooling, that distinction matters immediately. A drill can match the required diameter but have a different reach, point or shank. It may fit the chuck yet struggle to start accurately, clear chips or reach the required depth. None of those questions is settled by the HSS marking.
Think of HSS as the first line in the specification. The rest explains how the material has been turned into a usable cutting tool. A useful description identifies the tool material, surface treatment, drill construction, dimensions and application together. This gives a workshop enough information to select a replacement and gives a distributor a clearer basis for comparing apparently similar products.
Read Material, Process and Coating as Separate Descriptions
Drill listings often place several abbreviations beside each other. They answer different questions rather than representing a simple ladder from basic to best.
| Description | What It Usually Identifies | What Still Needs Checking |
|---|---|---|
| HSS | High-speed-steel material family | Exact grade and finished-tool design |
| HSS-Co or HSCo | Cobalt-bearing high-speed steel | Grade, cobalt designation and application |
| HSS-R | Common designation for a roll-formed drill | Geometry, finish and dimensional specification |
| HSS-G | Common designation for a ground drill | Which features are ground and the finished specification |
| TiN | Titanium nitride coating | Base material, geometry and suitable cutting conditions |
| DIN length-series reference | A specified drill form or dimensional series | Exact diameter, lengths, shank and applicable standard details |
These descriptions can coexist. A cobalt-bearing HSS drill can also have a coating. A ground drill can have different point designs. A dimensional standard does not turn every drill made to that series into the same material grade. Read each field separately before treating two catalogue entries as equivalent.
The suffixes are useful identification aids, but a short sales title may omit important details. For example, “ground HSS” says less than a drawing and a complete material description. Clarify the selected product instead of assuming that an abbreviation carries every property you need.
Distinguish HSS Grades From Surface Colour
Cobalt Is an Alloy Description
Cobalt-bearing HSS grades are part of the high-speed-steel family. M35 and M42 are examples of grade designations encountered in drill catalogues. Their names refer to the tool material; they do not mean that a cobalt-coloured layer has been painted onto an ordinary drill.
For selection purposes, the important question is whether the complete drill is suitable for the actual operation. A cobalt designation may be relevant to a demanding metal, but it does not remove the need for suitable geometry, stable holding and appropriate cutting data. Buying the most expensive material option while leaving those conditions unresolved can still produce disappointing holes.
For detailed product comparisons, use the individual M35 cobalt drill bit and M42 cobalt drill bit pages. Keep a general HSS definition separate from a specific grade-selection decision.
A Coating Describes the Surface
A coated drill has a base tool material underneath its surface layer. TiN is one example of a coating used on drills. This makes “HSS or titanium?” an incomplete comparison: a product described as titanium-coated may itself have an HSS substrate.
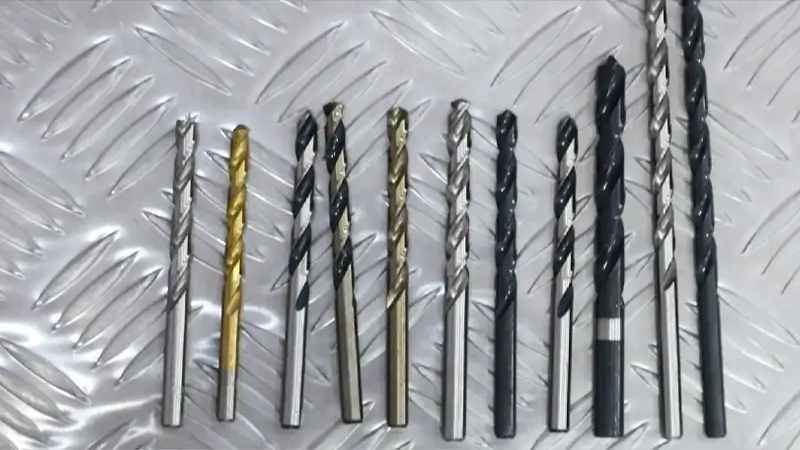
Gold, black and bright finishes are not reliable material tests. Lighting, wear and different surface treatments can produce similar appearances. Compare the written substrate and coating descriptions. If a listing only says “titanium drill,” establish whether it means a coating, a tool intended for drilling titanium, or something else before ordering.
Regrinding also makes the distinction practical. Sharpening changes the cutting faces and may remove coating from the reground area. It does not change a cobalt-bearing substrate into another steel grade. The reconditioned tool still needs correct geometry and an application-appropriate condition.
Understand Ground and Rolled HSS Drills
Ground and rolled descriptions relate to manufacture. They are not substitutes for an application test or a finished-tool specification. A process label cannot tell you the resulting hole size, straightness or tool life on its own.
When comparing offers, look beyond the appearance of the flute surface. Ask whether the diameter and length series match, whether the points have the same preparation and whether the tools are intended for the same material. A comparison between a short ground drill and a much longer rolled drill changes more than the manufacturing route.
The same caution applies to “fully ground.” Establish what is being described rather than assuming a guaranteed hole tolerance. Finished dimensions, edge condition and concentric running in the actual holder matter to the result. A damaged chuck or excessive projection can undermine a carefully made drill.
For a purchasing comparison, keep the process description alongside the material and geometry. This prevents a supplier quotation from being accepted simply because it repeats a familiar abbreviation. For a workshop comparison, run like-for-like tools on the same workpiece and judge useful holes, edge condition and repeatability, not surface shine.
Look at the Point, Flutes and Cutting Edges
Point Angle and Point Preparation Are Different
The point angle describes the included angle at the drill tip. A split point describes how the central region has been prepared. A stated point angle therefore does not prove that the drill has a split point.
This difference is important when a replacement has to reproduce reliable starting behaviour. A drill with an unsuitable or damaged point may wander before it establishes the hole. The solution is not automatically a change of steel grade. Inspect the point and the starting method as well as the workpiece surface.
Keep the required point description associated with the actual drill series. For a fuller explanation of the geometry, see the drill point angle guide.
Flutes Need Space for Chips
The flutes provide a route for chips to leave the cutting region. Their profile and helix are part of the drill design. The remaining central section contributes to the tool's strength. Changing these features affects more than the way the drill looks.
A flute packed with chips cannot continue doing its job normally. Heat, rubbing and irregular cutting can follow. Hole depth, material and coolant delivery all influence chip evacuation, so the same nominal diameter can behave differently in a shallow bracket and a deeper block.
The margins guide the drill along the hole. Worn or damaged guiding surfaces, unequal cutting edges and poor holding can affect the hole even when the material grade is correct. Examine the complete tool rather than judging it only from the sharpness of one visible lip.
Choose the Shortest Length That Reaches the Job
A longer drill provides access, but reach has a cost in support and rigidity. For a straightforward accessible hole, unnecessary projection makes the setup less stable. Choose the shortest suitable tool that reaches the hole and leaves the required working clearance.
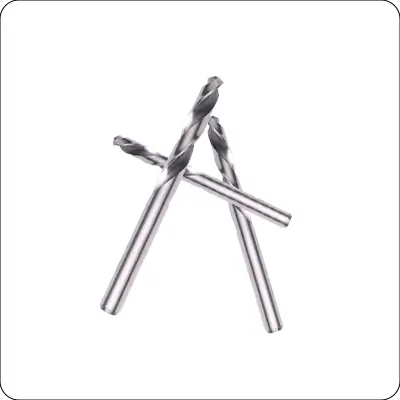
Overall length and flute length describe different dimensions. Overall length includes the shank; flute length describes the fluted portion. Neither should be used casually as the guaranteed drilling depth. The tool still needs room for chip movement and the holder must grip the correct section.
In a blind hole, the conical point also means that full-diameter depth and deepest point depth are different. A drawing that requires a full-diameter cylindrical hole must allow for the point shape. Ordering a drill by overall length alone does not resolve that requirement.
Length-series names such as stub, jobber and long help organize a range, but exact dimensions remain important. Compare the stated flute and overall lengths when replacing tooling across catalogues. An apparently similar long drill can change the available access or projection enough to affect the operation.
Match the Shank to the Holder and Machine
Straight shanks, reduced shanks, hexagonal shanks and Morse taper shanks have different holding arrangements. Their presence does not change the cutting diameter into a machine-capacity rating.
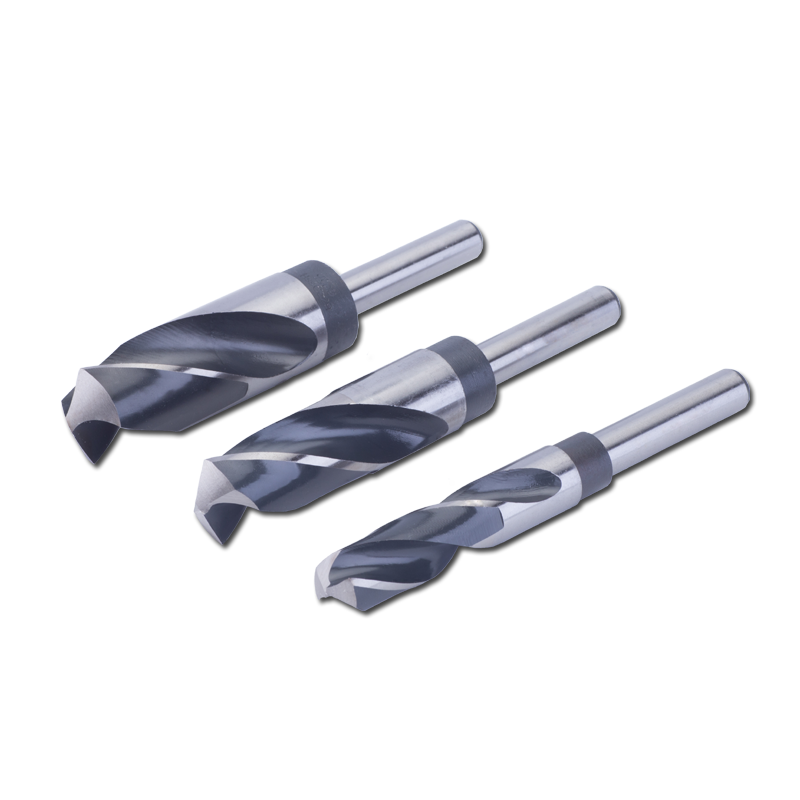
A reduced-shank drill may fit a smaller chuck, but that fit does not approve the larger hole for the machine. Torque, speed range, workholding and the machine's permitted drilling capacity remain separate considerations. Do not choose a large drill solely because its reduced end enters the chuck.
For a straight-shank tool, the chuck must grip the intended shank securely. For a taper-shank tool, identify the taper designation and compatible socket or approved sleeve. Do not improvise a mounting method from visual similarity. Excessive projection, damaged interfaces or contamination can produce poor running even with the correct nominal connection.
When buying for several machines, separate the cutting requirement from the interface requirement. The same workpiece diameter may need different shank arrangements across the workshop. A stock list organized only by diameter can hide those differences until the tool reaches the machine.
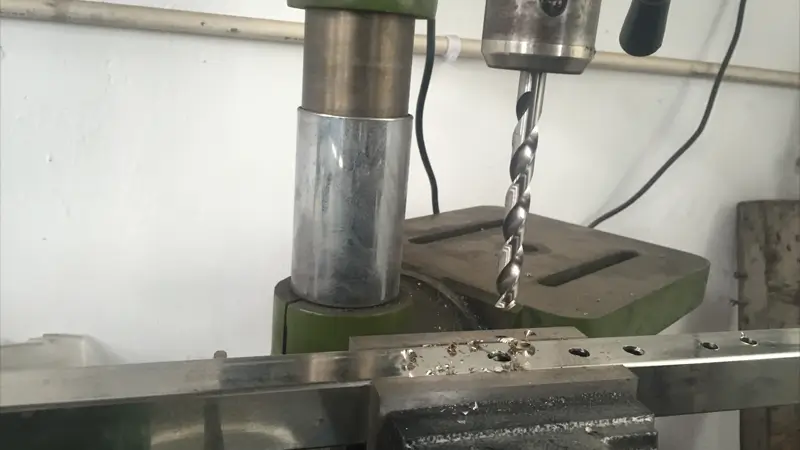
Select HSS Drill Bits for the Actual Material
Many HSS twist drills are intended for metalworking, but “metal” includes very different machining conditions. A mild-steel bracket, stainless tube and aluminium component do not necessarily need the same drill geometry or cutting approach. Identify the workpiece material and condition before selecting the tool series.
For stainless steel, use a drill designed for the specific material and maintain the recommended cutting conditions. Persistent rubbing is not a useful substitute for cutting. If progress stalls, investigate the point, settings, feed and chip removal rather than simply applying more pressure or buying a different coloured drill.
For thin sheet, breakthrough and grabbing deserve attention. A conventional twist drill is not automatically the best choice for every large sheet-metal hole. Depending on the required diameter and material, an appropriate step drill or another holemaking method may give better control. Keep that decision tied to the hole, not to the HSS label.
Some HSS metal drills can also drill suitable plastics or wood, but specialist geometries may give better entry, chip removal or finish. Check the chosen tool's application guidance. A drill that can make a hole is not necessarily the most efficient tool for repeat production.
A conventional HSS twist drill for metal is not the correct default for masonry or concrete. Those applications call for the appropriate masonry or concrete drilling tool and operating mode. Likewise, do not assume ordinary HSS is suitable for an unknown hardened component. Material condition can require a specialist drill and a substantially different setup.
Use Cutting Data Rather Than One Universal RPM
HSS is not a speed setting. Recommended cutting conditions depend on the drill series, diameter, material, hole depth, machine and lubrication. A speed that suits one diameter does not automatically suit another.
Use the selected tool manufacturer's cutting data as the starting point, then keep the setup within the machine's instructions. Feed must allow the edges to cut and the chips to leave. Neither prolonged rubbing nor excessive force corrects a blunt point or unsuitable tool.
Secure the workpiece and use the machine's required guarding. Never rely on handholding a metal component against drilling torque. Stop the machine before removing tangled chips or inspecting the point; suitable chip-removal tools avoid contact with sharp swarf.
A useful trial records the material, tool, holder and operating conditions together. If performance changes, this gives you a way to distinguish a tool change from a setup change. It also makes a successful replacement easier to repeat without turning one workshop result into a universal promise.
Diagnose the Problem Before Replacing the Grade
| What You Observe | What to Investigate First | What Not to Assume |
|---|---|---|
| Drill wanders at entry | Point condition, starting method, surface and rigidity | Every starting problem needs cobalt |
| Hole runs large or uneven | Holder condition, runout, projection and edge symmetry | Nominal drill size guarantees hole tolerance |
| Chips pack in the flutes | Hole depth, chip evacuation and cutting conditions | A harder material grade clears chips automatically |
| Rapid edge wear | Workpiece condition, suitable tool series and cutting data | A gold finish proves a better substrate |
| Tool slips or runs visibly off-centre | Shank, chuck, seating and damage | A tighter grip cures an incorrect interface |
These checks help avoid changing several variables at once. If a new grade, length and point are introduced together, any improvement is difficult to attribute. Compare one controlled change where practical. Stop using a damaged tool; diagnosis should not become a reason to continue drilling with a chipped edge or unstable holder.
Separate Drill Diameter From the Finished Hole Requirement
The diameter marked on a drill identifies the tool, not a guaranteed tolerance in every setup. A drawing may require a hole that must later be reamed, tapped or otherwise finished. Start with the finished feature and its purpose, then decide what the drilling operation needs to leave for the following process.
This is especially helpful when a purchaser receives a complaint that a drill is “the wrong size.” Check whether the customer ordered the correct nominal tool, whether the hole was measured consistently, and whether the machine and holder were suitable. Changing the ordered drill diameter before understanding the cause can hide a setup problem rather than solve it.
For a blind hole, state whether the required depth is measured to the tip or to the full-diameter cylindrical portion. For a through hole, include breakthrough clearance and the material underneath. These details help separate a dimensional misunderstanding from an actual tool-selection issue.
Build a Useful HSS Drill Specification
A concise specification can still be complete. Include the material designation, coating or surface condition, diameter, flute length, overall length, shank and point. Add the workpiece, required depth and machine when asking for a recommendation.
For example, “HSS drill for metal” leaves the user to make almost every important decision. A description that identifies the steel grade, exact drill dimensions, point and holder type is much easier to compare. If a hole needs later reaming or a particular finish, include that requirement rather than expecting the drill's material name to communicate it.
Distributors should keep comparable tools under clear series descriptions. Separating base material from finish helps customers recognize a genuine alternative without confusing appearance with alloy. It also reduces mistaken substitutions between different lengths or shanks sold under the same broad diameter heading.
For a bulk reorder, send a line-by-line size and quantity list rather than a photograph of a partly used set. Identify which dimensions must remain unchanged and whether the drill is sold individually or in a set. Ask for the proposed material, point and finish against each requested series. Review substitutions before accepting a lower unit price: a change of reach or shank can make an apparently equivalent drill unusable for the customer's machine.
Keep an approved sample or drawing linked to the order description. A photograph can show the supplied shape and marking; it cannot establish the steel chemistry or a coating's composition. Agree how any required material or dimensional conformity will be documented. This turns the general term HSS into a repeatable purchase without treating every order as a new selection exercise.
Frequently Asked Questions
What Does HSS Stand for on a Drill Bit?
HSS stands for high-speed steel. It describes a family of cutting-tool steels rather than one drill shape or exact alloy grade. To select a finished drill, also check its material designation, surface treatment, point, diameter, lengths and shank. The acronym is useful for identifying the tool family, but it is not a complete replacement specification.
Is a Cobalt Drill Bit Also an HSS Drill Bit?
Cobalt-bearing high-speed-steel drills belong to the HSS family. A description such as HSS-Co indicates an alloy distinction, while M35 or M42 identifies a grade. It does not mean the drill has a cobalt coating. Choose the complete tool for the workpiece and machine; cobalt content alone does not establish suitable geometry or operating conditions.
Are Gold-Coloured HSS Drill Bits Always Titanium-Coated?
Do not identify the coating or material from colour alone. A gold-looking surface is not a reliable specification, and a coated drill still has an underlying substrate. Read the actual coating and base-material descriptions. This is particularly important when comparing replacements, because two visually similar drills can differ in material, point, length and intended use.
Can an HSS Drill Bit Drill Masonry?
A conventional HSS twist drill intended for metal should not be selected as a masonry or concrete drill. Use the tool type and operating mode specified for the substrate and machine. A multi-material drill with an appropriate tip is a different design; its suitability cannot be transferred to an ordinary HSS metal drill because both fit the same chuck.
What Is the Difference Between SDS and HSS Drill Bits?
SDS describes a shank-and-holder interface; HSS describes the cutting material. They are not competing grades of steel. An ordinary straight-shank HSS metal drill is not a direct replacement for an SDS hammer bit. Match the connection, intended workpiece and operating mode. Adding an adapter alone does not make a metal drill suitable for hammer drilling.
Can HSS Drill Bits Be Resharpened?
Many HSS twist drills can be resharpened when their size, condition and design permit it. The point must be restored correctly, including any required thinning or split-point preparation. Regrinding can remove coating from the sharpened area. A heavily damaged or excessively shortened drill may no longer be an economical or suitable candidate for reuse.
Conclusion
HSS tells you what family the cutting material belongs to. Reliable selection comes from matching that material with the correct point, flute design, length and holding arrangement for the real workpiece. Keep grades, manufacturing descriptions and coatings separate, and investigate the setup before blaming the alloy for every drilling problem.
Send AXIMET your workpiece material, machine, diameter, required depth and current drill specification to discuss a suitable option from the HSS and cobalt drill range.