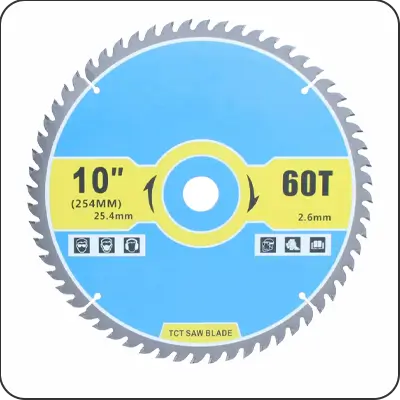
Choose a plywood saw blade for the panel, saw and finished edge. Tooth count matters, but tooth geometry, sharpness, kerf, face support and machine alignment also affect the result. A cleaner cut starts with matching those conditions rather than buying the blade with the most teeth.
Start With the Panel and the Finished Part
Plywood consists of bonded layers, usually with the grain direction changing between adjacent veneers. A cut that runs with the grain of the outer face still crosses other layers. This is why a solid-wood ripping recommendation does not automatically describe the best blade for plywood, even when the sheet is being cut lengthwise.
Identify the panel thickness, outer veneer and surface finish. Thin decorative faces, construction plywood and film-faced panels do not present identical finish requirements. A hidden structural edge may only need to be straight and usable; an exposed furniture edge may require very little face damage before edging or finishing.
Also identify the finished part rather than judging the whole sheet. If only one face will be visible, its orientation can be planned around the saw's cutting action. If both faces remain exposed, the cutting system needs to control breakout on both sides. This may involve a suitable blade and compatible splinter-control accessories.
Check whether the requested operation is rough sheet breakdown, accurate sizing, trimming or repeated production cutting. A fast first cut that leaves allowance for a finishing operation is different from a final cut to size. Specify the required result before deciding how much finish performance belongs in the blade itself.
What Makes a Circular Saw Blade Suitable for Plywood?
Tooth Count and Chip Clearance
Within a comparable blade diameter and design, more teeth are often associated with finer cutting, while fewer teeth provide more space for chips. That relationship is useful, but it is not a universal ranking of quality. Feed, thickness and tooth geometry still determine how the blade works in the actual panel.
Tooth count must be read with diameter. A 60-tooth compact-saw blade does not have the same tooth spacing as a much larger 60-tooth blade. Consequently, a recommendation copied from a table saw should not be transferred unchanged to a smaller portable saw. Select from the blade maker's plywood or panel range for the relevant machine.
Circular blades normally list a total tooth count, often marked Z. This is different from the teeth-per-inch descriptions used for many straight and band saw blades. Mixing those two measurements can make a replacement request unintelligible even when the number itself is correct.
Tooth Geometry and Hook Angle
Alternate top bevel, or ATB, describes teeth with alternating bevel directions. Panel and plywood ranges commonly use ATB or high-ATB designs to address face-veneer cutting. Other geometries, including triple-chip arrangements, serve particular materials or coated-panel applications. The shape must be considered with the intended material, not chosen from an attractive close-up alone.
Hook angle affects how the tooth approaches the work. A blade suited to one saw's feed arrangement is not automatically appropriate on a sliding mitre saw or another machine. Treat the permitted machine and application as part of the design, not as an optional note added after diameter and tooth count.
Match Diameter, Bore, Kerf and Plate Thickness
The outside diameter must fall within the saw's specified blade requirement. Do not install a larger blade to increase capacity or assume a smaller one is acceptable merely because it clears the guard. Cutting depth, guarding and the machine's intended geometry belong together.
Match the bore and any other mounting features to the approved spindle arrangement. Use only the reducing rings or adapters permitted for that blade and saw. An improvised sleeve or modified centre hole can compromise mounting; a fitting bore does not prove that every other dimension is suitable.
Kerf is the width removed by the teeth. Plate thickness is the thickness of the blade body. These are different dimensions, often shown as B and b respectively in blade drawings, although the drawing convention should always be checked. A thin-kerf replacement may change cutting resistance and waste, but it must still satisfy the saw's mounting and safety requirements.
On a saw with a riving knife, the knife, blade body and cutting width must have the relationship specified by the machine manufacturer. A very narrow kerf is not automatically compatible with the existing knife. Do not remove a required safety component to make an unsuitable blade fit.
Check direction markings and rated operating speed as well. The blade must be approved for the machine's speed and use. A familiar diameter or a label saying “wood” does not authorize every circular blade for every saw.
Select by Saw Type, Not Only by Blade Diameter
| Saw Arrangement | Main Selection Questions | Finish Considerations |
|---|---|---|
| Handheld circular saw | Approved diameter, bore, blade type and guarding | Support the sheet; plan the visible face around tooth travel |
| Track or plunge saw | Blade and rail-system compatibility, kerf and specified machine use | Check the rail strip and any offcut-side splinter guard |
| Table saw | Machine-rated blade, riving knife relationship and suitable feed setup | Support the panel and protect the exit-side veneer appropriately |
| Sliding or vertical panel saw | Main blade specification, feed system and any scoring arrangement | Main and scoring tools must work as the intended system |
| Mitre saw cutting narrow plywood parts | Blade specifically suitable for that saw and workpiece size | Clamp and support within the machine's permitted capacity |
A mitre saw is not a substitute for a sheet-cutting setup simply because it accepts a circular blade. Similarly, a table saw with a suitable blade still needs enough support and a workable method for managing a large panel. Machine selection and blade selection should solve the same job.
Allow for the Kerf When Sizing Parts
Mark which side of the line belongs to the finished part. The blade removes a strip of material, so placing the centre of the teeth on a finished dimension can leave the part undersize. Align the correct cutting edge to the waste side using the saw's intended guide or indicator, then verify it with a sample.
A replacement blade with another kerf can change that relationship even when its diameter and bore match. Recheck the guide reference and any compatible splinter strip after changing blades. For repeated parts, use the approved stop or measuring system rather than assuming that a previously established reference remains exact.
Bevel cuts add a further question: which face carries the required finished dimension? Establish that before setting the guide. A correctly sized long face can coexist with the wrong short-face dimension if the drawing and cutting reference are being read differently.
Put the Finished Face on the Correct Side
Veneer breakout is strongly affected by where the teeth leave the material. Fibres are generally better supported where teeth enter a face than where they emerge from it. This explains the familiar difference between conventional handheld circular-saw and table-saw face-orientation advice.
With a conventional handheld circular saw used normally above the sheet, the teeth emerge through the upper face, so the preferred face is commonly placed down. On a conventional table-saw through-cut, the teeth enter the upper face, so the preferred face is commonly up. Follow the actual saw instructions and verify the arrangement on an offcut.
A track saw can change the result on the upper surface because the guide rail's splinter strip supports the cut edge. A compatible guard on the other side can address the offcut edge as well. These features are specific to the system and its condition; a worn strip or a blade change can affect its relationship to the cut line.
Do not transfer the face rule blindly to a different machine, reverse-feed arrangement or unusual accessory. Nor should the desired finish be pursued by feeding against the permitted direction. Work within the saw's intended method, and use a representative trial to confirm which face needs additional protection.
Support the Sheet Without Trapping the Blade
Good support keeps the panel stable throughout the cut, including the moment the offcut separates. A sagging sheet can change the cut, damage the face veneer or close around the blade. Plan supports before starting and consider both the finished part and the waste piece.
Support should not force the cut to close or trap the offcut between a blade and an unsuitable stop. On a table saw, use the appropriate fence, mitre guide or crosscut system for the operation rather than combining references in a way that captures the waste. Follow the machine manual for large-sheet handling and outfeed arrangements.
For handheld work, use a stable support layout that leaves the intended blade path clear. Keep the machine base supported through the cut and arrange clamps outside the travel of the saw and guard. A second person should not pull the offcut away during cutting or steer the panel from a hazardous position.
Backer material and close-fitting support can help reduce breakout in suitable setups, but they are not universal accessories. Check their compatibility with the operation, guards and workholding. They cannot make a damaged blade, poor alignment or an unsafe feed arrangement acceptable.
Use Scoring and Splinter Control Appropriately
A scoring unit on a panel saw makes a preliminary cut intended to protect the face that would otherwise suffer breakout. Its width and position must be matched to the main blade and machine setup. A misaligned scorer can leave a visible step rather than improve the edge.
Some plunge-saw systems provide a defined scoring function or an approved method for a shallow preliminary cut. Follow that system's instructions. Do not improvise a backwards cutting pass or defeat a guard to reproduce a technique seen on a different saw.
Tape along a cut line is sometimes used to support delicate surface fibres or preserve a mark. It is not a replacement for a sharp blade and proper backing. Test adhesion on the actual finish because removing tape can damage a vulnerable surface. A short test is preferable to discovering that the protective measure lifted the veneer.
When both faces are visible, evaluate both after the trial. A clean top edge does not prove that the underside is acceptable. Identify whether the visible problem is at the entry face, exit face or end of the cut before changing the blade specification.
Tell Tear-Out, Burning and Core Defects Apart
| Observation | What It Describes | First Checks |
|---|---|---|
| Chips or torn fibres along a face | Veneer tear-out | Tooth condition, geometry, exit-face support and orientation |
| Brown or scorched cut edge | Burning or heat discoloration | Edge condition, deposits, alignment and feed |
| Damage mainly at the end of the cut | Exit or offcut breakout | Support, control and the final separation |
| Gaps inside the exposed edge | Possible core voids or internal panel defects | Panel construction and a fresh comparison sample |
| A cut that wanders or marks unevenly | Guidance, support or blade-condition problem | Machine setup, blade mounting and workpiece stability |
Different symptoms can appear together. More teeth do not identify the cause of burning, and a smoother face does not repair a void within the panel. Inspect the actual defect before changing specifications. For a broader heat-related diagnosis, use the circular saw burning guide.
Stop if there is abnormal vibration, binding, unusual noise or visible blade damage. Disconnect the power before inspecting the teeth, mounting surfaces or accessories. Do not continue cutting to “wear in” a suspect blade. Damaged carbide tips, cracks and distorted plates need appropriate professional assessment or replacement.
Feed, Cleanliness and Blade Condition Matter
Use a controlled, steady feed that suits the saw, panel and blade. Forcing an overloaded cut and dwelling unnecessarily in one place are both poor substitutes for selecting the right setup. When cutting feels markedly different from the sample, stop and investigate rather than compensating with greater force.
Adhesive and other deposits can obscure the tooth edges or create additional rubbing. Inspect a disconnected blade and clean it using a product and method permitted by its manufacturer. Aggressive scraping or an unsuitable chemical can damage the blade. Cleanliness should not be confused with sharpness: a clean but worn edge may still need servicing.
Sharpening changes more than how bright the tooth looks. The grind and relationships between teeth must remain appropriate, and the blade must remain within serviceable limits. Use a competent sharpening service for a suitable blade, and compare its cut after maintenance before returning it to finish-critical work.
Blade condition also affects comparison tests. Comparing a new candidate with a heavily worn existing blade may demonstrate the value of a fresh edge without proving that the new tooth geometry is better. Where practical, compare tools in comparable condition and keep the machine setup unchanged.
Run a Useful Plywood Cutting Trial
Use representative panels, including the actual face finish and thickness. Mark the intended finished face and cut direction. Make straight cuts with the approved guides, guards and support, then examine both faces and the exposed edge. Keep the result before sanding so the cutting performance remains visible.
Assess whether the cut meets the next operation. An edge going under edging tape may have different acceptance needs from a polished exposed edge or a close joint. Look for straightness, face breakout and local damage, not simply whether the operator considers the cut “smooth.” Avoid judging every blade against an undefined promise of a perfectly chip-free result.
Change one relevant variable at a time where practical. If the blade, panel, support and feed all change together, the reason for improvement becomes unclear. Keep one accepted example or a clear photograph of both faces so replacement blades can be assessed against the same finish requirement.
Compare the number of parts that meet the required size and finish, not simply the number of completed cuts. A blade that requires extra trimming changes both usable panel yield and labour. Assess those effects with the same cutting plan and acceptance criteria; a narrower kerf or a higher tooth count does not establish a saving by itself.
A useful result for a distributor is a repeatable application description: which saw, panel and cutting task a blade suits. That is more valuable than advertising a single tooth count as suitable for all plywood. It also helps separate a rough-cutting assortment from blades intended for final sizing.
Specify a Replacement Without Losing Important Details
For replacement, provide the saw model and the markings from the current blade, together with outside diameter, bore, kerf, plate thickness and tooth count. Add tooth form where known. Include the panel type, thickness, cut direction and the face or faces that must remain clean.
When troubleshooting, photograph the cut before sanding and show both faces. Include a close-up of the defect and an overall view that shows its location. A picture of a loose blade alone cannot explain support, guidance or where the damaged veneer occurs.
Compare suitable product families in the TCT circular saw blade collection. Keep the plywood application separate from blades selected for aluminium, masonry or other materials; a similar-looking carbide tip does not make those products interchangeable.
Frequently Asked Questions
What Is the Best Circular Saw Blade for Plywood?
Choose a blade intended for plywood or panel cutting and approved for the actual saw. Compare tooth geometry and count with diameter, kerf and the finish requirement. A blade for rough sheet breakdown need not be the best choice for an exposed furniture edge. Support and splinter control must also suit the machine and panel.
Are More Teeth Always Better for Cutting Plywood?
No. A higher count can support finer cutting within a comparable design, but it does not correct dull teeth, poor support or unsuitable feed. A 60- or 80-tooth label is not a universal plywood specification. Compare count alongside diameter, geometry and machine approval: the same count on different diameters does not describe equivalent spacing or cutting conditions.
Should Plywood Be Cut With the Good Face Up or Down?
That depends on tooth travel and the saw system. Conventional handheld circular saws commonly favour the good face down; conventional table-saw through-cuts commonly favour it up. Track-saw splinter strips and scoring systems can change the available protection. Follow the actual machine instructions and check both faces of a representative sample before cutting finished parts.
Why Does Plywood Burn Even With a Fine-Tooth Blade?
Burning can involve edge condition, deposits, rubbing, alignment or an unsuitable feed, rather than a lack of teeth. A fine-tooth label does not diagnose the cause. Inspect the disconnected blade and machine setup, and distinguish scorched edges from torn veneer. Persistent heat-related problems need diagnosis before another blade is chosen solely by tooth count.
Can a Thin-Kerf Blade Replace Any Standard-Kerf Blade?
No. The replacement still needs the correct diameter, bore, machine approval and operating limits. On machines with a riving knife, cutting width and plate thickness must satisfy the specified relationship to that knife. Do not remove required protection or improvise mounting changes to accommodate an unsuitable thin-kerf blade, even if reducing waste is desirable.
Can Backing or Tape Guarantee a Chip-Free Plywood Cut?
Neither provides a universal guarantee. Suitable backing can support vulnerable fibres, and tape may help in particular situations, but blade condition, tooth geometry, workholding and the panel itself still matter. Test the method on the actual face finish and inspect the underside as well. Avoid a protection method that interferes with guarding or safe feeding.
Conclusion
The right saw blade for cutting plywood matches the panel, saw and finished part. Read tooth count together with diameter, geometry, kerf and mounting requirements. Plan face orientation and support, then separate veneer breakout from burning or internal panel defects.
An effective trial checks both faces and the edge before sanding. Keep that finish requirement with the replacement specification so the next blade is selected for the same job, rather than for a larger tooth-count number alone.