
What Are Carbide Burrs Used For in industrial production? They remove local stock, clean edges and correct contours where larger tools cannot reach. The harder decision is matching the burr to the material, feature and drive. Use this guide to specify samples, ranges and customer instructions.
What Is a Carbide Burr?
A carbide burr is a rotary cutting tool with formed teeth on a tungsten-carbide head. Many industrial models use a carbide head joined to a steel shank; small designs may be solid carbide. Unlike a bonded abrasive, the teeth produce chips as the head moves across the workpiece.
The term 'burr bit' can be misleading. The tool is not a twist drill and it is not intended to create a tolerance-controlled hole by axial feed. Its value is controlled, localized removal on edges, welds, cast surfaces, slots, radii and hard-to-reach transitions. Product approval must still follow the supplier's material, speed, drive and contact guidance.
Buyer Definition: Specify a carbide burr by head shape, head diameter, cutting length, tooth geometry, shank diameter, total length and intended material. The word 'burr' alone is not a quotation-ready specification.
Which Jobs Do Carbide Burrs Perform?
Industrial burr work usually falls into six operations. The application decides the contact area and head profile; the material and finish target then narrow the cut. Treat the table as a sourcing map, not a substitute for a model-specific trial.
Broad surface finishing is different. A burr can establish geometry or remove a local high spot, but a flap wheel, mounted point or another abrasive may be better for the final blend. A drill, reamer, end mill or countersink is also preferable when the result is defined by hole size, positional accuracy or a fixed machine path.
| Operation | Typical Work | Specification Priority |
|---|---|---|
| Edge Deburring | Remove machining burrs, sharp edges and flash | Access, edge condition and allowed chamfer |
| Weld Correction | Reduce excess bead and clean local weld transitions | Parent material, bead position and stop boundary |
| Casting Cleanup | Remove gates, riser remnants, fins and local scale | Casting alloy, interruption and removal volume |
| Contour Shaping | Blend cavities, radii, ports and irregular profiles | Shape match, visibility and reach |
| Hole and Slot Work | Open, blend or deburr an existing feature | Entry angle, hidden edges and diameter allowance |
| Tool and Die Repair | Correct localized damage without disturbing adjacent geometry | Control, finish target and inspection method |
Industrial Applications by Sector
The same burr shape can behave differently across industries because the workpiece, access and acceptance criteria change. Ask where the tool enters the process before choosing a catalog range.
Industry labels do not approve a tool. Aerospace work, for example, may involve aluminum, titanium, stainless steel or nickel alloys, each with different chip, heat and documentation needs. Your RFQ should identify the actual grade, condition, feature and removal target rather than only naming the sector.
- Metal fabrication and welding: edge cleanup, weld dressing, hole correction and preparation before abrasive blending.
- Foundries and forging shops: removal of flash, fins, gate remnants and local casting defects.
- Automotive and transport: casting cleanup, port and manifold work, fixture repair and component rework.
- Aerospace and energy: localized deburring where traceability, runout and process limits matter.
- Tool, die and mold shops: cavity correction, radius work and repair in restricted areas.
- Maintenance, shipyard and heavy equipment: weld repair preparation and access-limited field correction.
Carbide Burrs vs Other Deburring Tools
A distributor should not promise that one tool replaces the rest. The best process may use a burr for stock removal, a blade for an accessible residual edge and an abrasive for the final surface. Describe the handoff between operations so customers evaluate each item on the correct result.
| Tool | Strongest Fit | Main Limitation |
|---|---|---|
| Carbide Burr | Localized stock removal, shaping and complex access | Requires matched cut, speed, holder and operator path |
| Hand Deburring Blade | Reachable straight or curved edges with light burrs | Limited removal rate and poor access to some internal features |
| Mounted Point | Grinding, blending and surface refinement | Abrasive wear changes the profile during use |
| Flap Wheel | Broad blending after geometry is established | Less suited to narrow slots and precise local correction |
| Countersink | Repeatable chamfer around an accessible round hole | Does not follow irregular edges or free-form contours |
| End Mill | Programmed geometry and dimensional control | Needs a rigid machine, holder and defined toolpath |
Carbide Burr Cut Types
Tooth geometry controls chip size, cutting action, guidance and the resulting surface. Names vary by producer, so a generic label must be tied to a drawing, sample or supplier code before private-label artwork is approved.
Single cut can provide an aggressive, directional cutting action and longer chips. Double or cross cut divides the teeth, usually producing smaller chips and easier hand control. That does not make double cut automatically faster or smoother on every material. Compare matched head sizes on the customer's workpiece and record removal, finish, chatter and tool condition.
Open-flute aluminum designs are a separate decision. They create more chip space for soft non-ferrous alloys. Using a dense cut on a loading-prone alloy can fill the flutes, increase rubbing and push operators toward excess pressure.
| Cut Family | Typical Decision | Buyer Check |
|---|---|---|
| Single Cut | Longer chips and direct cutting action for selected stock-removal work | Material, feed direction, finish and operator control |
| Double or Cross Cut | Shorter chips and easier hand control on many ferrous applications | Removal target, surface requirement and exact tooth geometry |
| Aluminum Cut | Open flute space for soft, long-chipping non-ferrous materials | Alloy, loading tendency and anti-stick guidance |
| Fine or Specialist Cut | Higher finish, hard materials or a defined automated process | Material hardness, cycle target and manufacturer data |
How to Choose a Carbide Burr
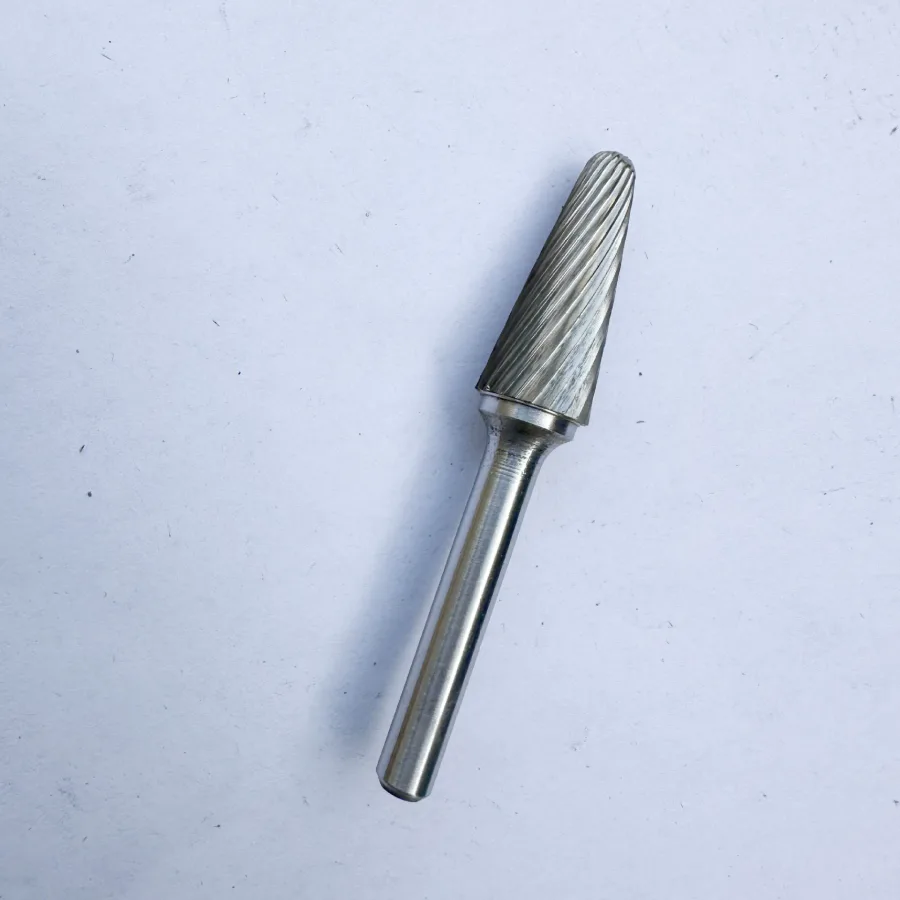
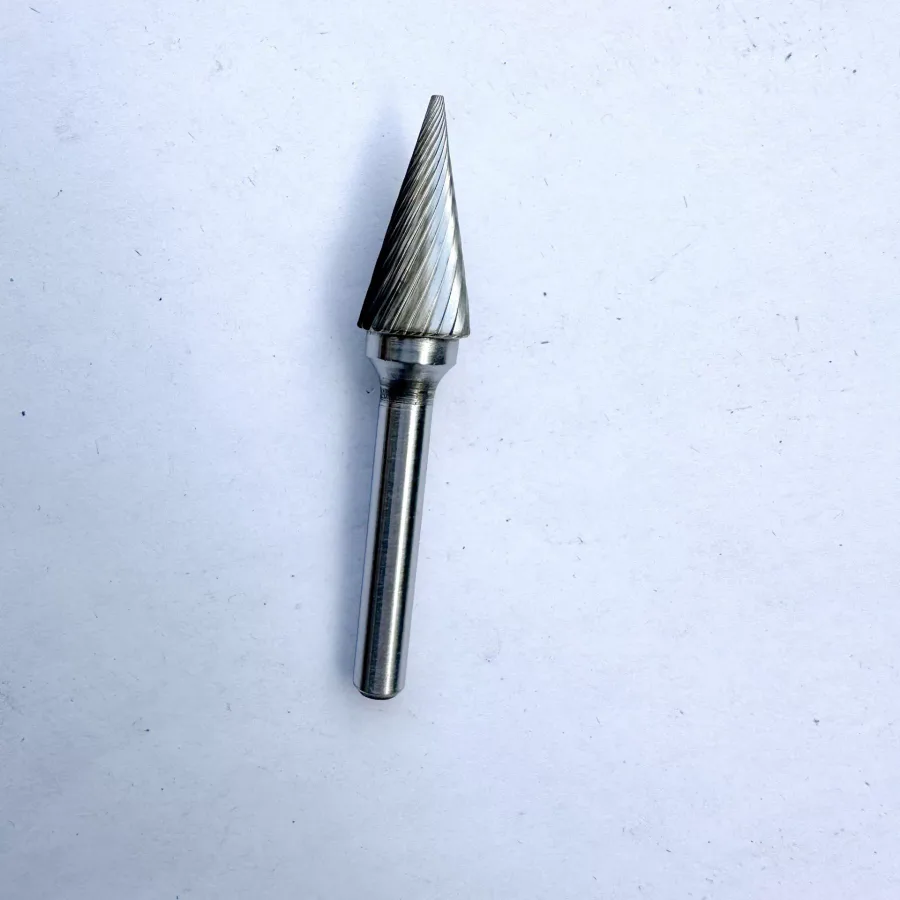
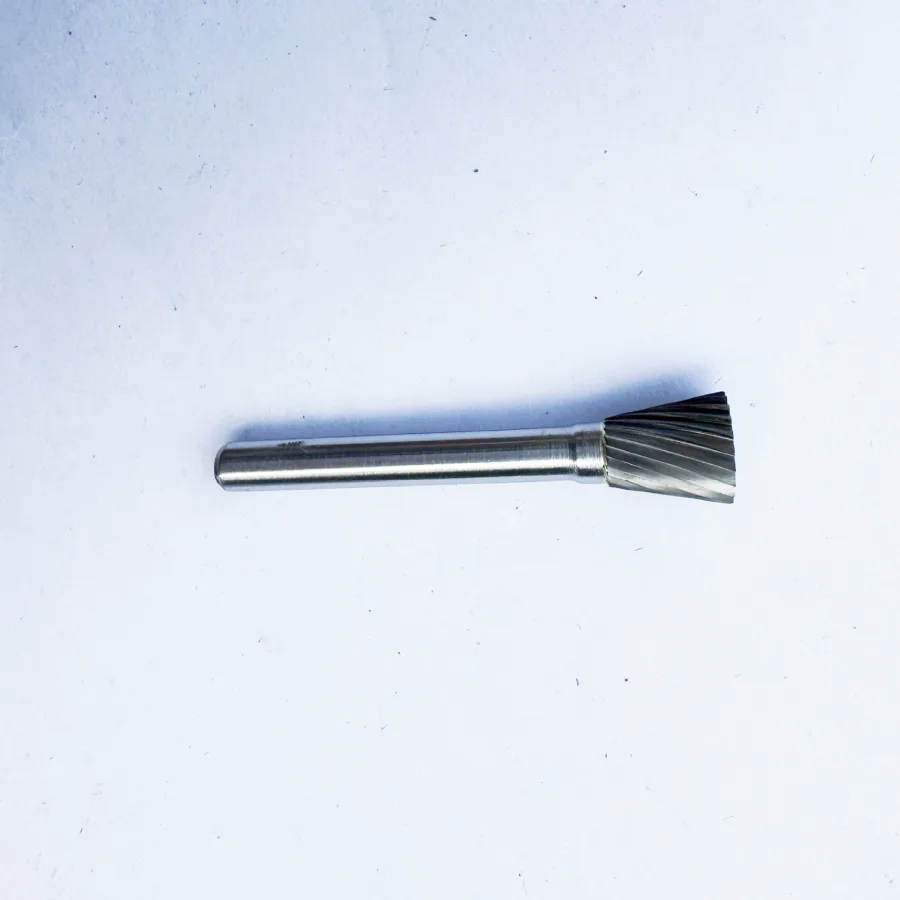
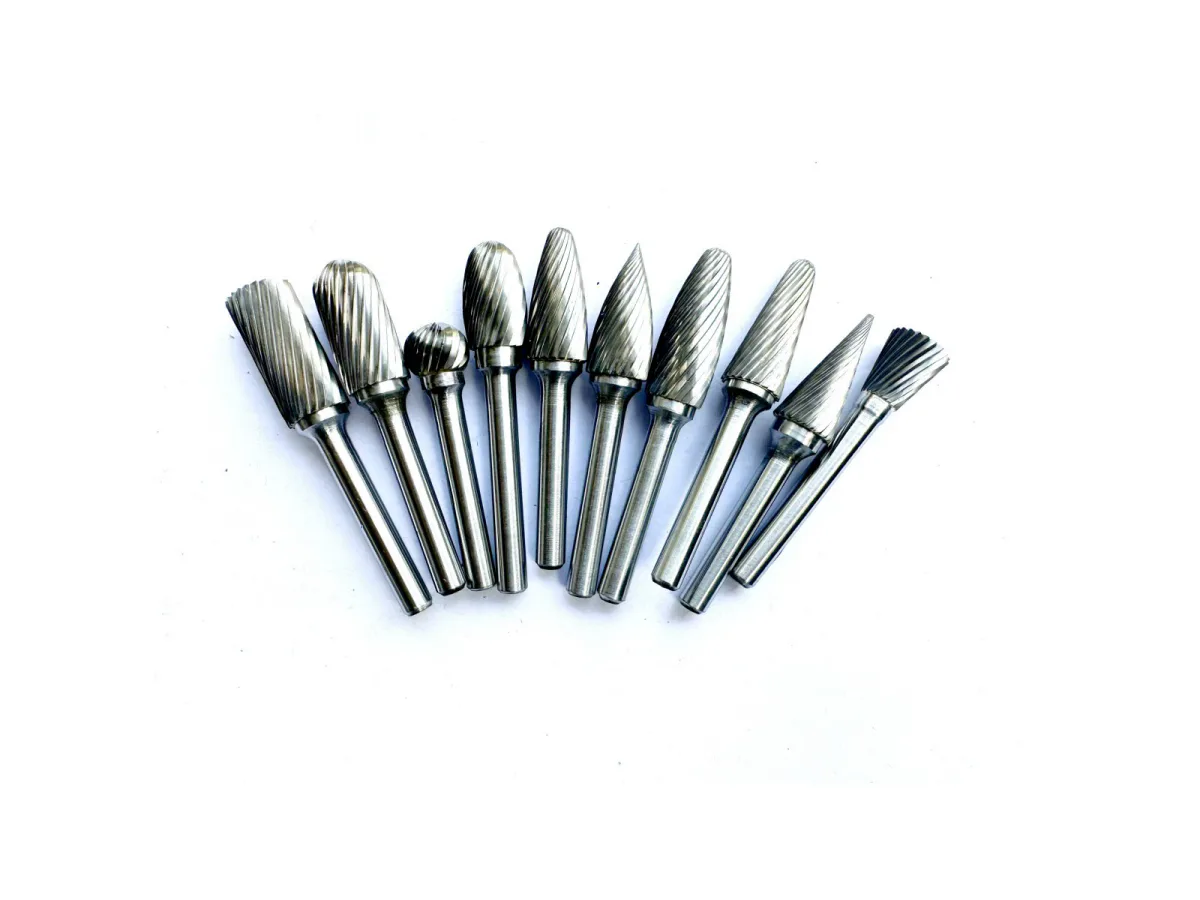
Start with the part, not the catalog. The correct selection preserves the surface that must remain and reaches the material that must be removed. These Types of Carbide Burrs are commonly organized by head profile, but the same profile may be offered in several cuts and dimensions.
| Feature | Useful Shape Family | Selection Risk |
|---|---|---|
| Flat Surface or Straight Edge | Cylinder or end-cut cylinder | An end cut must be specified when face cutting is required |
| Internal Radius or Concave Surface | Ball, oval, radius cylinder or radius tree | A head that is too large bridges the contour |
| Narrow Contour or V-Groove | Pointed tree, flame or tapered profile | Thin tips are not intended for heavy leverage |
| Chamfer or Countersink Cleanup | Cone, tapered or angle-specific profile | Included angle and access must match the feature |
| Reverse-Side Edge | Inverted cone or dedicated back-deburring solution | Poor visibility increases the risk of overcutting |
| Cross-Hole Deburring | Ball, oval or process-specific guided tool | Contact path must protect the bore and opposite wall |
- Choose the cut from workpiece material, chip behavior, removal target and finish.
- Choose the head diameter from access, contact area and the radius that must remain.
- Choose cutting length and total reach without adding unnecessary overhang.
- Match 3 mm, 6 mm, 1/8-inch or 1/4-inch shanks to an exact collet; nearby metric and inch sizes are not interchangeable.
- Confirm the drive can reach and hold the supplier's permitted speed for the selected head.
- Approve the range on representative parts before expanding the claim to other materials or shapes.
Best Carbide Burr for Weld Removal
There is no universal best model. A cylinder or radius-end cylinder works on accessible bead and flat transitions. A ball, oval, tree or flame profile may reach fillets and curved joints. The cut must match the parent metal and required finish, while the head size must stay inside the approved removal boundary.
For purchasing tests, mark the allowable profile before cutting. Record the burr code, drive, speed, time, material removed, surface condition and any heat discoloration. If a wide blended appearance is required, stop the burr at the geometry stage and use an appropriate abrasive for the finishing stage.
Drive Systems for Manual and Automated Deburring
Pneumatic and electric die grinders are common for manual work because they accept defined collets and operate in the speed class used by many burrs. Flexible-shaft drives can improve access. The exact machine must still provide sufficient power, low runout and the permitted speed range.
Robotic cells, automated centers and machine tools can use selected burrs when the process is engineered around a rigid holder, controlled path, workpiece variation and tool-wear limits. Do not transfer a hand-use SKU into CNC or robotic duty from physical fit alone. Long-shank designs may carry specific restrictions and lower speed limits.
Automation Boundary: Approve the exact burr, holder, spindle, toolpath and part family together. A catalog statement that lists robots or machine tools does not qualify every shape, shank length or operating condition.
How to Use a Carbide Burr
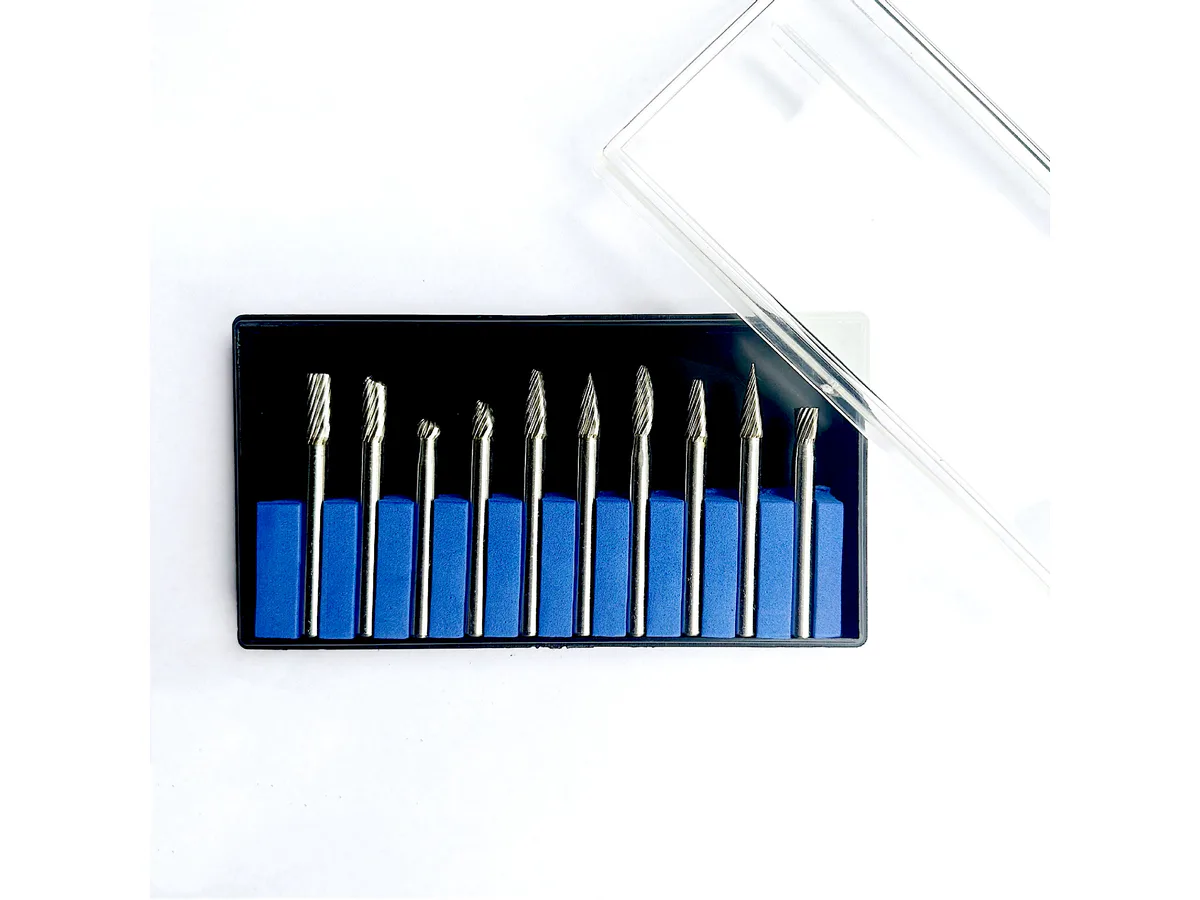
Follow the burr and drive manufacturers' instructions first. The operating sequence below is a qualification framework for industrial buyers, not a universal speed recipe.
- Secure the workpiece and inspect the burr for chipped teeth, a bent shank, a damaged joint or contamination.
- Clean the collet and shank, insert the shank to the specified depth and minimize unsupported length.
- Set the speed from the supplier's chart for the exact head diameter, cut, material and shank configuration.
- Bring the tool to stable speed, use controlled contact and keep the head moving across the intended surface.
- Use enough pressure to cut without pulling the drive speed down; rubbing and stalling are process warnings.
- Stop if vibration, slipping, abnormal noise, heat or surface damage appears, then correct the system before restarting.
Loading, Cleaning, Sharpening and Tool Life
How to Prevent Carbide Burr Clogging: Match an open cut to aluminum and other loading-prone materials. Maintain effective cutting speed, avoid force that slows the drive and keep the teeth moving through fresh material. Use only permitted anti-stick compound or lubricant.
How to Clean Carbide Burrs: Isolate the drive and remove the tool. Use an approved brush and compatible cleaner. Do not strike the teeth, attack the joint with aggressive chemicals or reinstall the burr while solvent remains on the shank.
How to Sharpen Carbide Burrs: Do not present field sharpening as routine maintenance. Complex flute geometry requires specialist equipment. Separate, inspect and replace a chipped or badly worn tool unless its producer approves qualified regrinding.
How Long Do Carbide Burrs Last: There is no honest fixed-hour answer. Measure pieces or removal volume under a defined test and replace the tool when cycle time, finish or vibration crosses the approved limit.
Carbide Burr Safety
A rotating burr can eject chips and can fail if it is damaged, badly held or run outside its limit. Your work instruction must follow the tool, drive and site risk assessment. It should define eye, hearing, respiratory and hand protection; workpiece restraint; guarding; inspection; maximum speed; shutdown and disposal.
- Never exceed the lowest maximum-speed rating in the approved tool, holder and drive system.
- Keep the workpiece away from the shank and brazed joint; cut only with the designed tooth area.
- Remove burrs that are dropped, bent, cracked, chipped, loose at the joint or visibly out of balance.
- Reduce speed and follow start-contact rules where specified for extended shanks.
- Control chips and dust according to the material, coating and site exposure assessment.
- Do not use a hand-guided process where geometry or risk controls demand fixtured machining.
How Buyers Should Qualify a Carbide Burr Range
A sample should answer a commercial question. Test the configurations that cover the largest share of customer work instead of collecting one of every shape. Keep the same product code on the drawing, sample label, test record, carton artwork and repeat-order specification.
For private-label supply, ask the factory to confirm dimensional tolerances, head-to-shank runout, joint integrity, tooth consistency, marking and pack control. A polished catalog is not evidence that mixed production lots will behave the same. Repeat the application test after any material, cut, joint or process change.
| RFQ Field | Information to Send | Acceptance Evidence |
|---|---|---|
| Workpiece | Material grade, condition, scale or coating | Representative coupon or production part |
| Feature | Photo or drawing, access, allowed removal and finish | Before-and-after inspection record |
| Burr | Shape, cut, head size, cutting length and shank | Controlled SKU and dimensional report |
| Drive | Machine, collet, power, speed range and duty cycle | Stable runout and operating record |
| Commercial | Annual volume, pack, logo, barcode and market | Approved artwork and reorder file |
| Performance | Cycle time, removal, finish, loading and life target | Repeatable result across an agreed sample size |
Frequently Asked Questions
Which details should an importer include in a carbide burr RFQ?
Send the workpiece grade, feature photo or drawing, allowed removal, finish target, shape and cut, sizes, drive, speed, quantity, packaging and destination market, with an approved test method.
Should a distributor build one universal range?
No. Start with common shapes and shanks while keeping material-specific cuts and application limits visible. Add specialist ranges only after demand and testing support them.
Which quality checks support repeat orders?
Control dimensions, runout, tooth geometry, joint integrity, marking, pack count and lot identity, paired with a representative cutting test.
What are carbide burrs used for?
They deburr edges, remove localized stock, dress welds, clean castings, shape contours, blend slots and correct selected features.
Which industries use tungsten carbide rotary burrs?
Metal fabrication, foundry, automotive, aerospace, energy, shipbuilding, tool-and-die, mold repair and industrial maintenance all use them, subject to application-specific approval.
How do carbide burrs differ from blades and abrasive tools?
Burrs cut chips for localized shaping; blades scrape accessible edges; abrasive points and wheels grind and wear to a different profile.
Can carbide burrs be used for weld removal, casting cleanup and edge finishing?
Yes, when shape, cut, head size, speed and drive match the work. A broad final blend may require a following abrasive process.
Are carbide burrs suitable for pneumatic, electric, robotic and CNC deburring?
Selected models can be, but suitability is model-specific and requires confirmation of holder, speed, power, runout, shank length, path, guarding and restrictions.
How do buyers choose shape, cut, material range and shank size?
Choose shape from access, cut from material and chip behavior, head size from contact area, and shank from the exact collet, then approve on a representative part.
Final Thoughts
Do not source carbide burrs as a universal grinding accessory. Build the range around verified applications, materials, shapes, cuts, shanks and drive limits. A documented sample test gives distributors stronger product claims, fewer returns and more reliable repeat orders.
Discuss Your Application | Request an OEM Burr Range
Related Product and Buyer Guides
- Tungsten Carbide Burrs
- Carbide Burr Shapes
- Double Cut Carbide Burr
- Single Cut Carbide Burr
- Shape Chart
- Size Chart