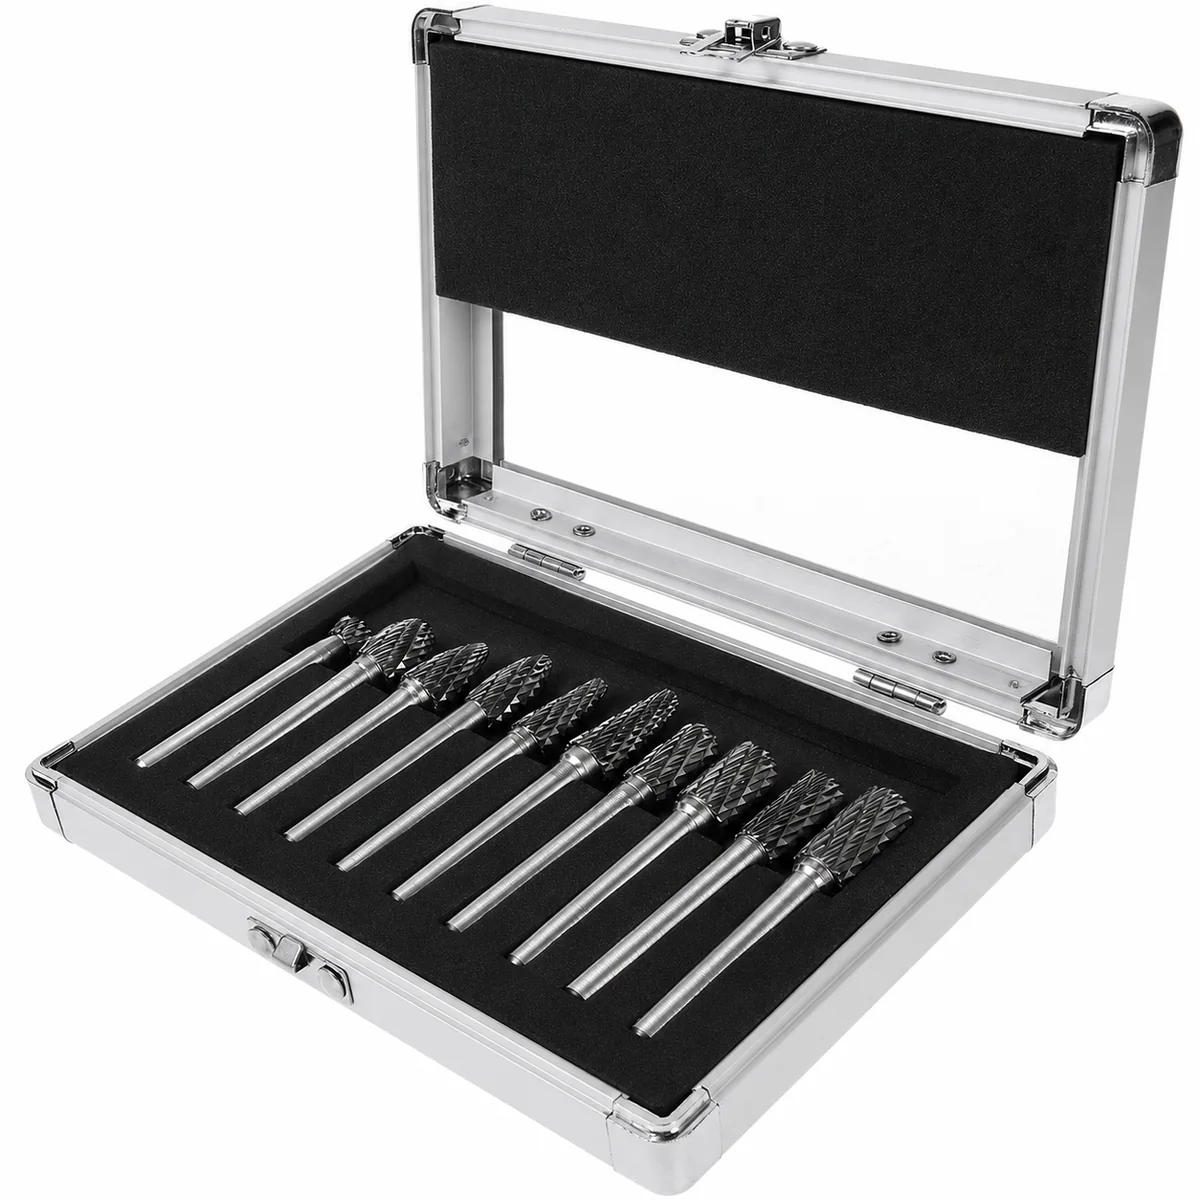
Long Carbide Burr Bits for Standard Recesses
Moderate extensions for recessed edges and welds where you can maintain rigid holding, controlled side contact and a verified operating range.

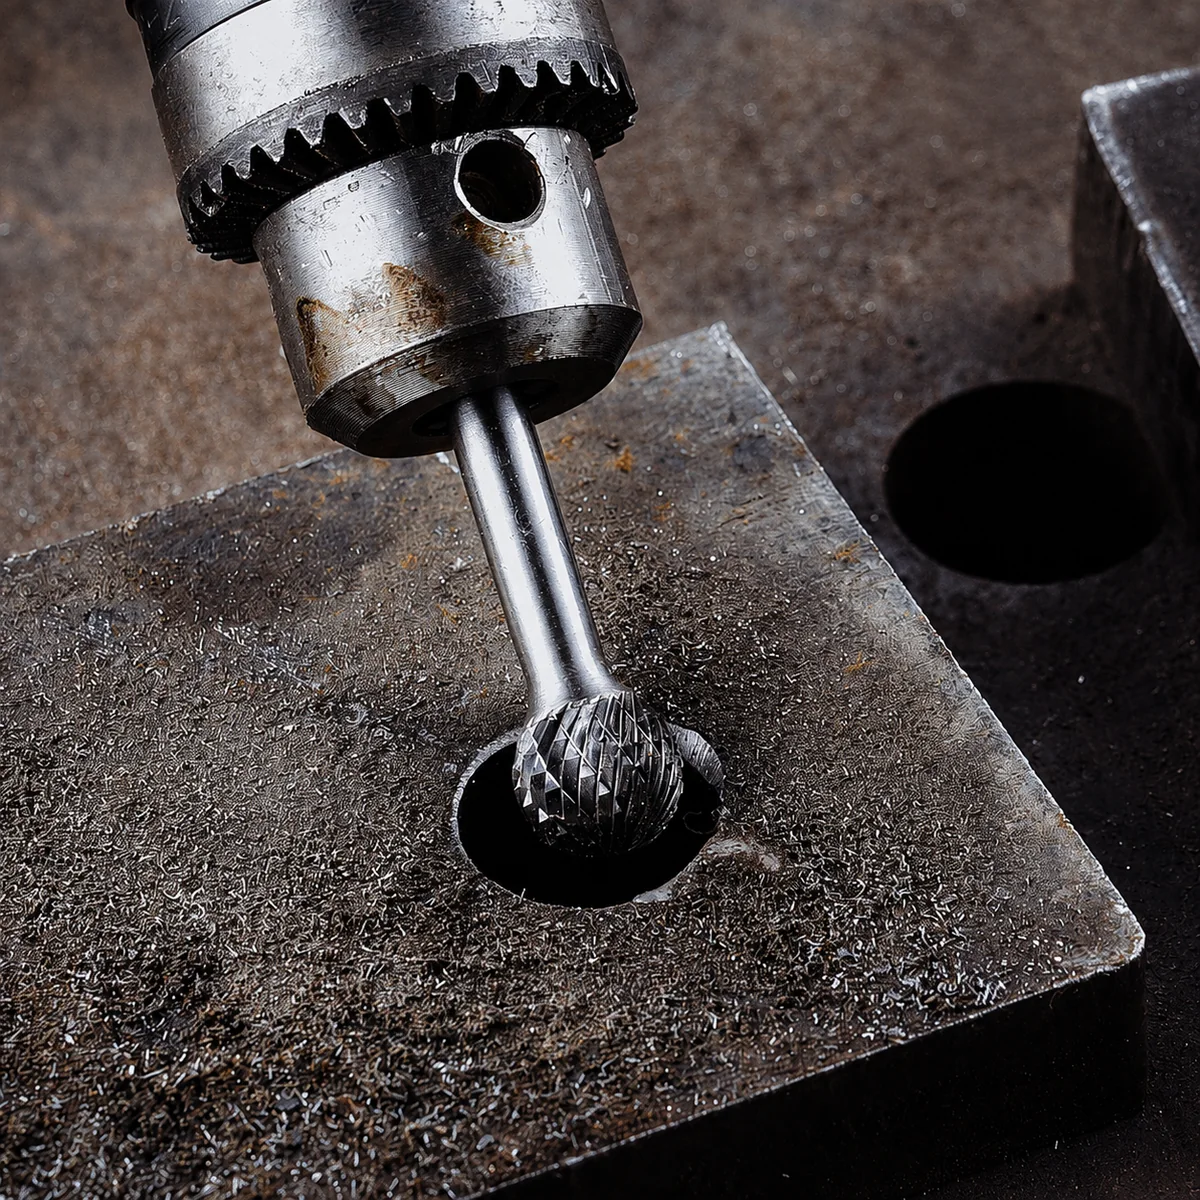
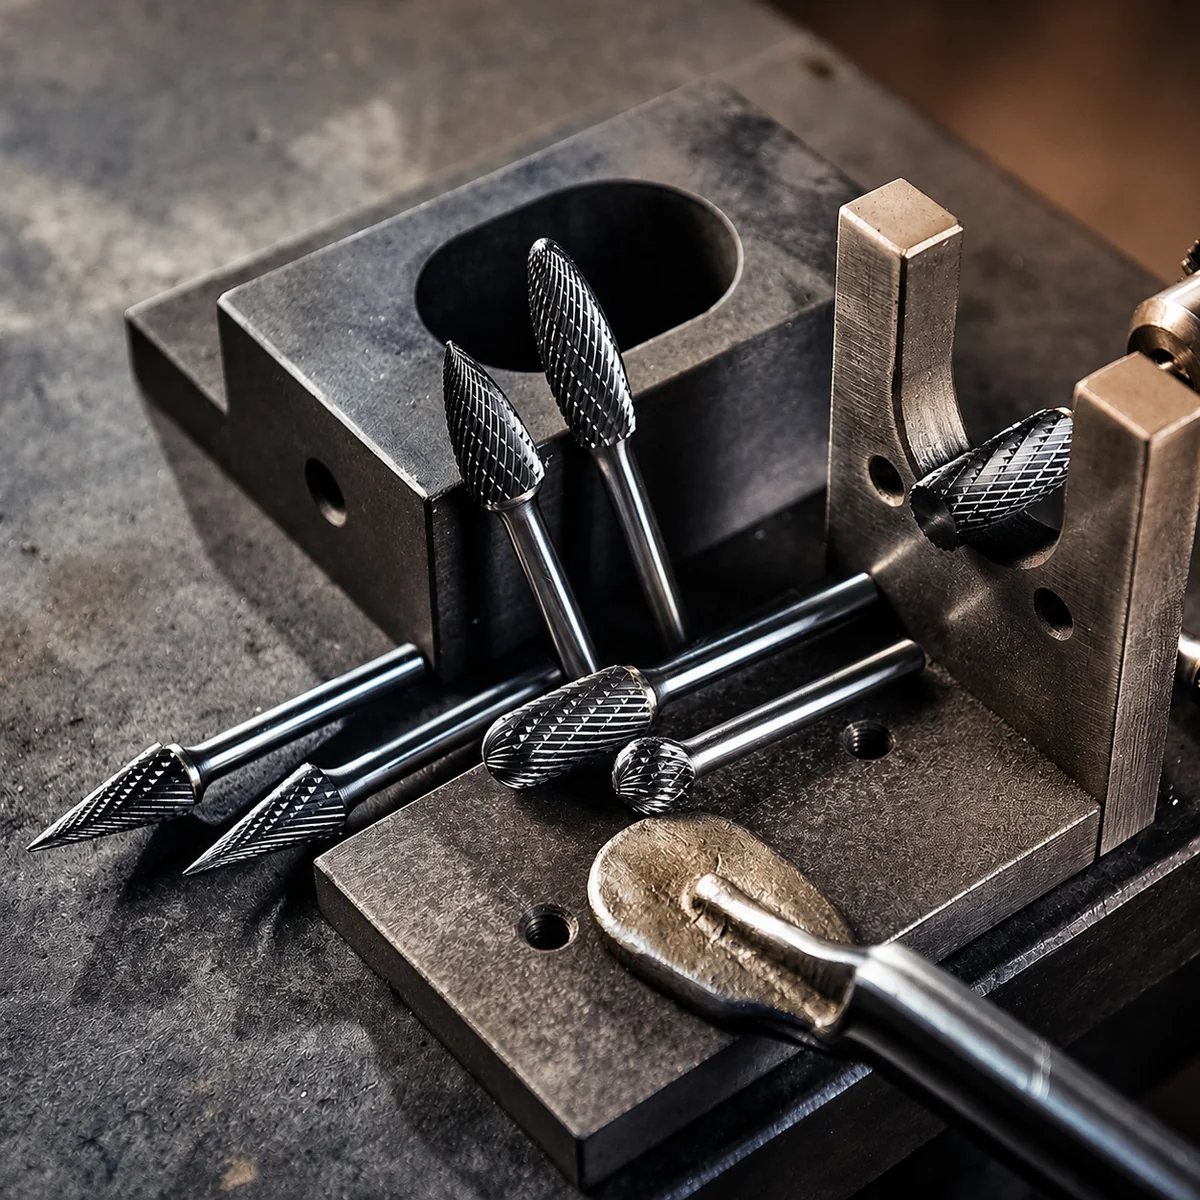
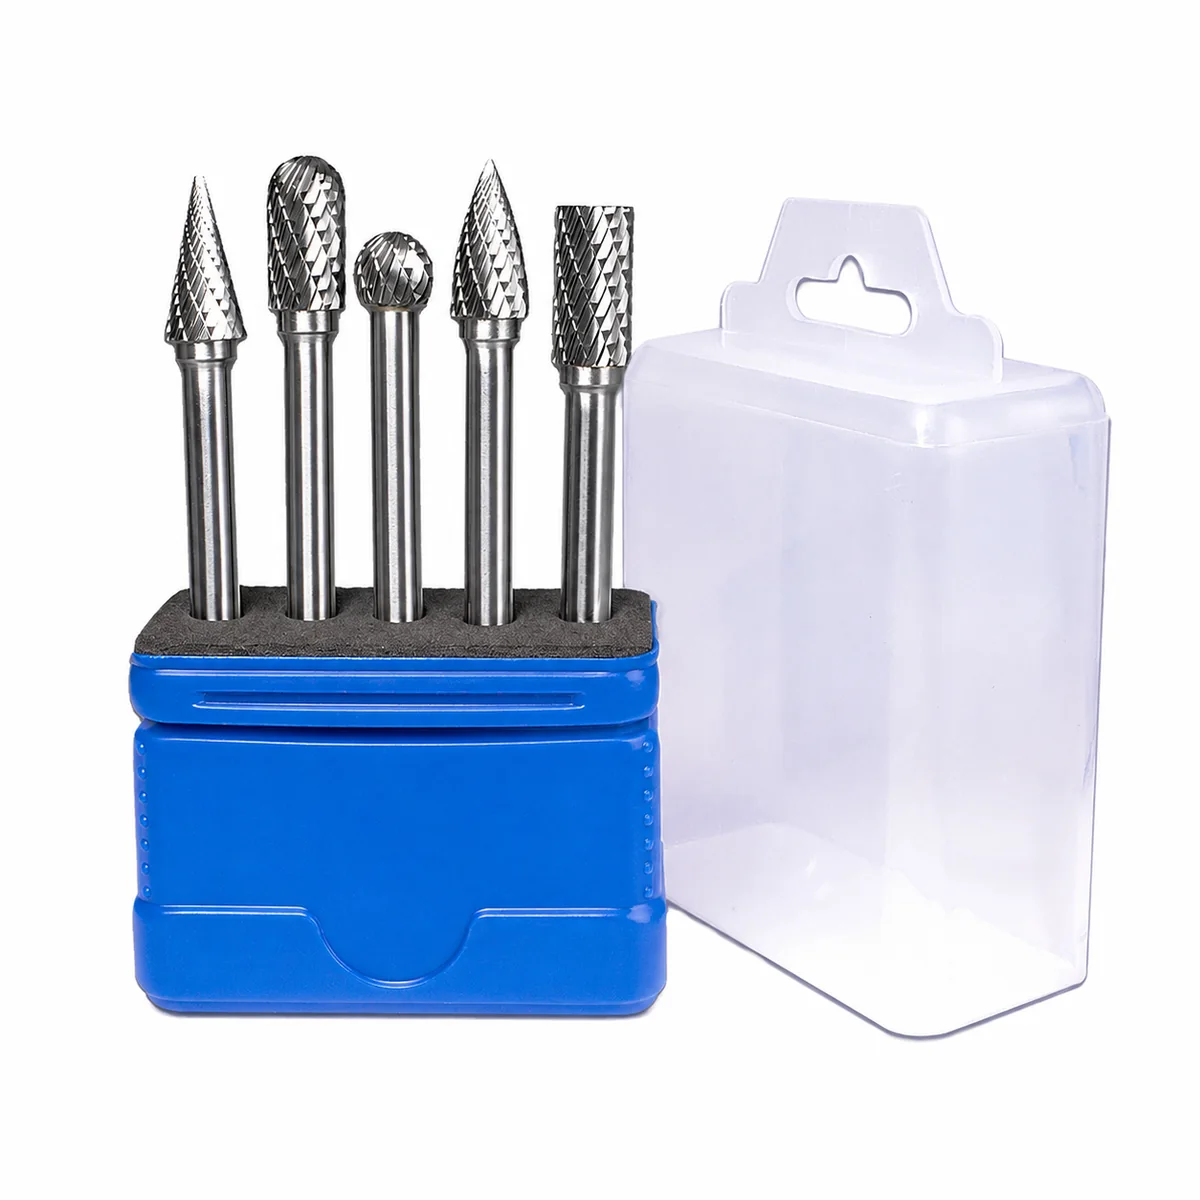
A Long Shank Carbide Burr reaches recessed welds, cavities, bores and internal passages that a standard tool cannot access with sufficient grinder clearance. Extra reach also increases sensitivity to overhang, side load, runout and drive condition, so every model needs its own dimensional and operating record. AXIME TOOLS structures the range around usable reach, head shape, cut, shank construction and workpiece material. You can then connect the approved sample to OEM marking, labels, protective packaging and repeat-order codes without treating every long tool as interchangeable.
Each product option remains connected to its corresponding record so buyers can build a controlled assortment.

Moderate extensions for recessed edges and welds where you can maintain rigid holding, controlled side contact and a verified operating range.

Additional reach for deep cavities and internal passages, quoted only after the feature opening, working depth, tool support and drive are confirmed.

Nominal six-inch requests must be converted into head size, cutting length, shank diameter, overall length and usable reach before quotation.

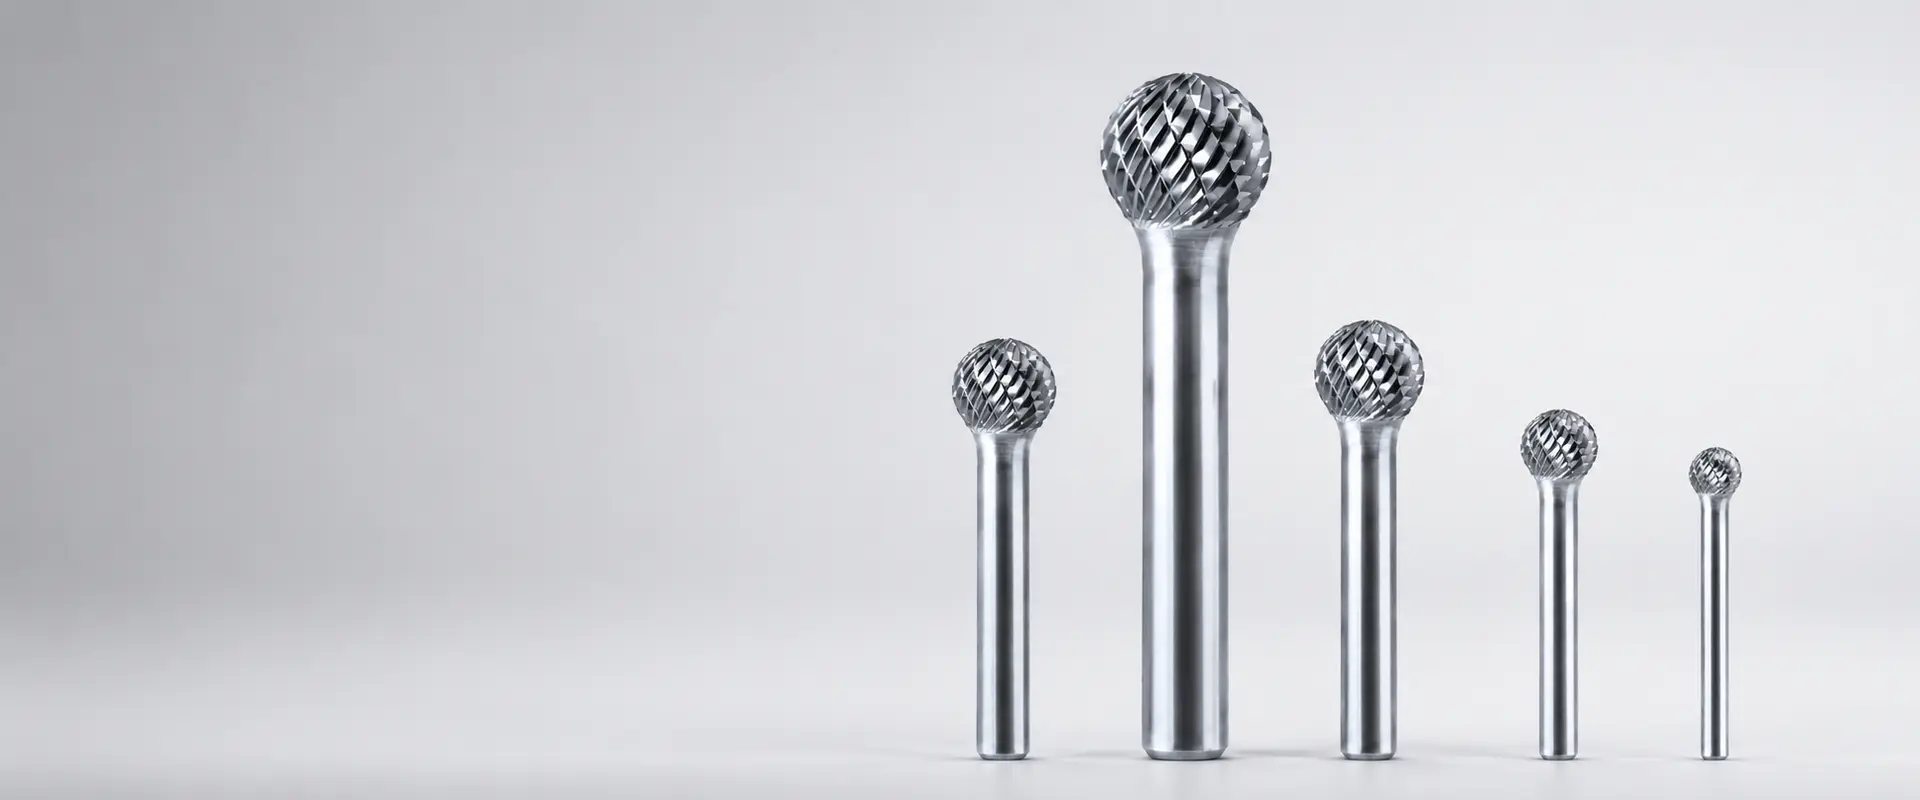
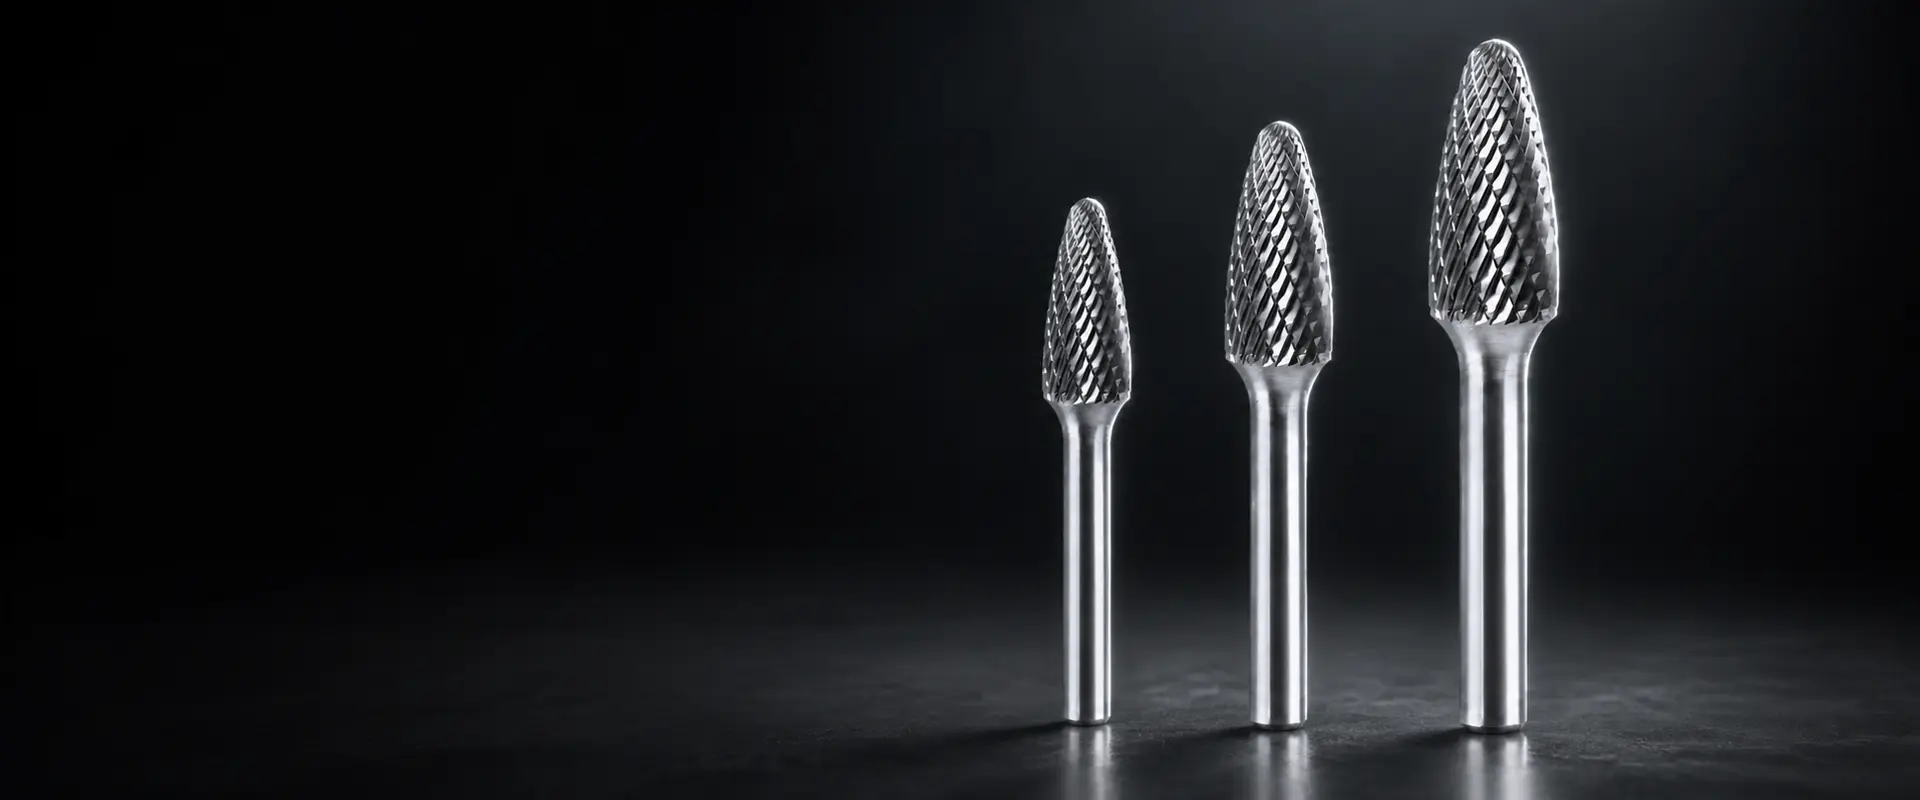
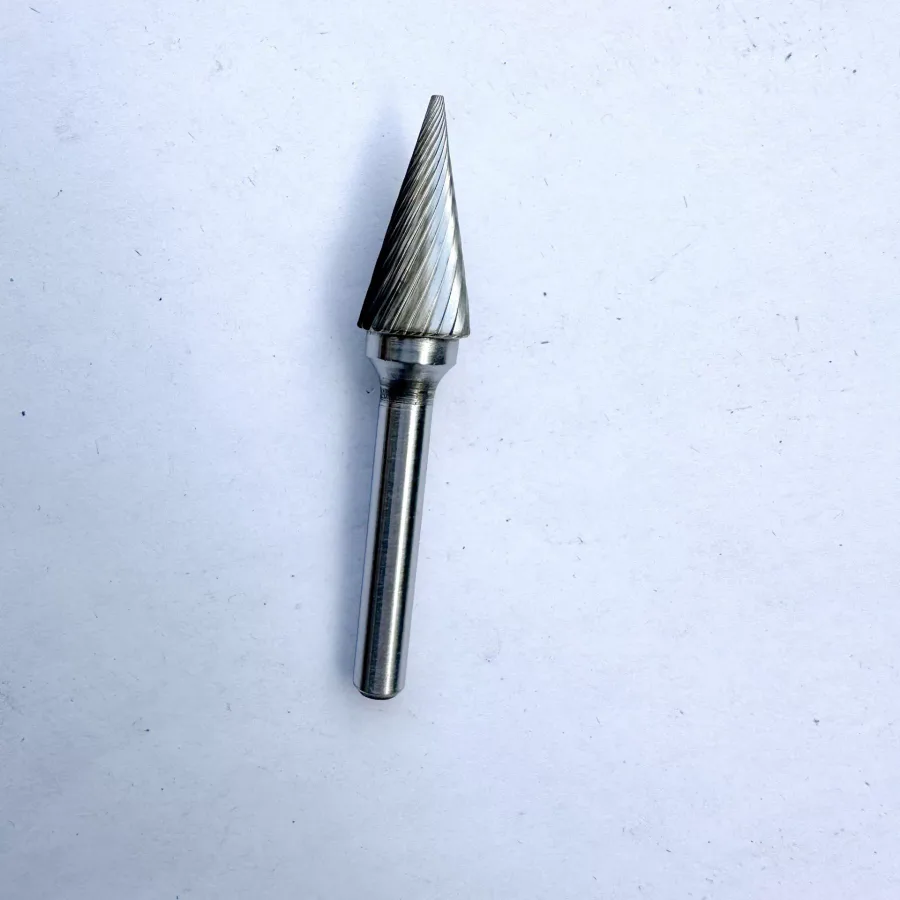
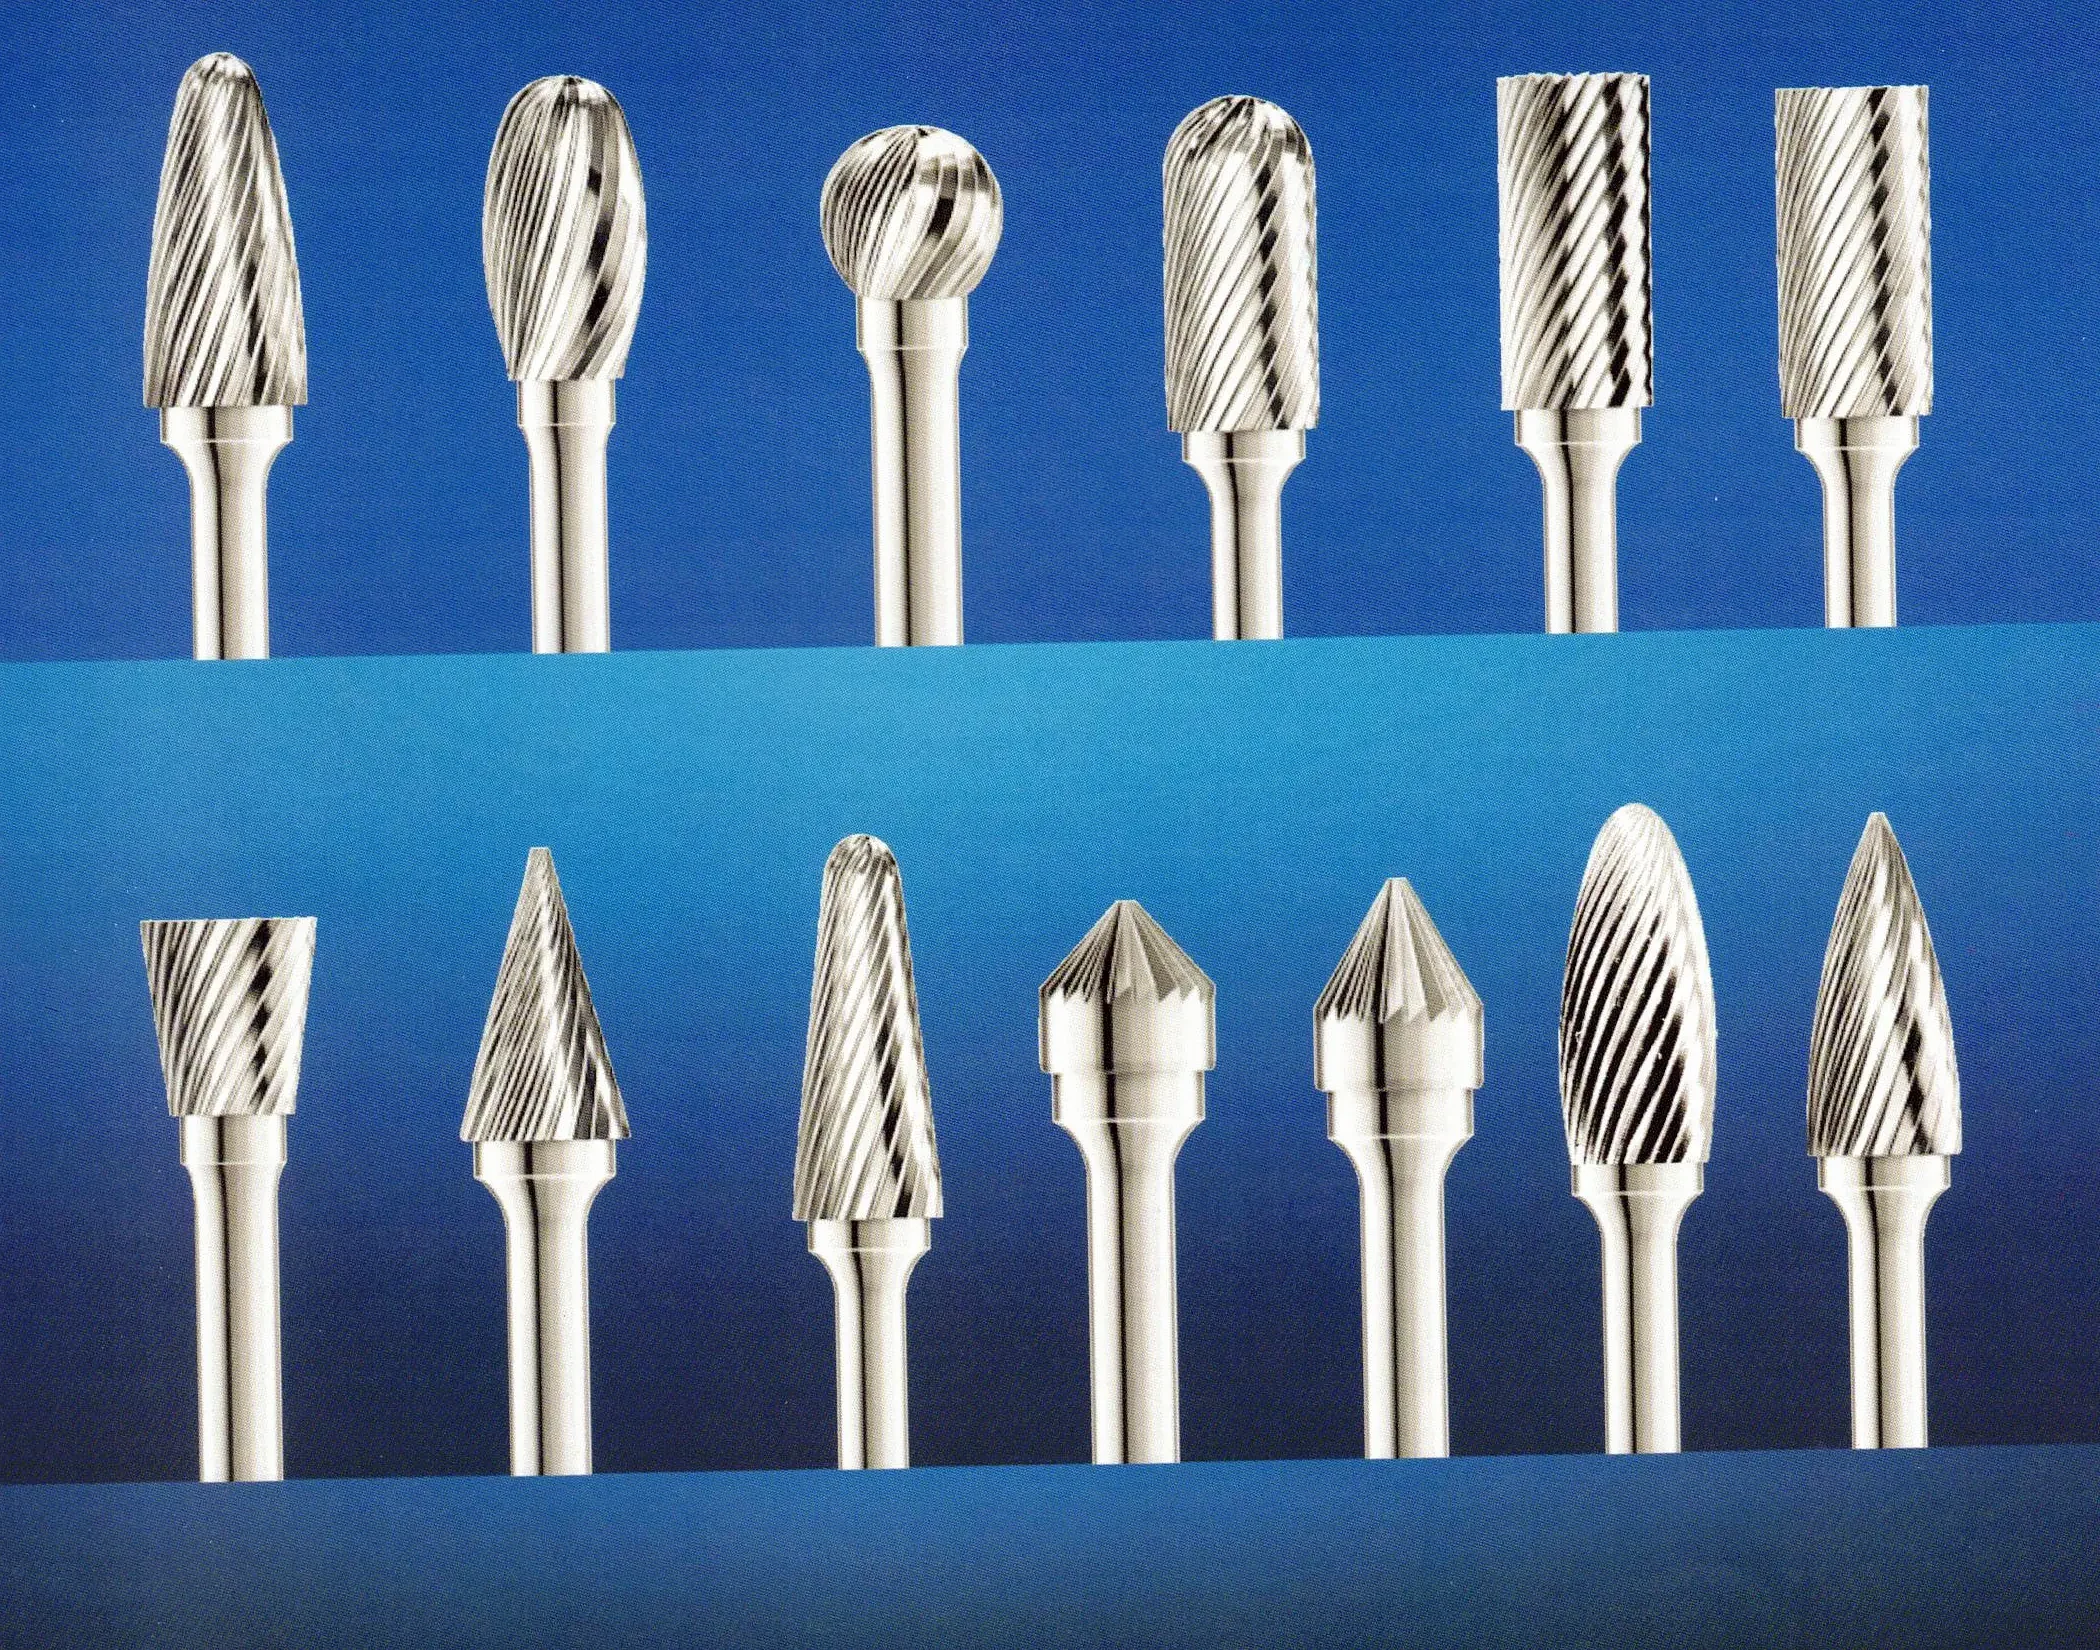
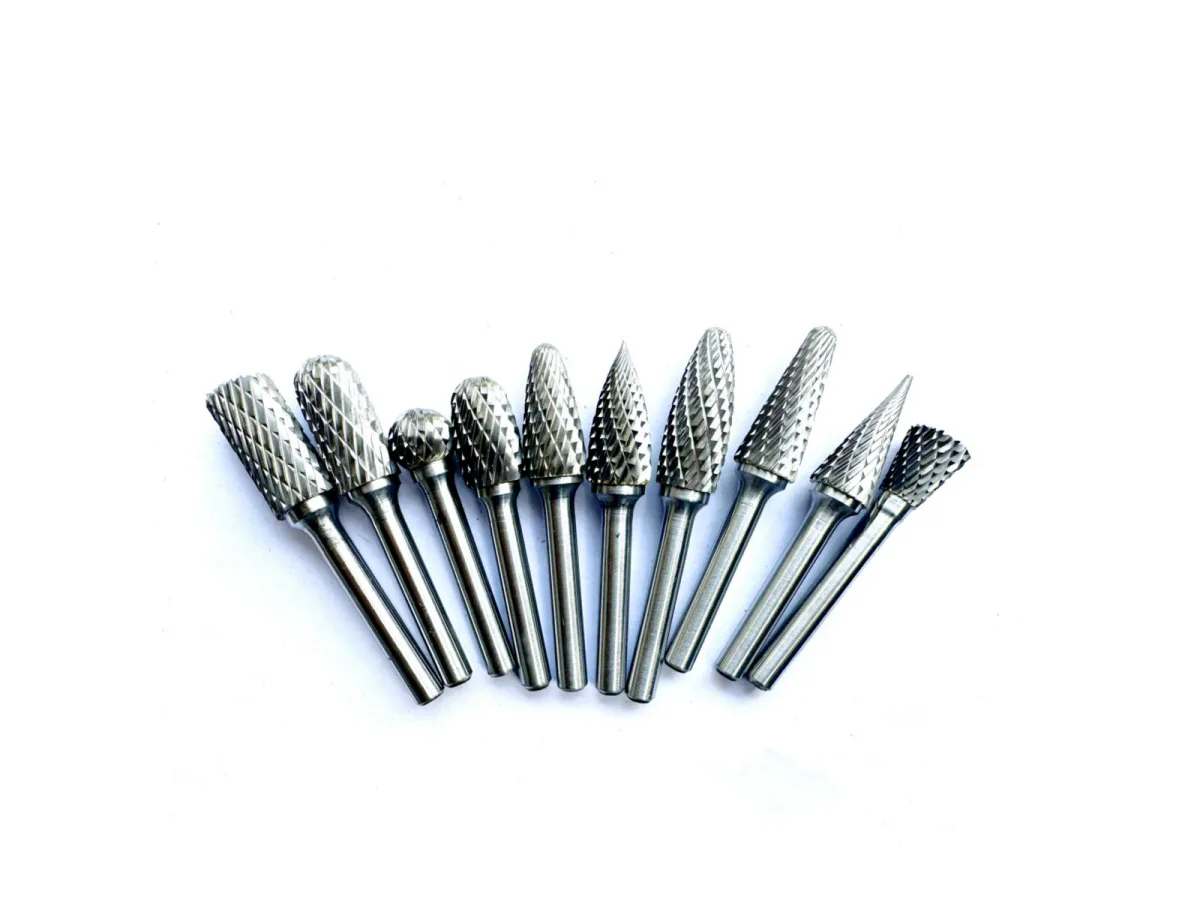
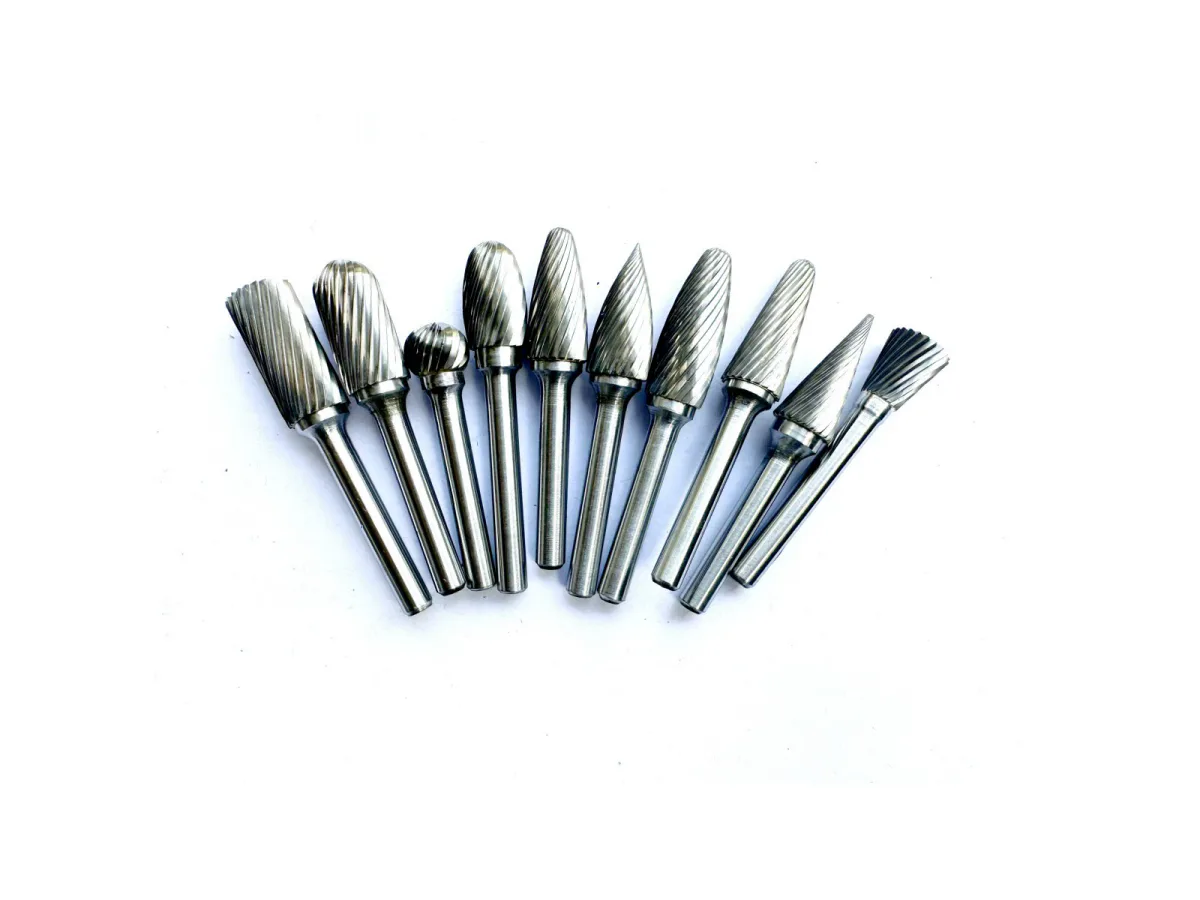
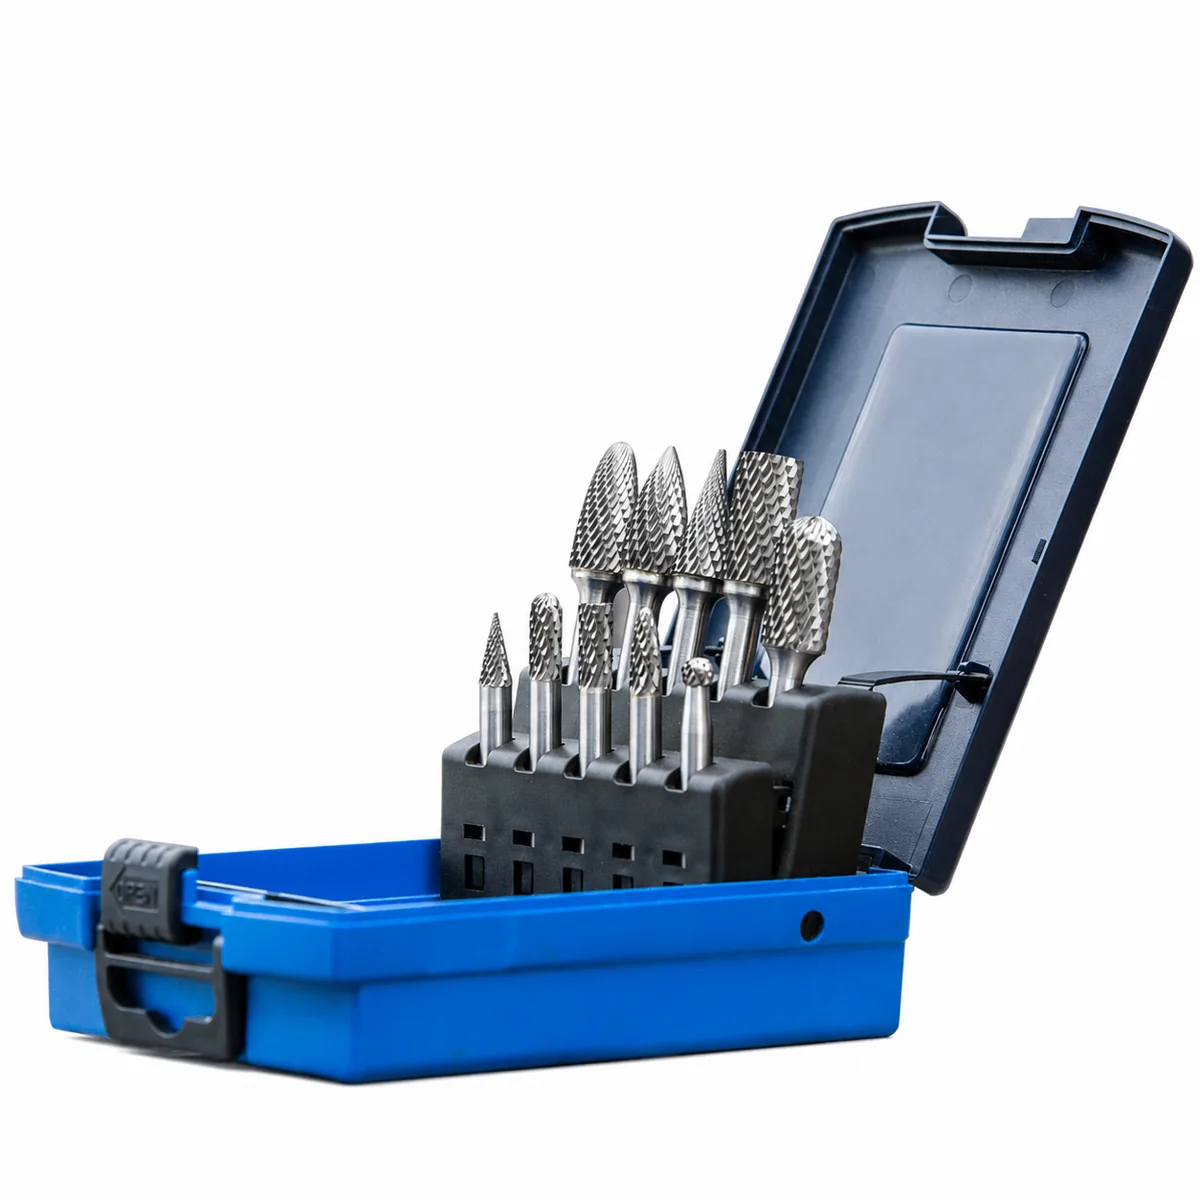
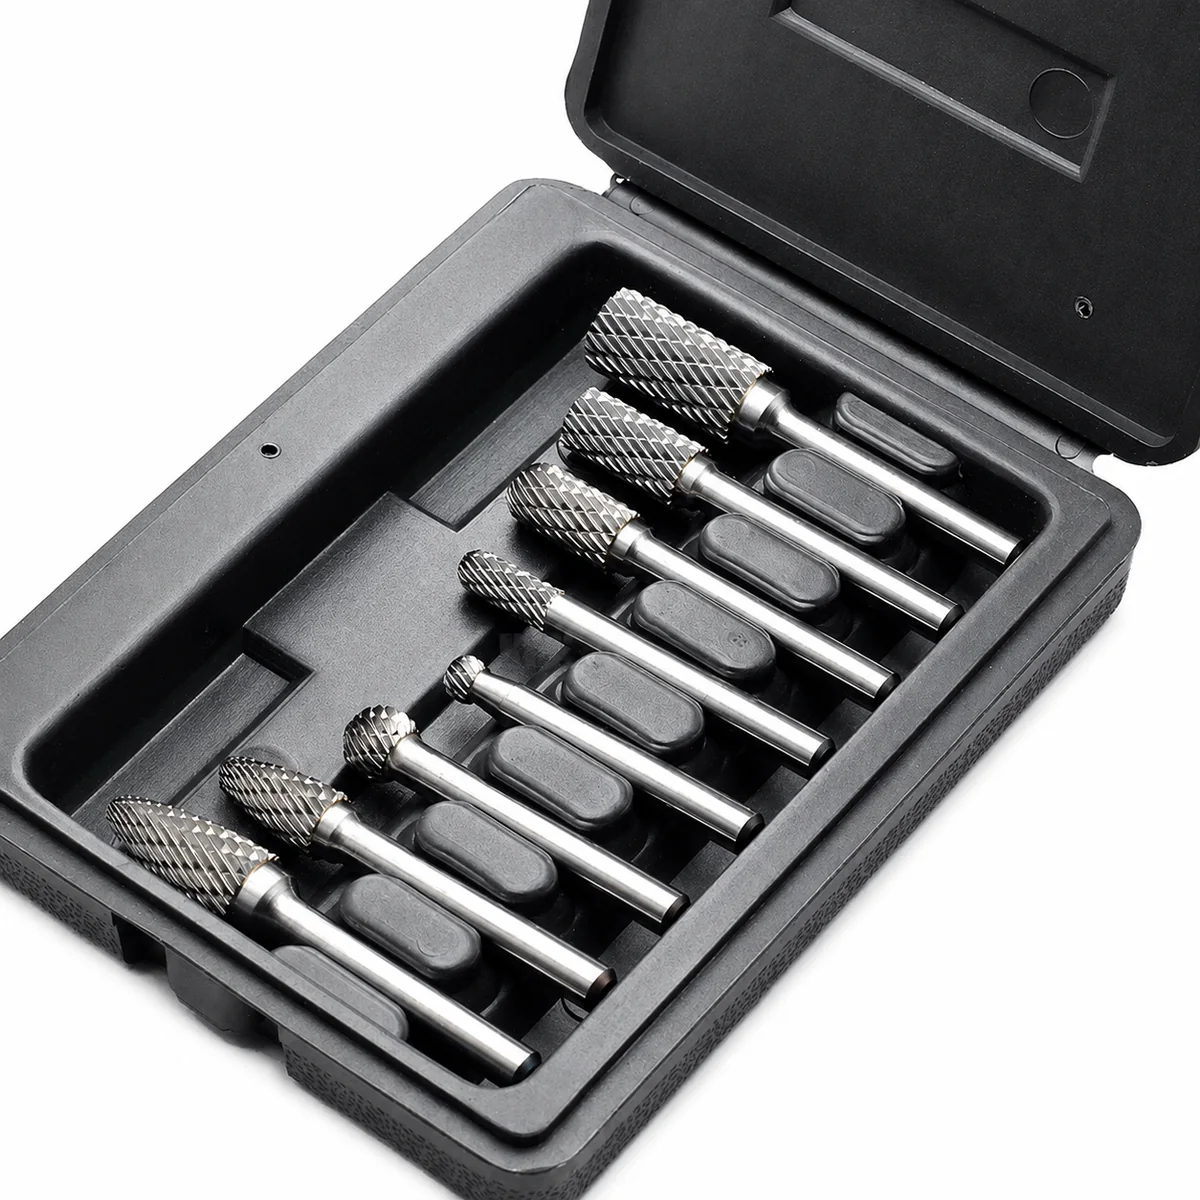
Cylinder, radius, ball, oval, tree, flame and tapered families are shortlisted from the internal surface and approach path; availability remains model-specific.

Selected shapes, dimensions, labels and packaging can form a distributor program only after the technical matrix and representative samples are approved.
These products solve different access problems. Do not merge them because buyers use similar search language. The quotation should state which construction is being supplied and which operating instructions govern it. Terminology Boundary: A flexible-shaft drive is not the same as a flexible burr shank. Never substitute products from the search phrase alone.
A longer tool is valuable only when the standard burr and grinder nose cannot reach the cutting point. You should send the opening diameter, depth from the collet face, working angle and required contact direction. AXIME TOOLS can then shortlist the smallest effective extension instead of adding unsupported length that increases bending leverage and makes the operator fight vibration.
Long-shank tools should not inherit the speed note of a standard model just because the head diameter appears equal. Permissible speed also depends on unsupported length, construction, cut, material, contact condition and drive rigidity. Your catalog, sample report and carton insert should point to the approved model-level range rather than publishing one universal RPM for the whole collection.
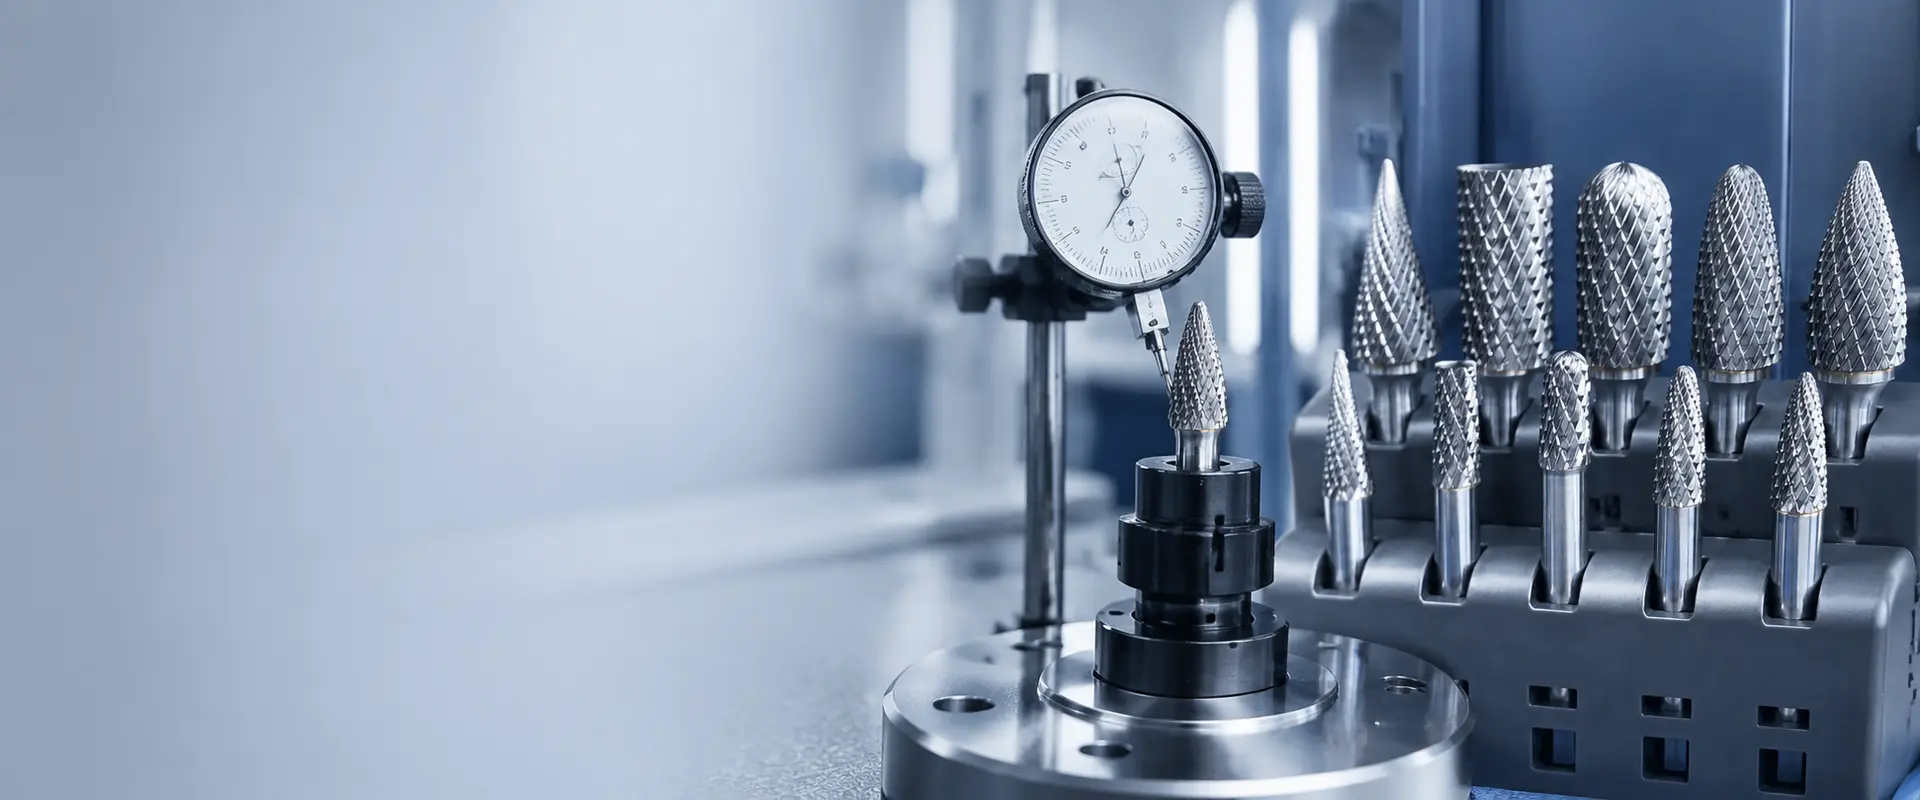
Deep-access buyers notice instability immediately. A sound range needs a straight shank, controlled head-to-shank alignment, a consistent joint, undamaged teeth and an exact collet interface. Agree how dimensions and runout will be checked, then repeat the same method for production lots. The inspection record should identify the model and sample quantity instead of making an unsupported whole-range claim.
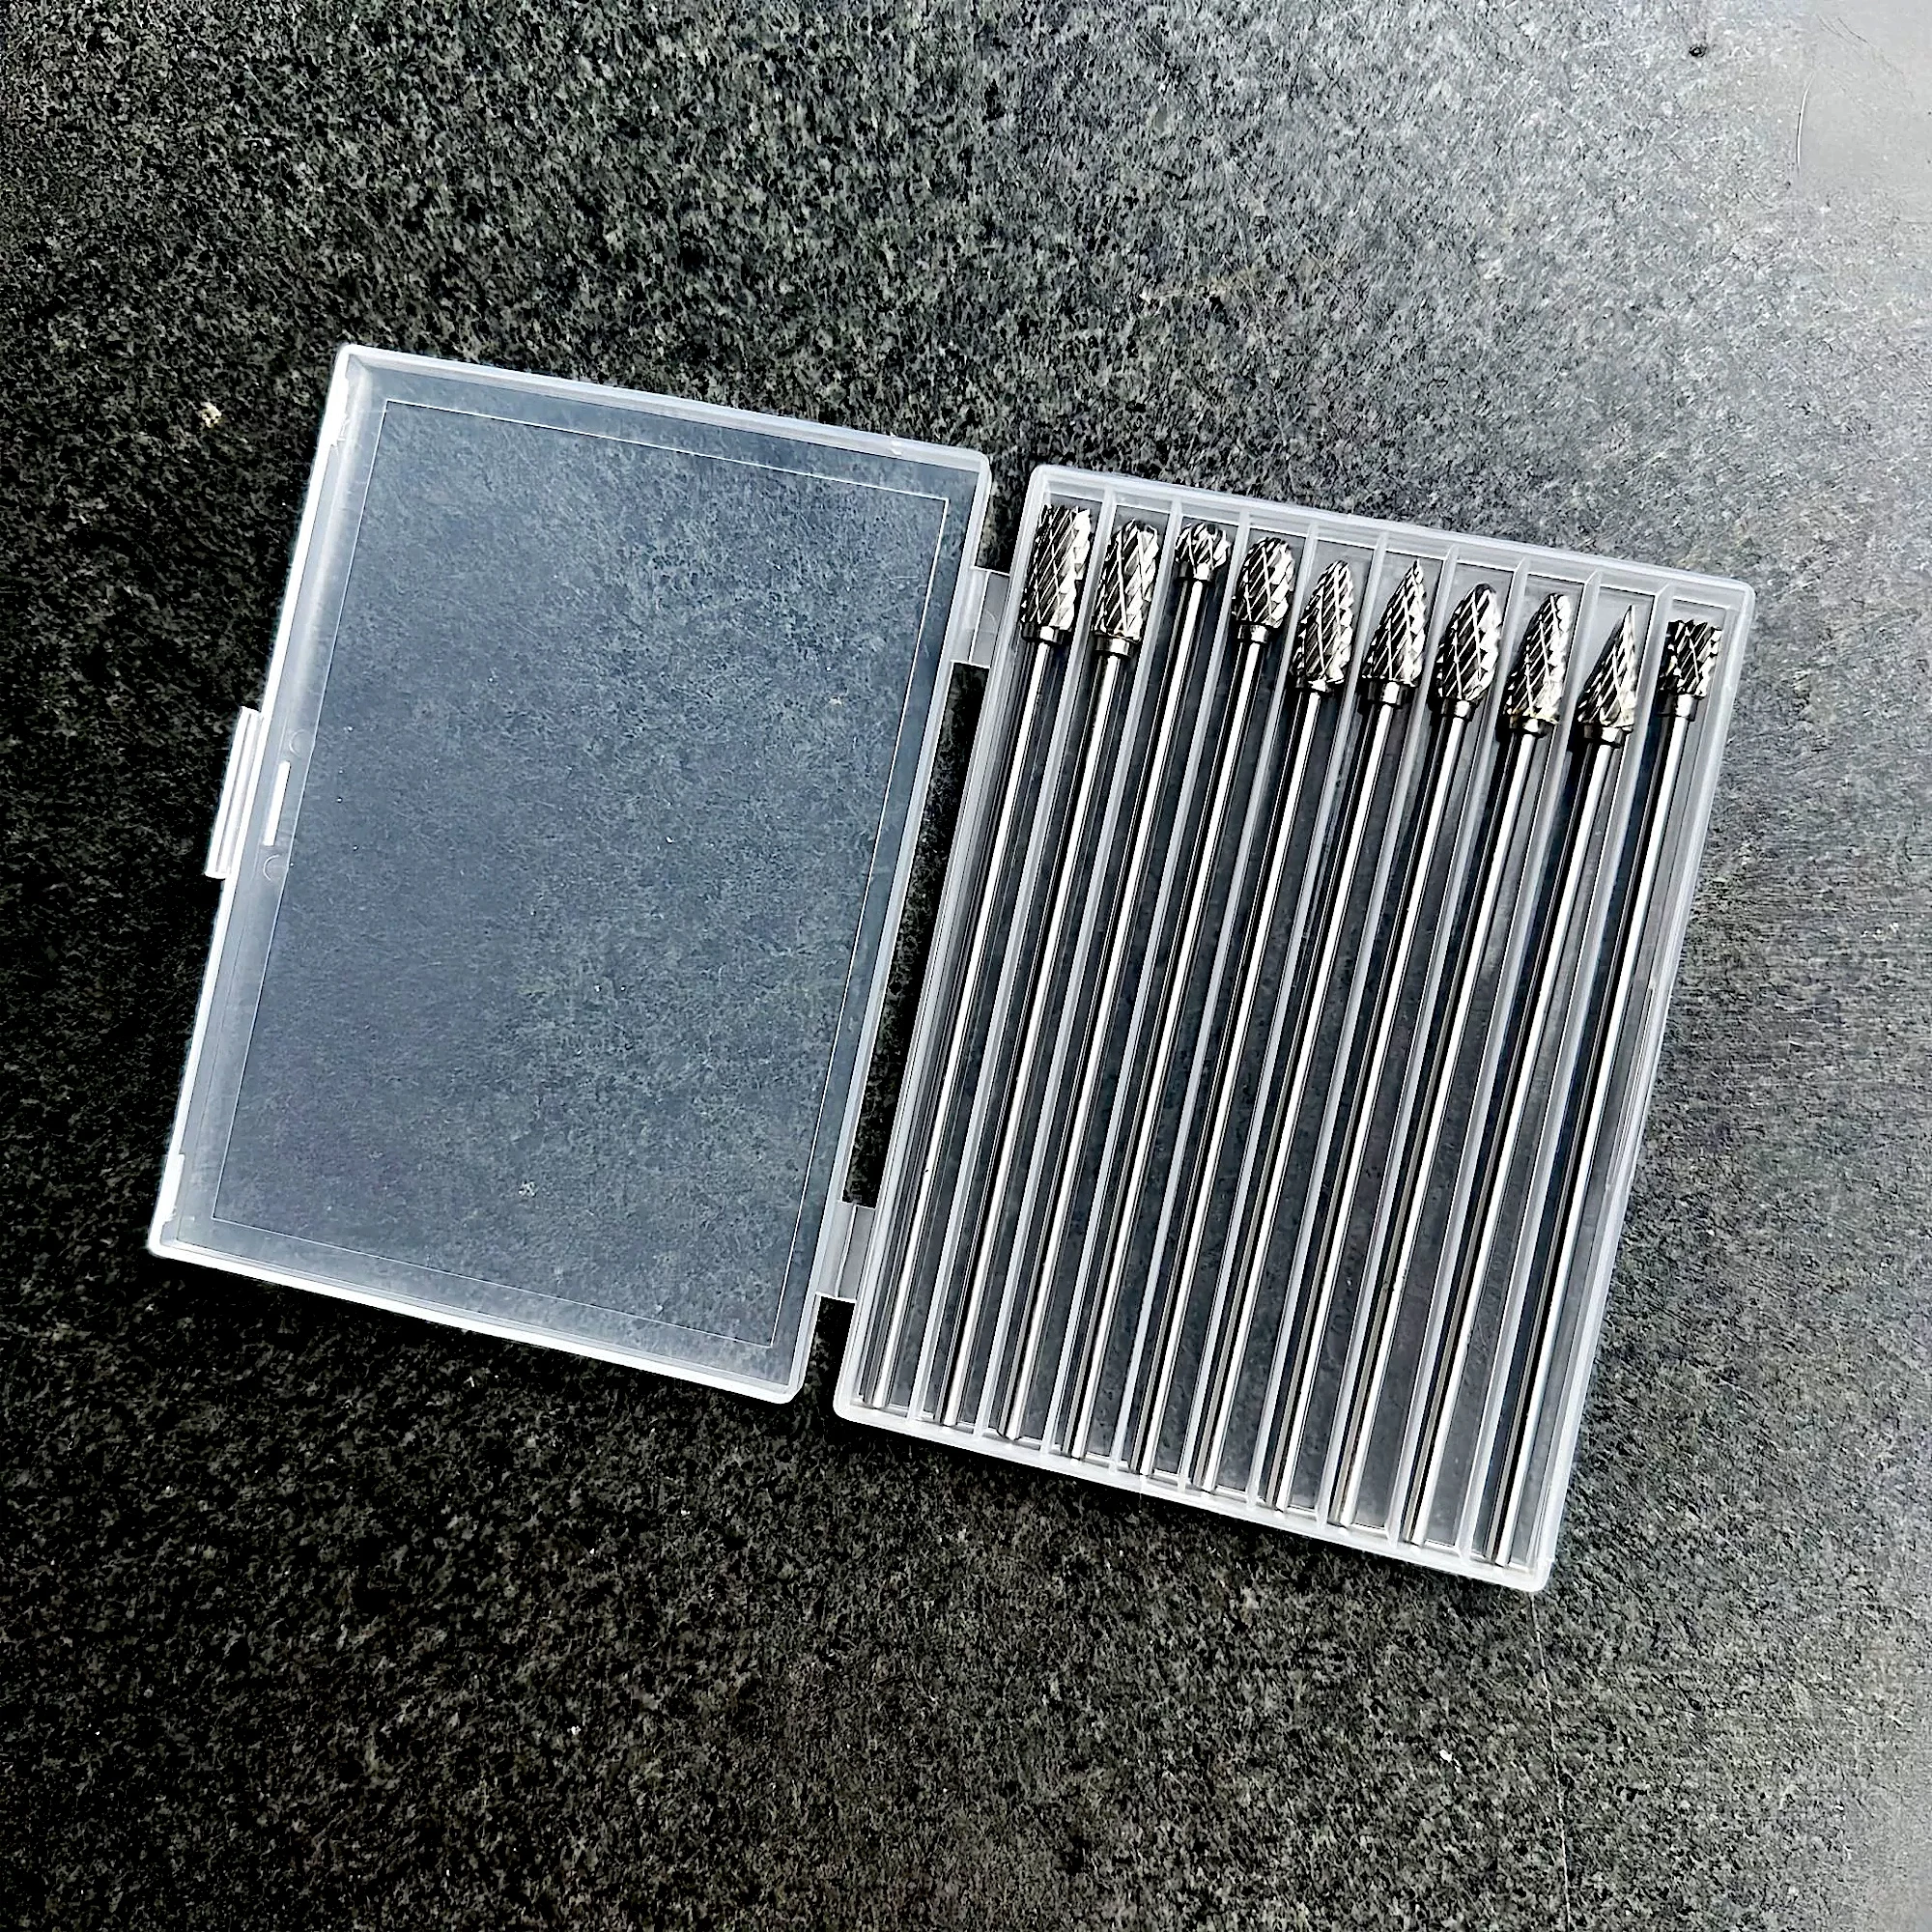
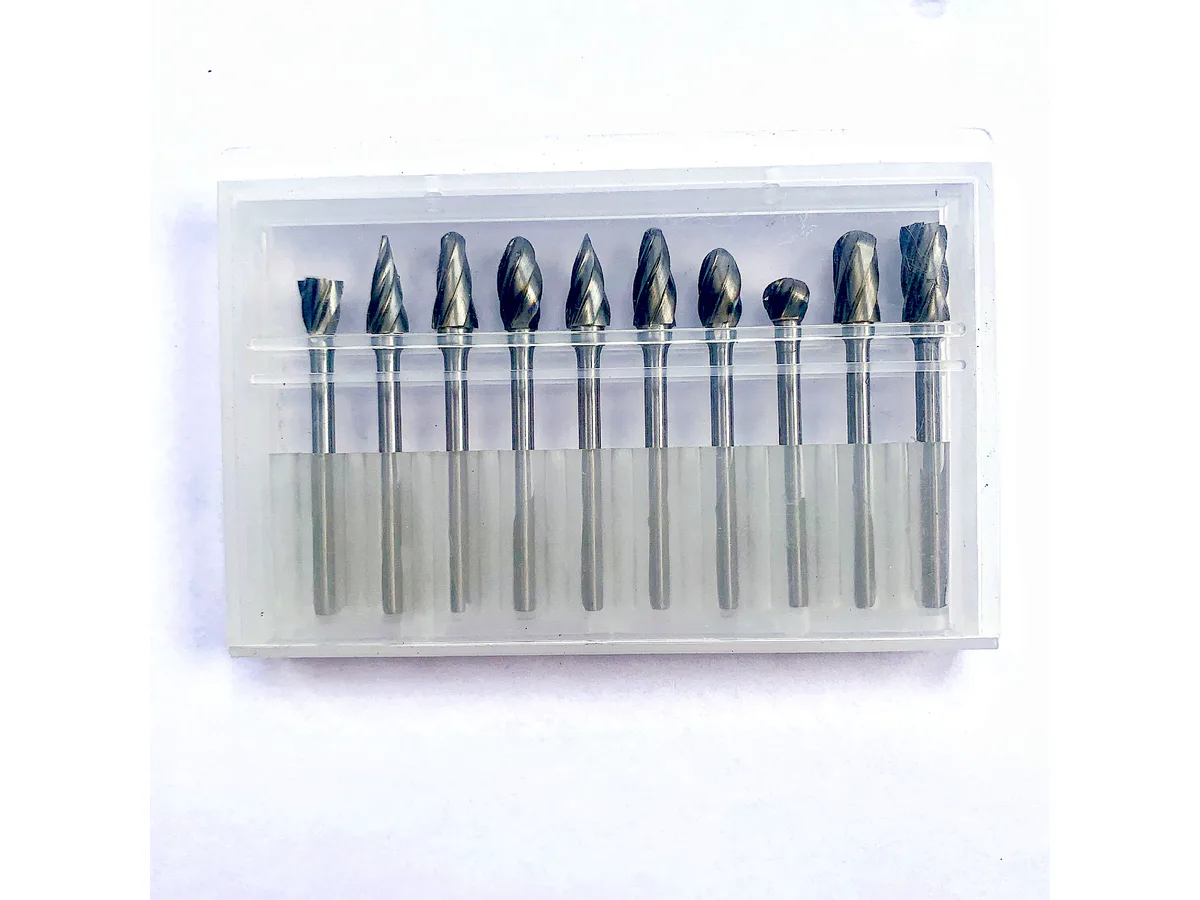
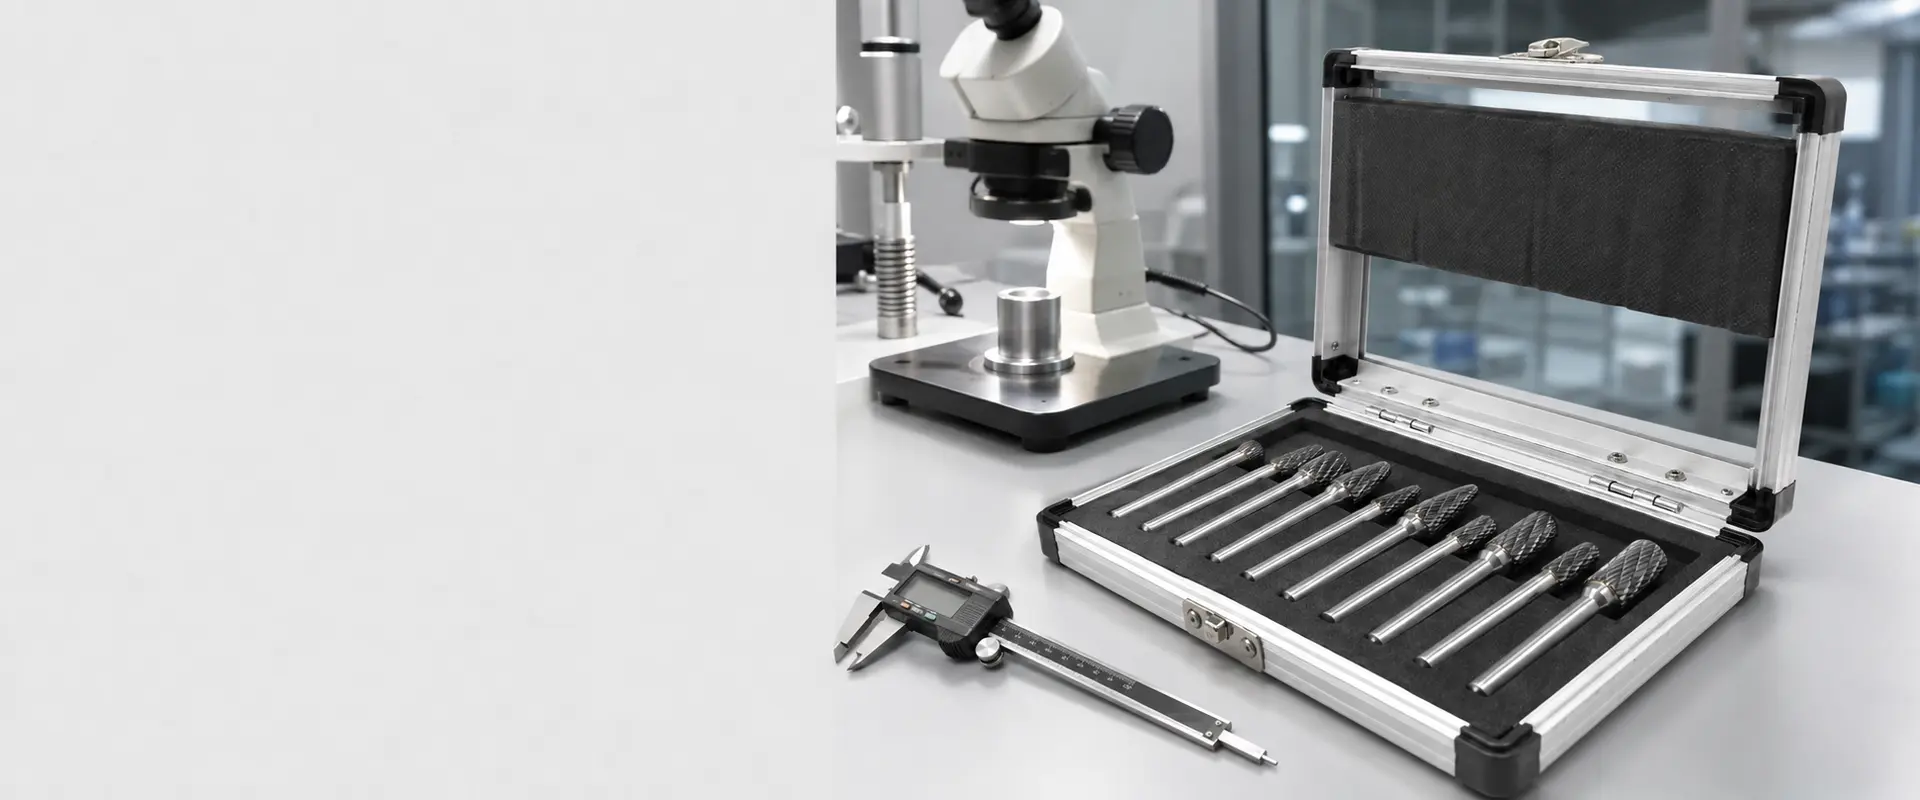
Private-label work begins after the technical assortment is frozen. You can specify laser marking where space permits, model and dimension labels, individual sleeves or tubes, set cases, barcodes and export cartons. Keep usable reach, head shape, cut and shank on the same controlled SKU so artwork cannot turn two similar-looking long tools into one ambiguous replacement item.
| System | Best Fit | Buyer Must Confirm |
|---|---|---|
| Factory Long-Shank Burr | Repeat deep-access work with a controlled one-piece SKU | Head, reach, construction, speed and runout |
| Carbide Burr Extension | Occasional access using an approved spindle-extension system | Holder rating, tool size, alignment and no stacked extensions |
| Flexible Shank Carbide Burr | A separate flexible construction or product family | Drawing, drive method, bend limits and supplier approval |
Request the Long-Shank Model Matrix
Send Selection Requirements →Build an extended-reach burr range around usable working length, head geometry, cut type and approved operating limits—with OEM support for importers and distributors.
Working distance is measured from the collet face, not inferred from overall length.
Metric and inch shanks remain separated in quotations, labels and replacement records.
Each SKU retains its approved head geometry, tooth pattern and material guidance.
Long-shank operating limits stay linked to the exact model and contact condition.
Individual sleeves or fixed cavities reduce impact and bending risk during transport.
Artwork and packaging revisions cannot silently alter the approved cutting-tool specification.
Build an extended-reach burr range around usable working length, head geometry, cut type and approved operating limits—with OEM support for importers and distributors.

Reach weld metal behind flanges, inside frames and along confined joints without presenting every extended tool as universal. You should define the bead location, parent material, access angle and allowed removal. Cylinder, radius, tree or oval profiles can then be evaluated on a representative joint before a wholesale range is approved.

Remove fins, gate remnants and localized defects inside pockets only after you confirm the opening, depth, interrupted surface and contact direction. Long reach improves access, but rough cast skin can increase impact and vibration. A sample test should record chatter, tooth condition and remaining geometry, not only removal speed.

Blend ports, bores, pipe transitions and molded passages with a head profile that follows the intended contour. You should send a section drawing or clear dimensions because overall length alone does not prove that the head can enter and move. Keep the shank and joint away from the workpiece throughout the approved path.

Correct restricted radii and cavity details while protecting adjacent finished surfaces. The smallest effective head and reach usually give better control than the longest available tool. Buyers should define finish allowance, visibility, drive access and inspection method before selecting pointed, radius, ball or tapered profiles.
These products solve different access problems. Do not merge them because buyers use similar search language. The quotation should state which construction is being supplied and which operating instructions govern it. Terminology Boundary: A flexible-shaft drive is not the same as a flexible burr shank. Never substitute products from the search phrase alone.
| System | Best Fit | Buyer Must Confirm |
|---|---|---|
| Factory Long-Shank Burr | Repeat deep-access work with a controlled one-piece SKU | Head, reach, construction, speed and runout |
| Carbide Burr Extension | Occasional access using an approved spindle-extension system | Holder rating, tool size, alignment and no stacked extensions |
| Flexible Shank Carbide Burr | A separate flexible construction or product family | Drawing, drive method, bend limits and supplier approval |
These products solve different access problems. Do not merge them because buyers use similar search language. The quotation should state which construction is being supplied and which operating instructions govern it. Terminology Boundary: A flexible-shaft drive is not the same as a flexible burr shank. Never substitute products from the search phrase alone.
Request the Long-Shank Model Matrix
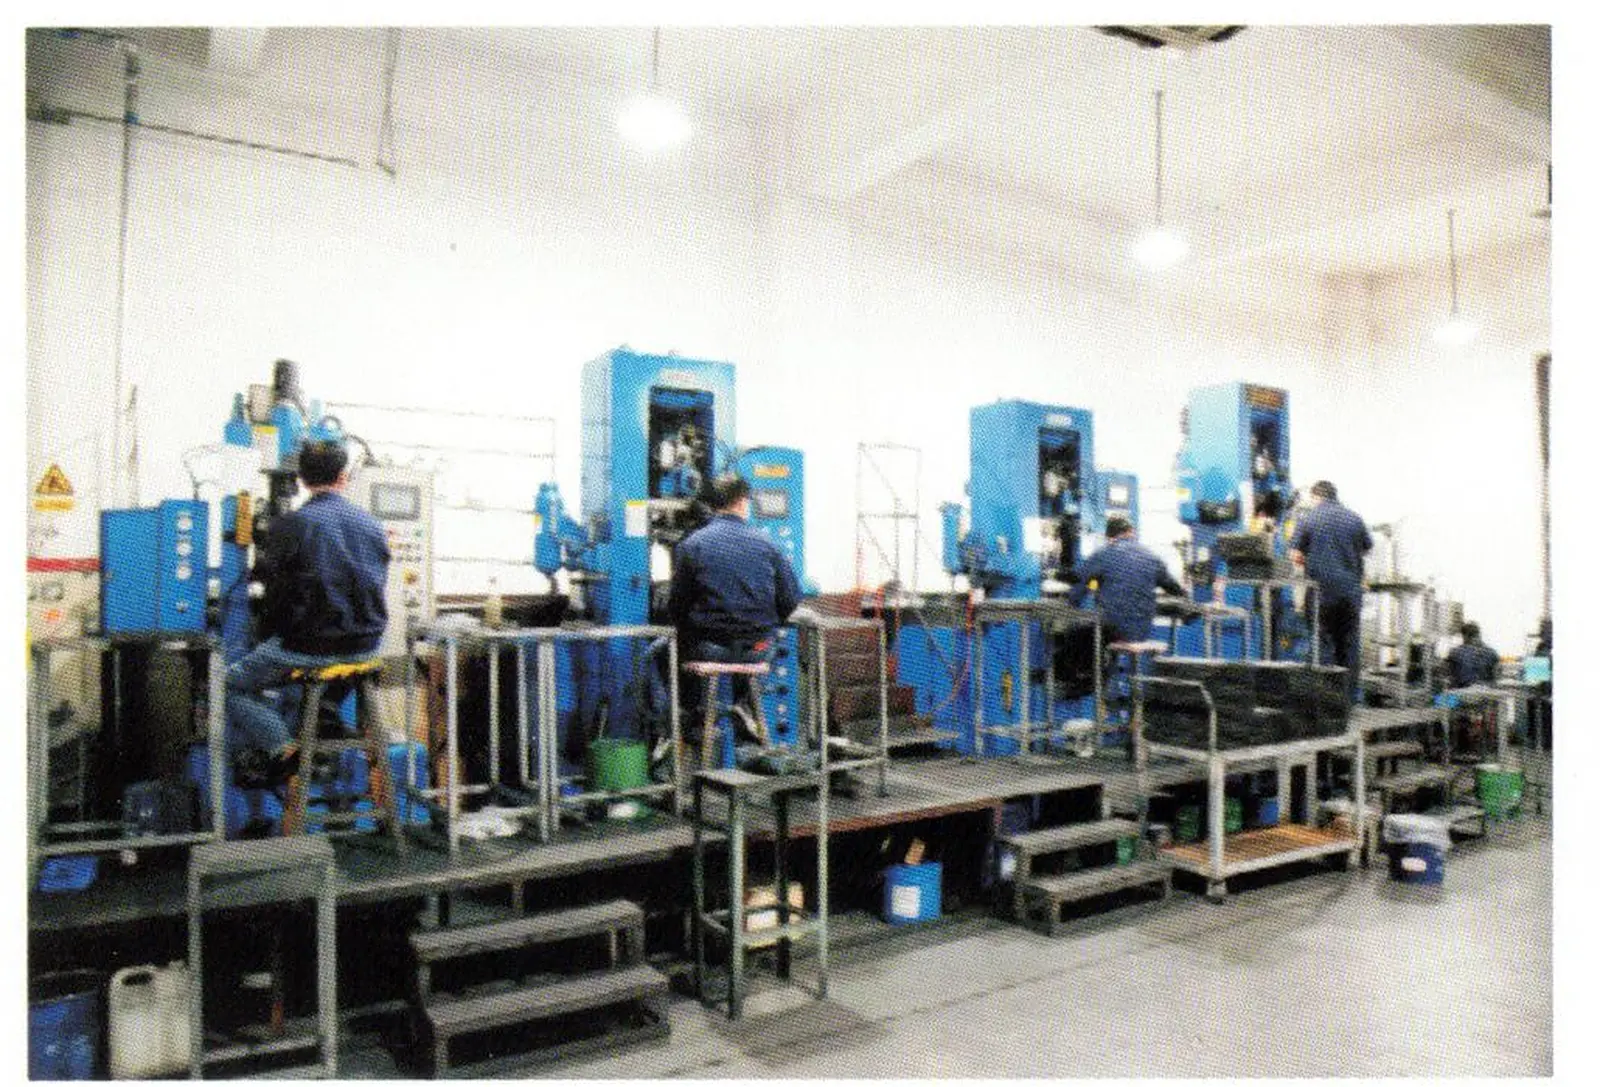
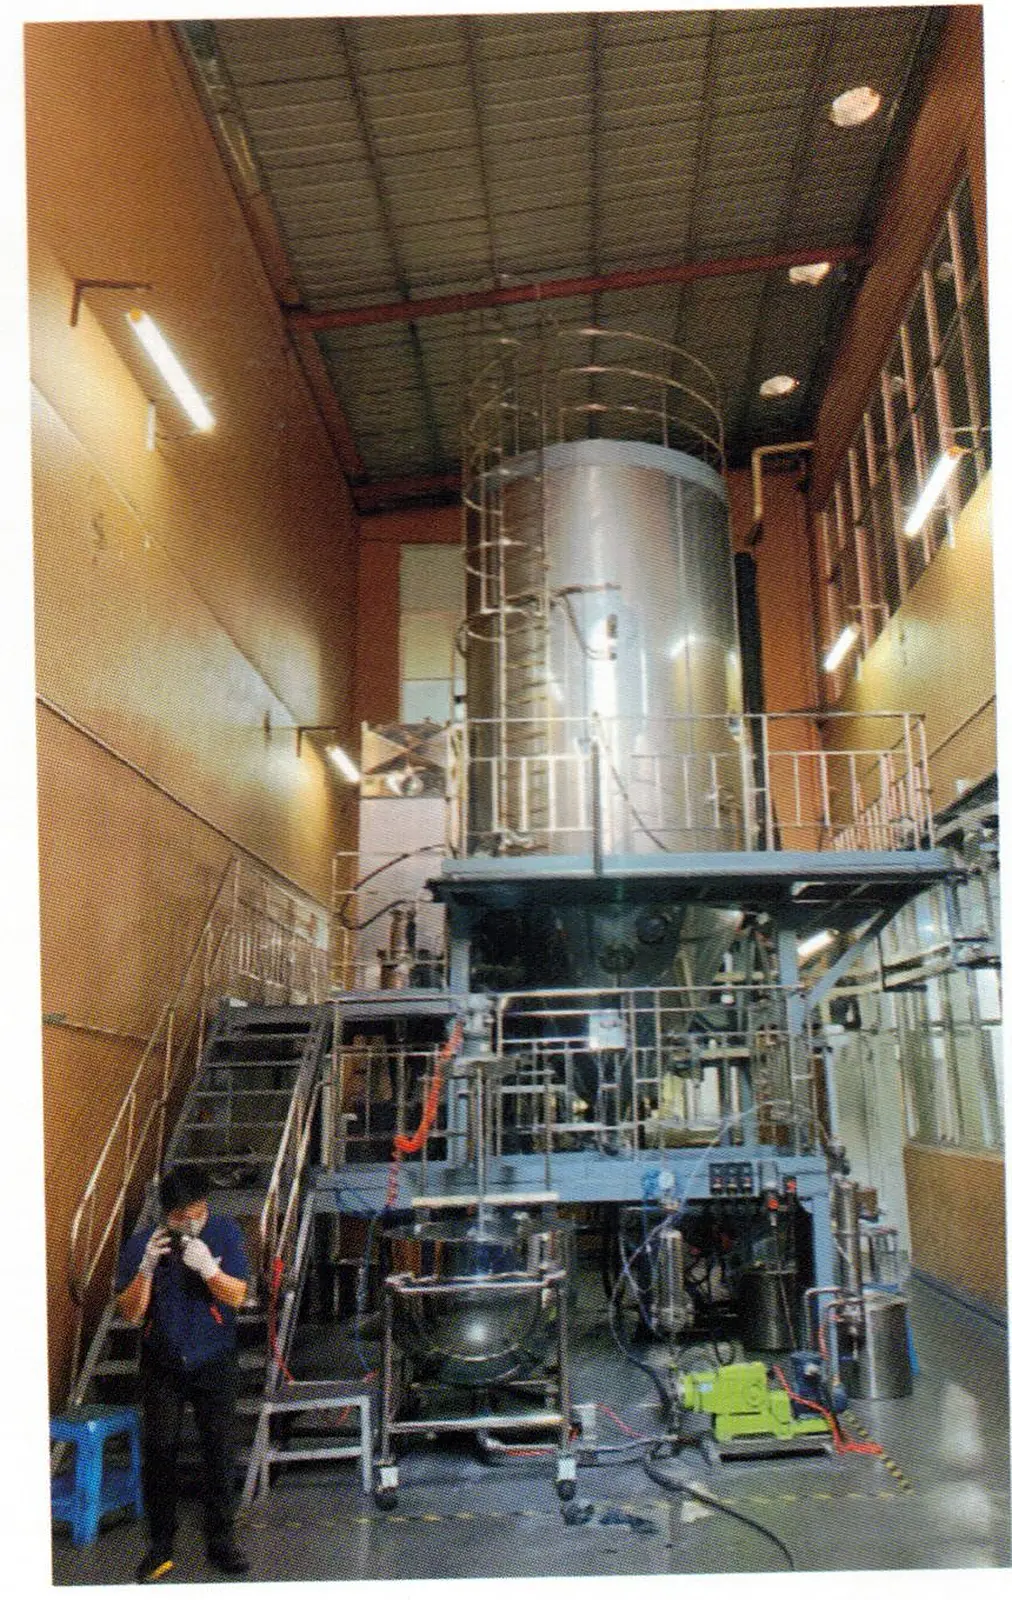
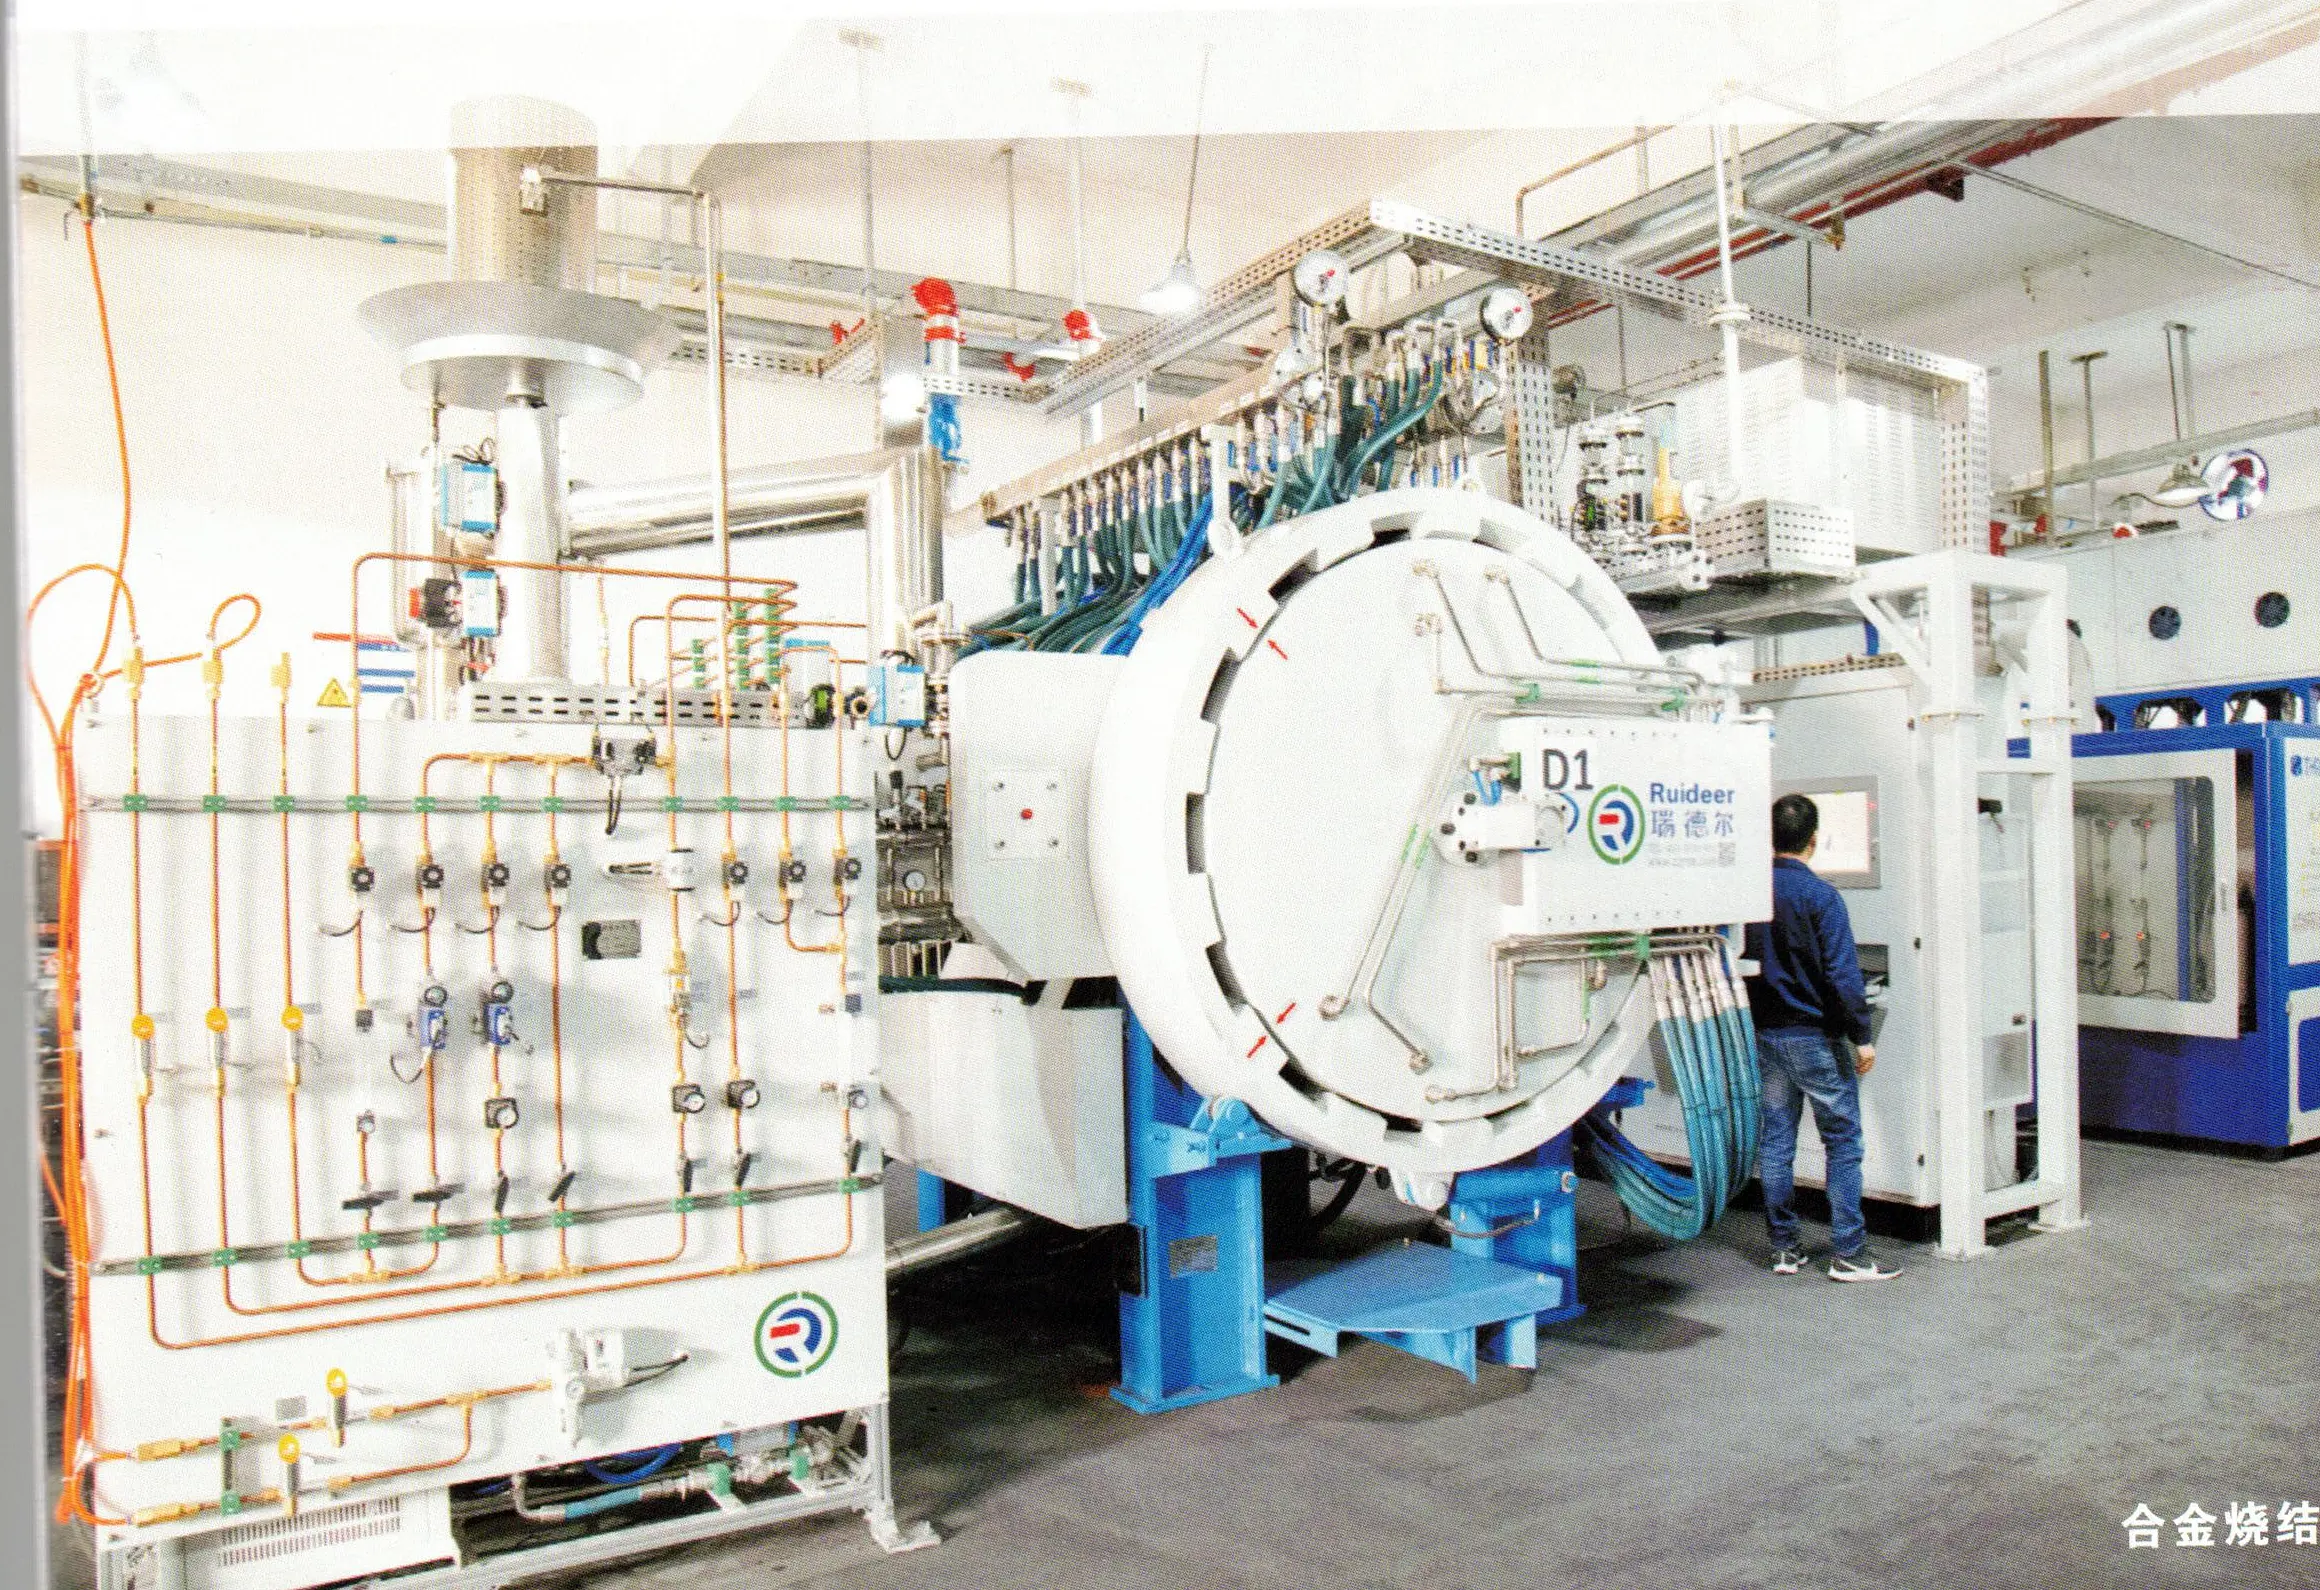
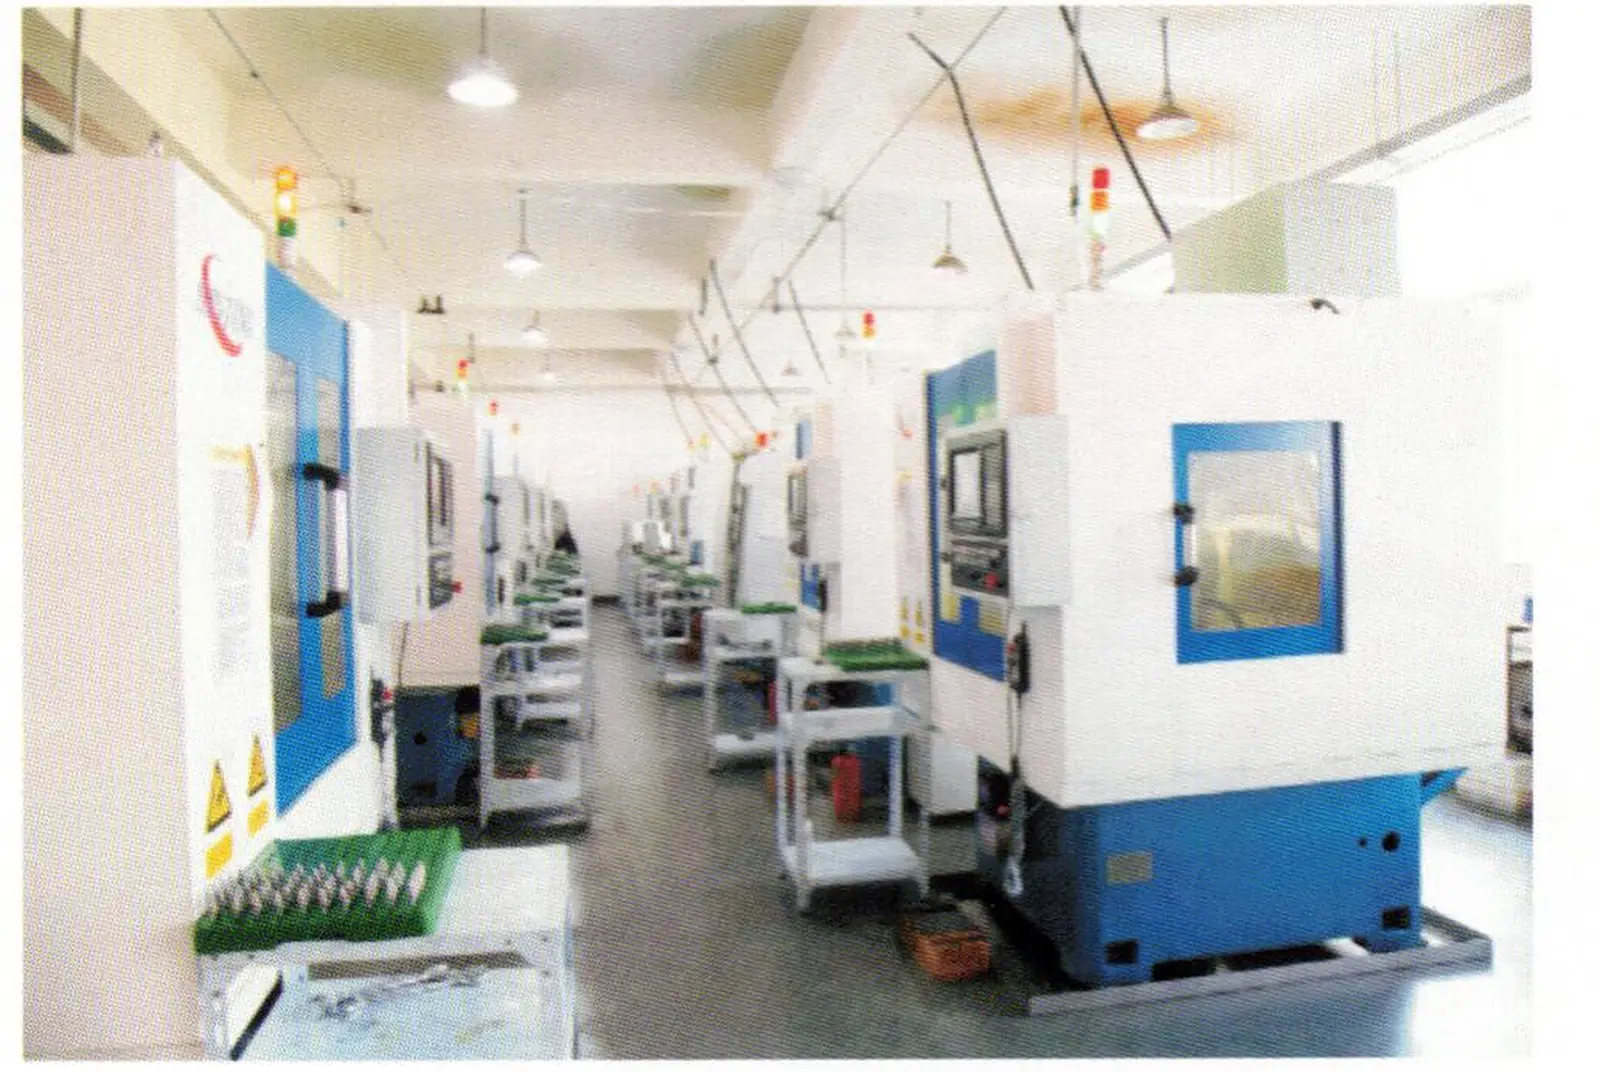
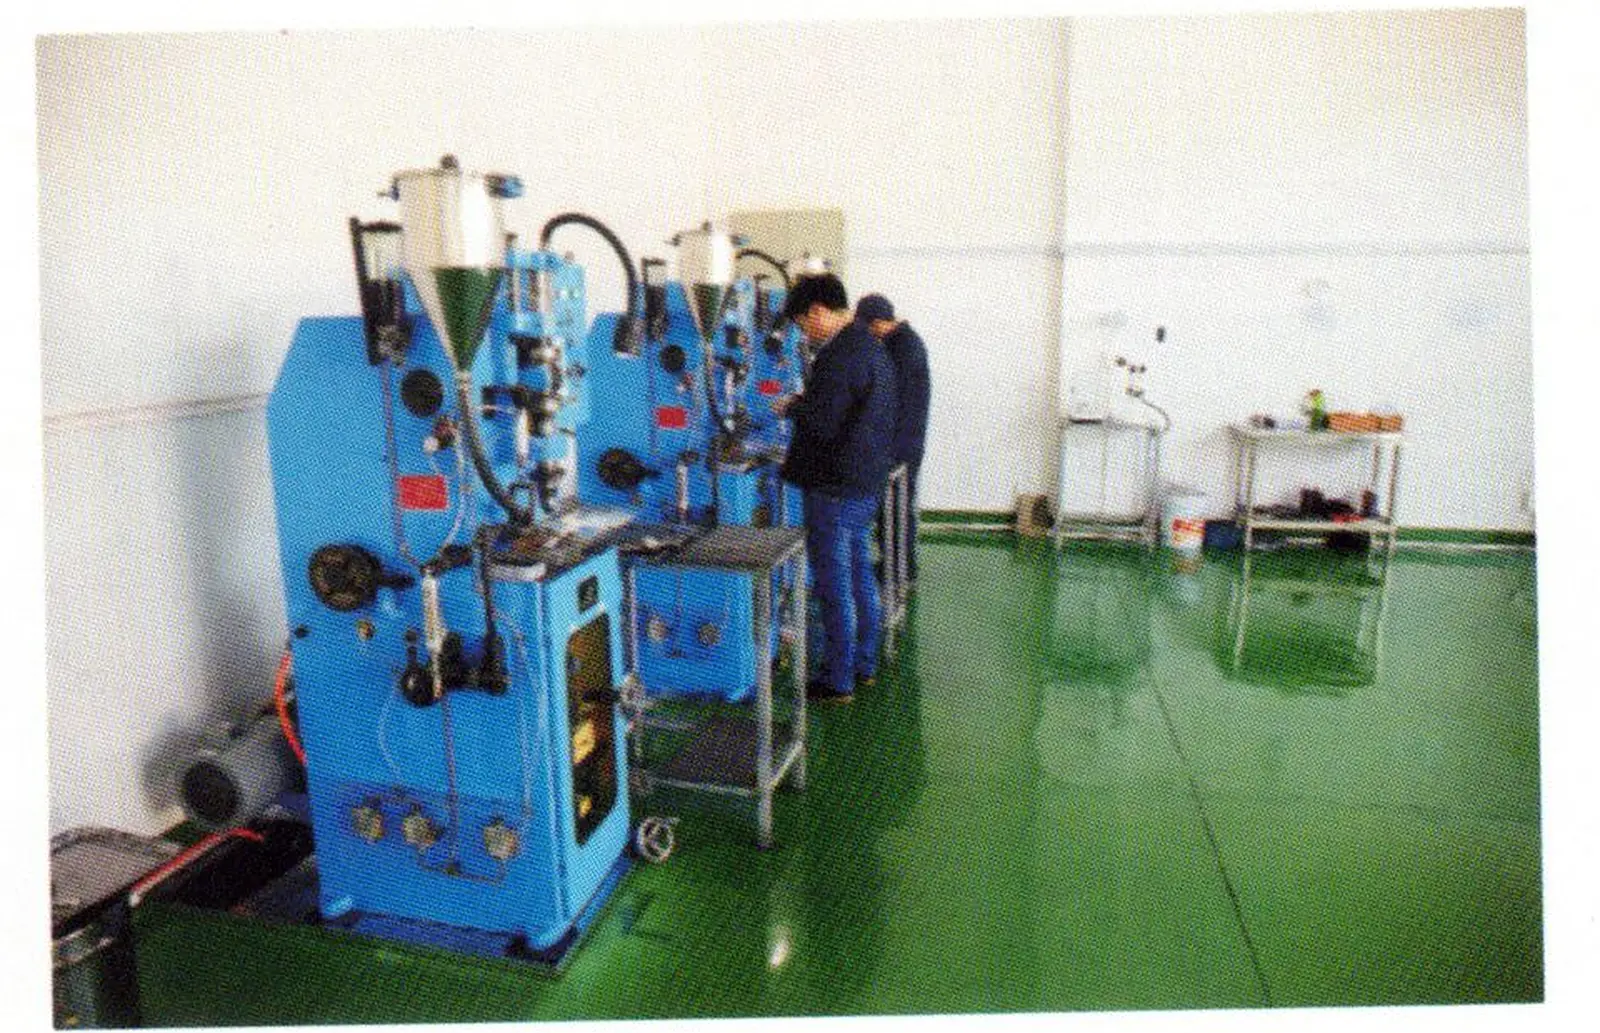
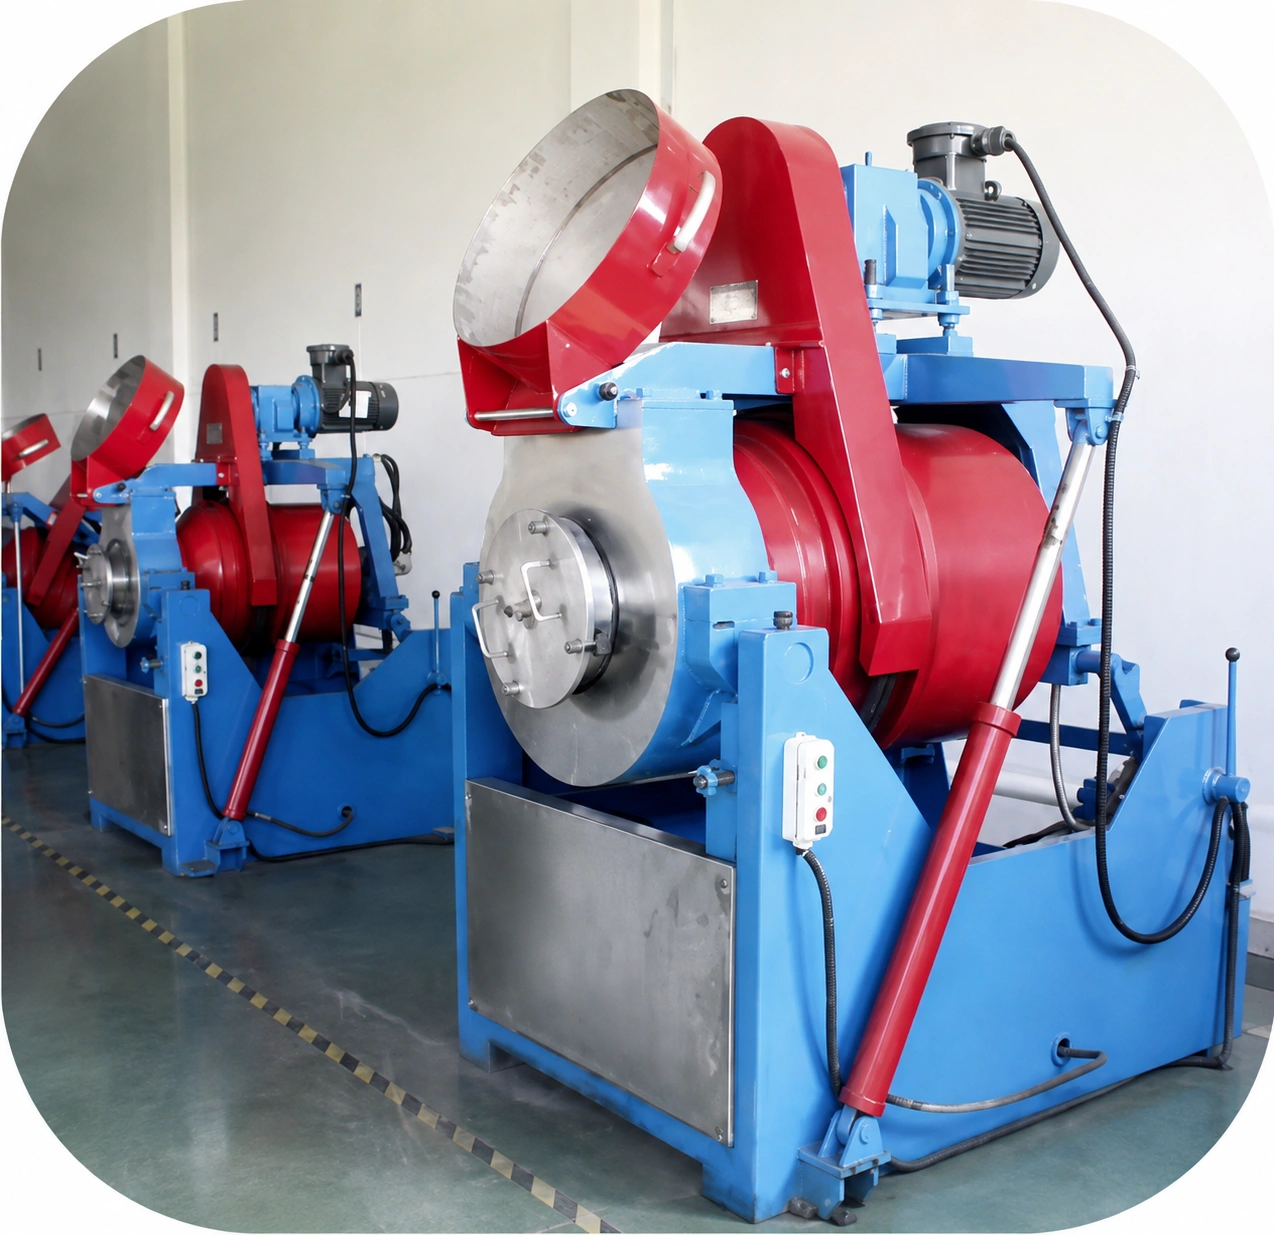
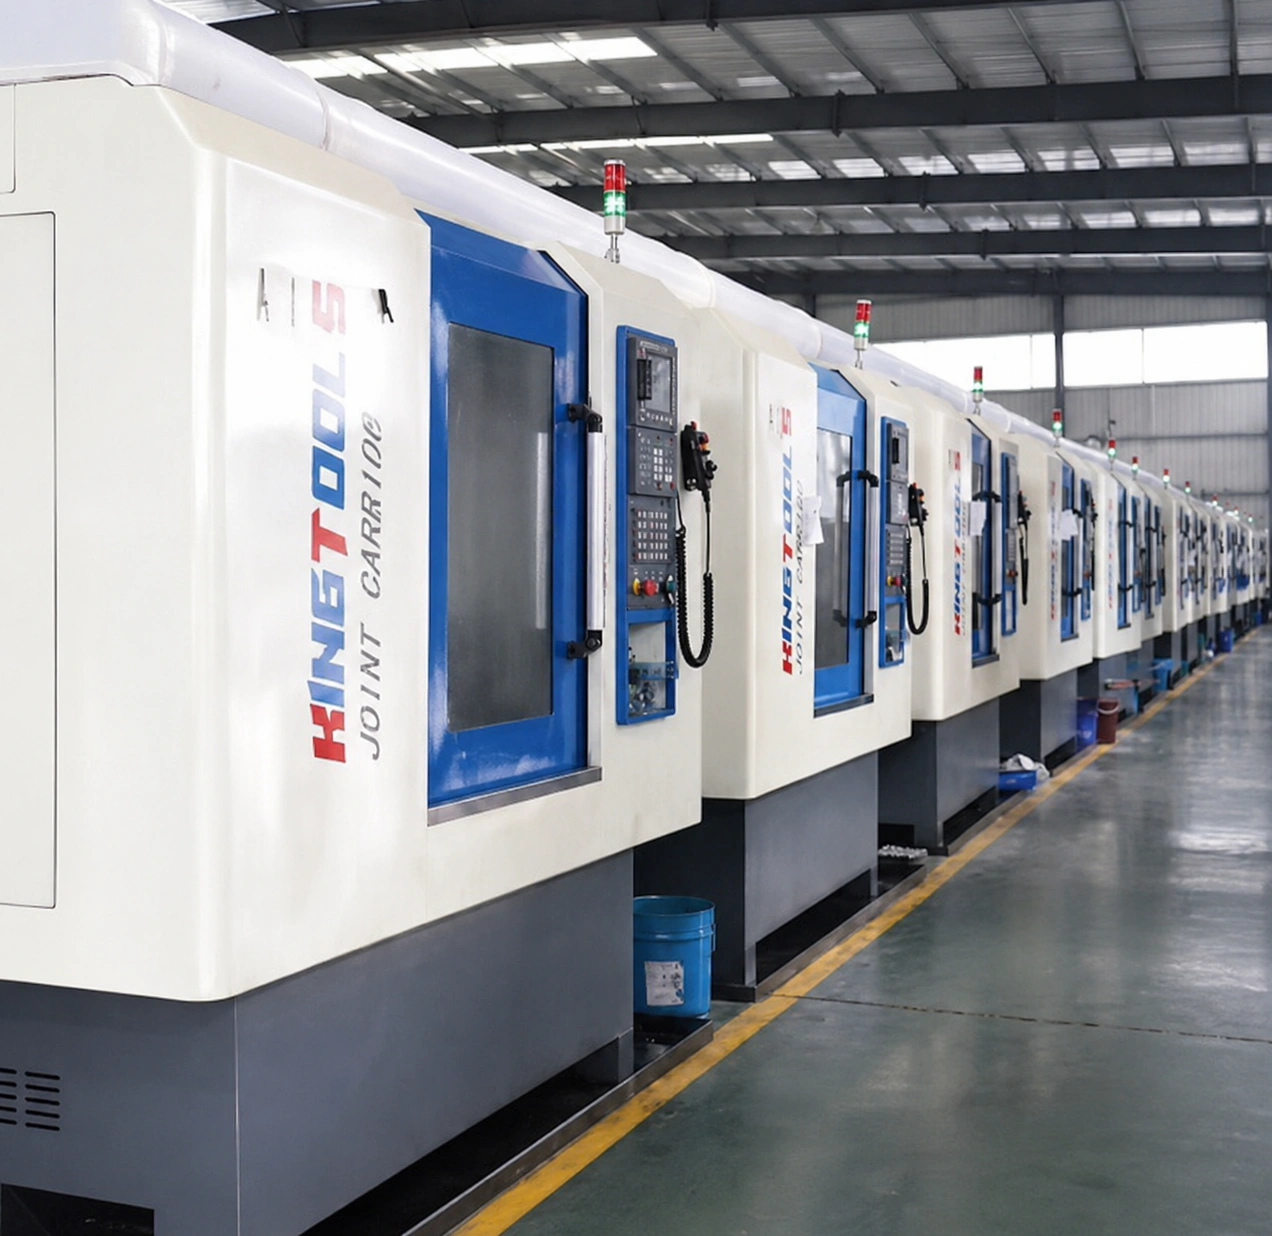
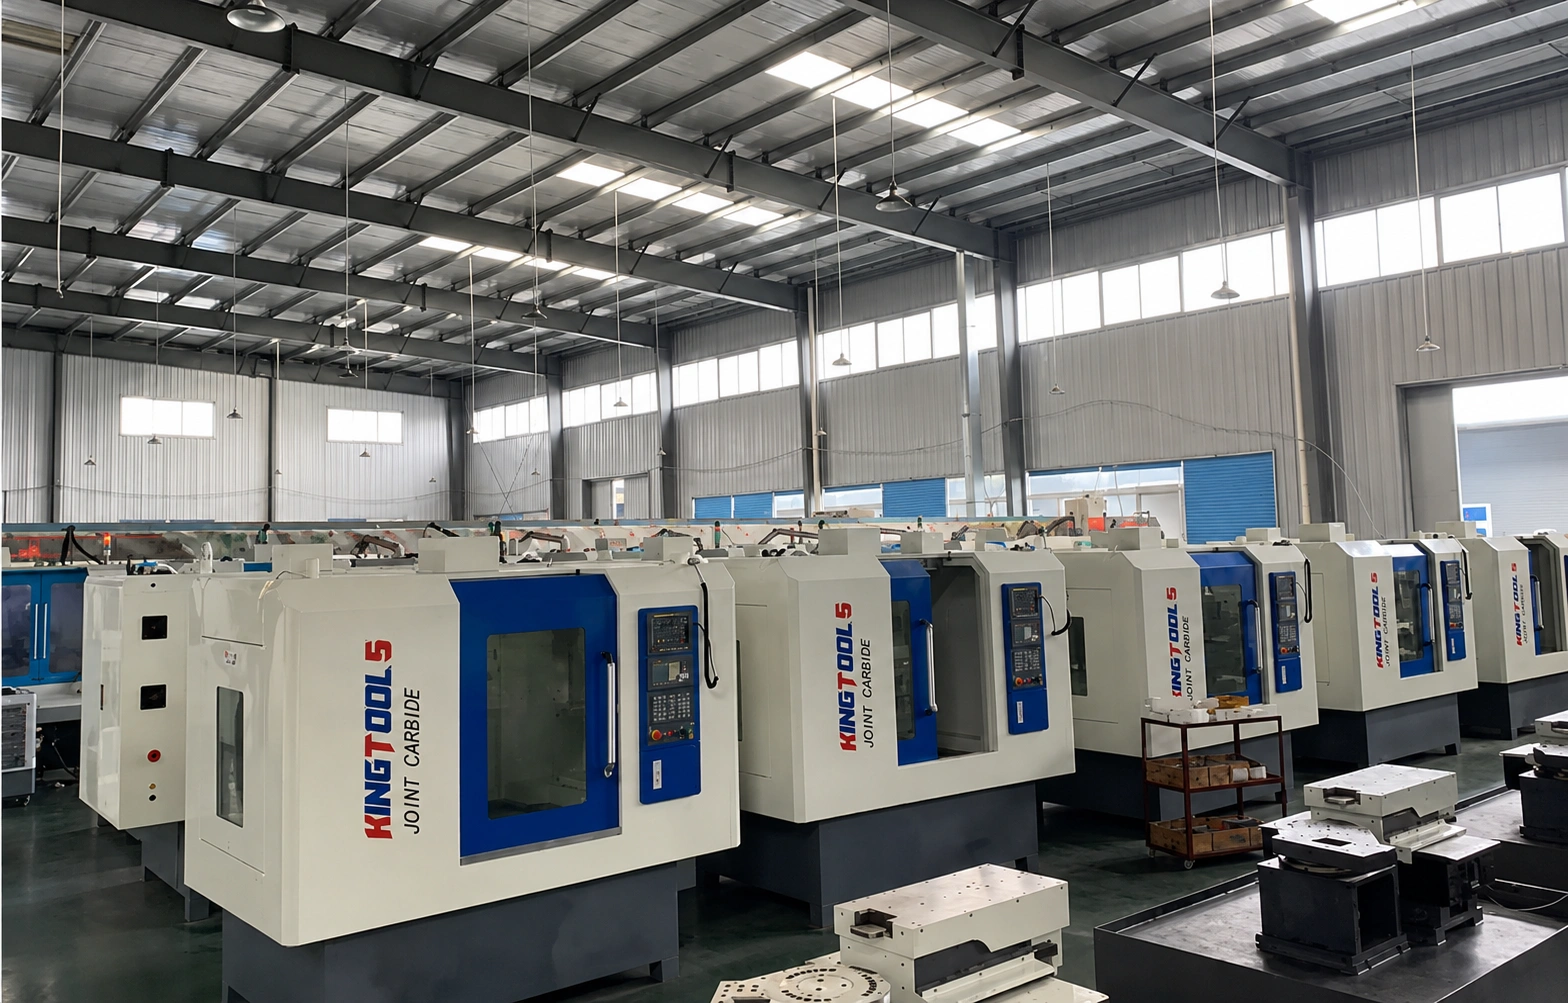
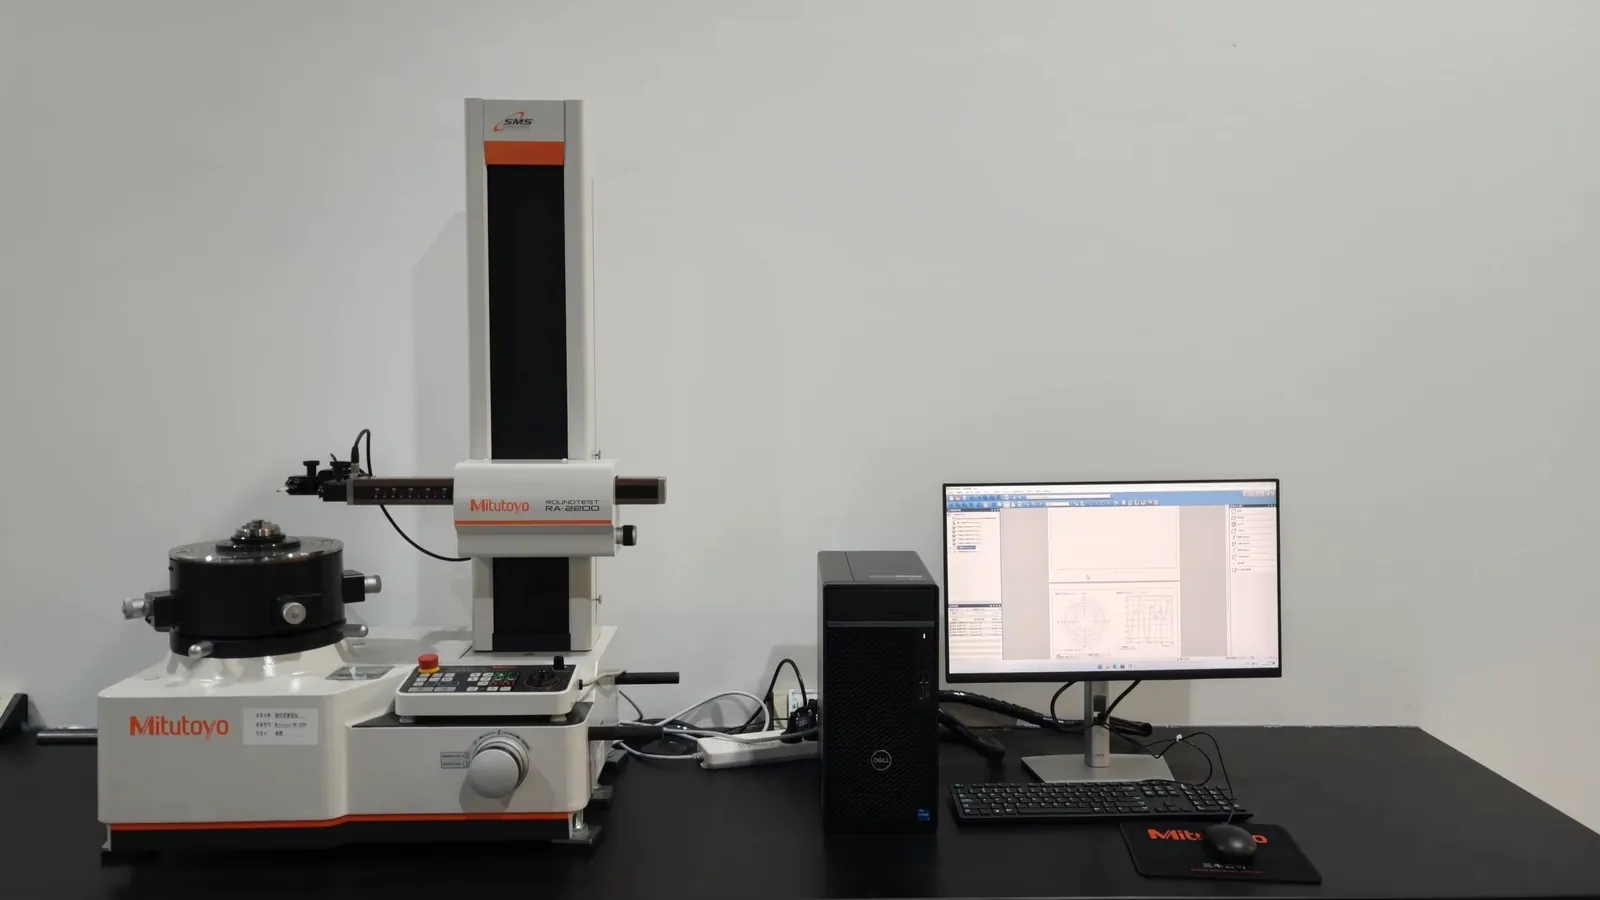
Compare for My Program →The following factory images come from the supplied carbide-burr production library and are shown as capability context, not as unsupported model-specific proof.


Request the production and inspection information relevant to the exact models in your quotation.
Request Factory Information →Long-shank quality is a system, not a photograph. Ask for item-linked evidence covering shank material and dimensions, head geometry, tooth condition, joint process control, straightness, concentricity or runout, visible damage and pack protection. Any acceptance limit should belong to the approved drawing or purchase specification rather than being invented as a universal value for every length and head.


Confirm the inspection method, sampling plan and acceptance criteria for the requested models before production.
Request Quality Information →
Private-label work begins after the technical assortment is frozen. You can specify laser marking where space permits, model and dimension labels, individual sleeves or tubes, set cases, barcodes and export cartons. Keep usable reach, head shape, cut and shank on the same controlled SKU so artwork cannot turn two similar-looking long tools into one ambiguous replacement item.
Confirm the case, insert, item code, barcode, artwork and replacement-model record for the exact assortment in the quotation.

Keep each burr position connected to the approved shape, cut and dimension reference.

Confirm the set layout, replacement model list and label information before production.

Organize the assortment around real buyer applications instead of an arbitrary piece count.

Artwork, barcode, marking and carton requirements remain linked to the approved model matrix.
Authorized customer names, roles and portraits are matched to the relevant product-series review library.
Carbide Cutting Tools · Assortment / Range PlanningA Practical Range for Wholesale Buyers
“For our business as a category manager, the supplier has to support both the product and the commercial process. Our goal was to build a useful assortment rather than stock every possible SKU. Aximet Tools helped us focus on core professional cutting tools selected around real industrial applications and repeat demand and left room to expand later, which is a practical approach for managing inventory. It is the kind of cooperation that helps a buyer build a category instead of constantly changing suppliers.”
Carbide Cutting Tools · Packaging / LogisticsExport Packaging That Supports Distribution
“As an industrial supply buyer, we evaluate suppliers on the full buying experience, not just the quotation. For imported carbide cutting tools, packaging affects total cost and dealer experience. Aximet Tools paid attention to edge protection, clear identification, individual packs, and organized export cartons, making the goods easier for a warehouse and downstream distributor to handle. It is the kind of cooperation that helps a buyer build a category instead of constantly changing suppliers.”
Carbide Cutting Tools · Repeat-Order ReliabilityRepeat Orders Are Easier to Manage
“When I assess a new supplier as an importer & distributor, I look for details that will still matter after the first order. The first order was only the starting point. What mattered was whether tool geometry, grade/finish, dimensions, marking, and packaging would stay organized on repeat purchases. Aximet Tools made the reorder discussion straightforward and reduced unnecessary rechecking. Those details make the overall sourcing decision stronger than choosing on unit price alone.”
Want a range structured around professional customer demand?
Discuss Your Product Range →A quotation should place cutting-head diameter, toothed length, shank size, full tool length and effective projection in separate fields. It should also name the profile, tooth code, end-cut condition, construction and item number. This prevents a nominal length request from becoming an incorrect assumption about working depth or collet support.
Not automatically. Availability depends on head diameter, cut, construction, reach and the supplier's approved operating range. Request a controlled matrix for cylinders, radius cylinders, balls, ovals, trees, flames and tapered profiles. Approve representative samples before adding unlisted combinations to a private-label catalog.
Request item-linked dimensional results, straightness and runout checks, tooth and joint inspection, sample cutting records, marking approval and packaging verification. The record should identify the SKU, drawing revision, inspection method and sample quantity. A generic certificate or one clean sample does not prove consistency across a multi-model production order. RECOMMENDED FAQ QUESTIONS
Choose an extended model only after the standard grinder setup fails the access check. Measure the obstruction, entry width, target depth and direction of cut, then specify the shortest configuration that clears them. This keeps the collection focused on genuine deep-access work instead of selling unnecessary projection as a general upgrade.
A longer unsupported section behaves like a longer cantilever: the same lateral cutting force can create more deflection at the head. Suppliers may therefore assign a different operating window to the extended model. Your product data should connect the approved speed reference to the model code, projection, work material and intended engagement.
Neither system is inherently safer for every job. A purpose-built long tool has one controlled assembly, while a rated extension can provide economical occasional reach. Compare the approved tool size, holder capacity, rotational limit, connection count and alignment procedure. The selected system must be quoted and instructed as a complete configuration.
Commercial assortments can cover straight and radius cylinders, spherical and oval heads, tree and flame profiles, plus selected cones or tapers. The available combinations vary by head dimension, tooth style and reach. Build website filters and packaging from the supplier's released SKU matrix rather than extending every standard profile visually.
Control the complete setup: select only the reach required, inspect shank straightness, clean the correct collet, check spindle condition and use the model's documented speed range. Operators need a stable approach path and limited lateral force. Any new vibration, visible deflection, poor finish or looseness should stop the process and trigger inspection.
Send your workpiece, feature dimensions, usable reach, head shape, cut, shank, grinder and quantity by model. AXIME TOOLS can then prepare a controlled shortlist, sample plan and OEM packaging scope for industrial distribution without inventing an unverified speed or overhang limit. Request the Long-Shank Model Matrix | Discuss OEM Packaging